For industrial applications involving silica fume, efficient material handling is crucial to ensure smooth production processes and maintain operational efficiency. Pneumatic conveying systems have emerged as a preferred solution for transporting silica fume due to their ability to handle fine powders with precision and minimal environmental impact. This article explores the working principle and key characteristics of silica fume material pneumatic conveying systems, providing insights into how such systems operate and the advantages they offer in industrial settings.
Understanding the Working Principle of Silica Fume Pneumatic Conveying
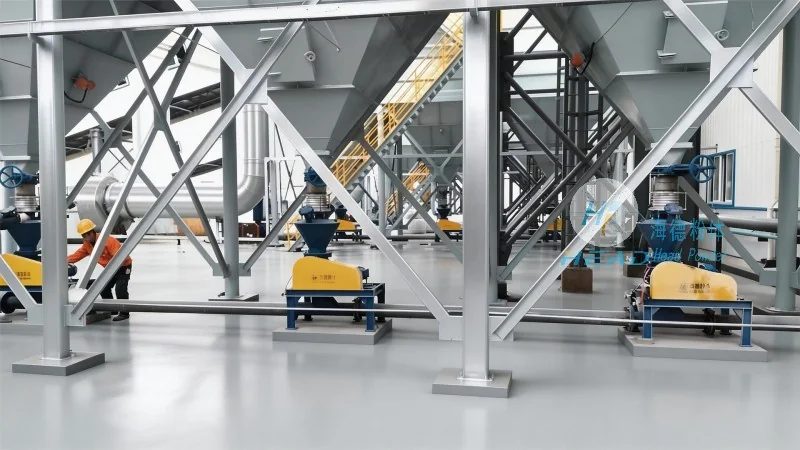
The core of a pneumatic conveying system for silica fume lies in its ability to use compressed air or other gases to transport the material through a network of pipes. The process typically involves several key components, including a material feed hopper, a rotary airlock valve, a conveying line, and a receiver or discharge point. The working principle can be broken down into the following steps:
First, silica fume is fed into the system from a storage silo or hopper. The material is then introduced into the conveying line through a rotary airlock valve, which controls the flow rate and prevents backflow. Compressed air is introduced at the inlet of the conveying line, creating a pressure differential that propels the silica fume particles forward. As the air and material mixture travels through the pipe, the velocity and pressure are maintained to ensure the material remains suspended and moves efficiently to the destination. At the receiving end, the air is separated from the silica fume, often using a cyclone separator or a filter, and the material is collected in a designated container.
Key Characteristics of Silica Fume Pneumatic Conveying Systems
Several distinct characteristics make pneumatic conveying an ideal choice for handling silica fume in industrial applications. These features contribute to the system's effectiveness, reliability, and adaptability in various production environments:
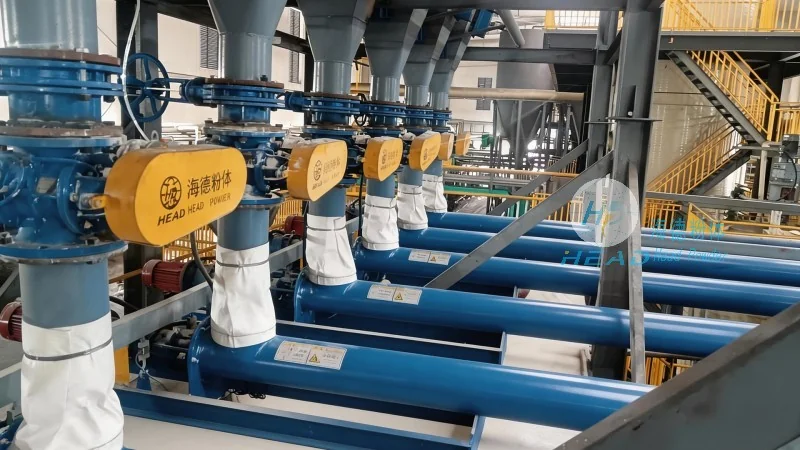
1. Efficiency and Speed: Pneumatic conveying systems can transport silica fume at high speeds, reducing the time required for material movement between processing stages. This efficiency is particularly valuable in high-volume production lines where rapid material turnover is essential.
2. Environmental Friendliness: Unlike traditional mechanical conveying methods, which may generate dust and require additional cleaning, pneumatic systems minimize dust emissions and provide a cleaner working environment. The enclosed pipe system also helps contain the material, reducing the risk of contamination and environmental impact.
3. Flexibility and Scalability: Pneumatic conveying systems can be designed to accommodate various pipe configurations, allowing for complex layouts that can adapt to different plant layouts and production needs. They can be scaled up or down to meet changing production demands, making them a versatile solution for silica fume handling.
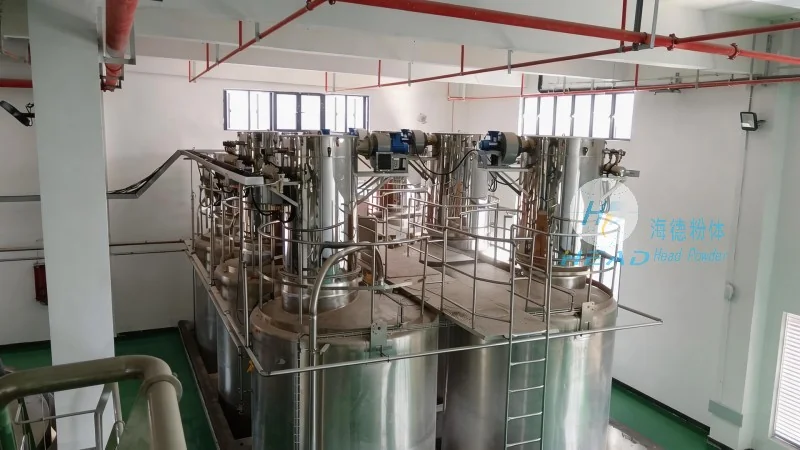
4. Low Maintenance Requirements: Compared to mechanical systems that involve moving parts like belts or buckets, pneumatic conveying systems have fewer moving components, resulting in lower maintenance costs and longer operational lifespans. This reduces downtime and operational expenses for industrial facilities.
5. Safety and Reliability: The enclosed nature of pneumatic systems helps prevent material spillage and exposure to workers, enhancing workplace safety. Additionally, the system's reliability in handling fine powders like silica fume ensures consistent performance and minimal product loss.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
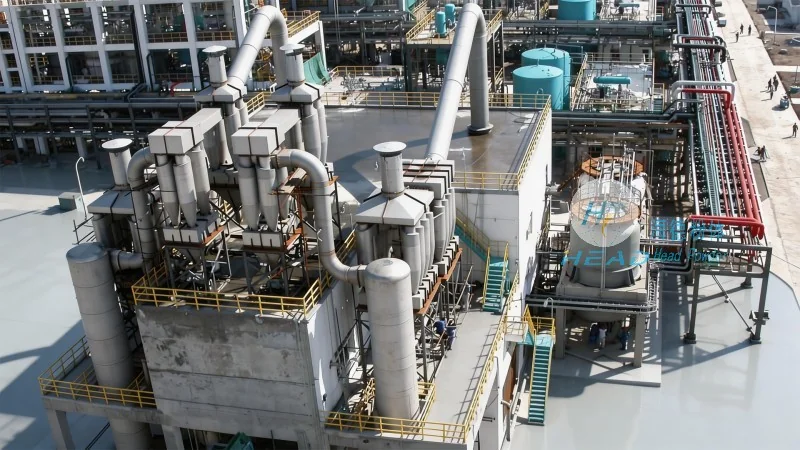
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced material handling systems, including pneumatic conveying solutions for silica fume and other fine powders. With a focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in the industrial sector, providing tailored systems that meet the specific needs of clients across various industries.
HeadPowder's expertise lies in understanding the unique challenges of handling silica fume, such as its fine particle size and potential for dust generation. By leveraging cutting-edge technology and engineering expertise, the company develops pneumatic conveying systems that optimize material transport while ensuring compliance with environmental and safety standards. The company's commitment to quality and reliability has earned it a reputation for delivering durable and efficient solutions that enhance operational efficiency and reduce costs for its clients.
Located in Shandong, China, headpowder serves a global market, providing customized pneumatic conveying systems that cater to diverse industrial applications. The company's team of experienced engineers and technicians work closely with clients to assess their material handling requirements, design suitable systems, and ensure seamless integration into existing production processes. This customer-focused approach has enabled headpowder to build long-term relationships with clients and deliver solutions that meet their evolving needs.




