Working Principle and Characteristics of Pneumatic Conveying for Limestone Powder Materials
Release time:2026-09-18 06:01:25
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Understanding the pneumatic conveying of limestone powder materials is crucial for industries that rely on efficient material handling solutions. This article delves into the working principles and key characteristics of such systems, providing insights into how they operate and the advantages they offer.
Introduction to Pneumatic Conveying Systems
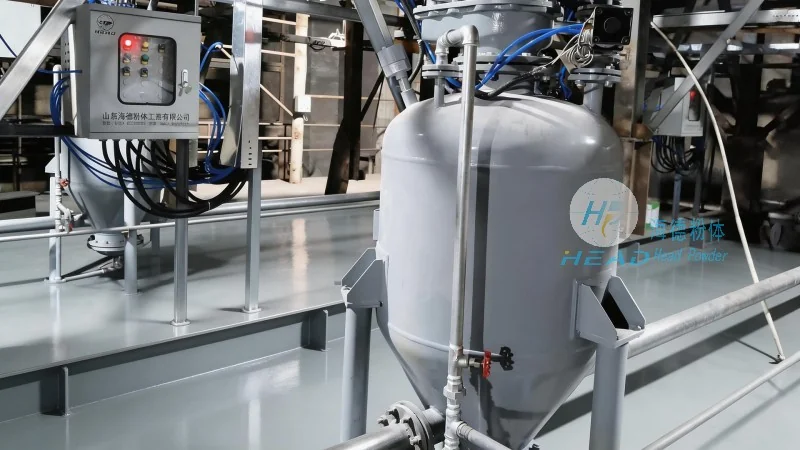
Pneumatic conveying systems are used to transport bulk materials like limestone powder through a pipeline using air or gas as the conveying medium. These systems are widely adopted in various industrial applications due to their ability to handle fine powders and minimize material degradation. The process involves creating a pressure differential or using vacuum to move the material from the source to the destination.
Working Principle of Limestone Powder Pneumatic Conveying
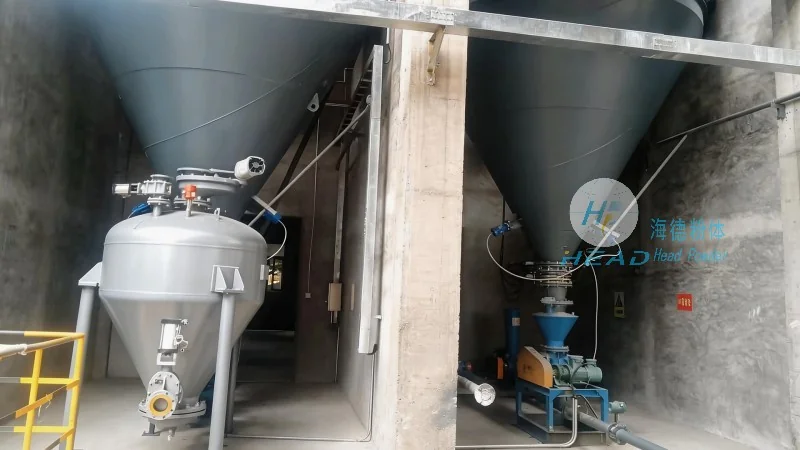
The core of a pneumatic conveying system for limestone powder lies in the interaction between the material and the air flow. The system typically consists of a hopper, a conveyor line, and a receiver. The limestone powder is fed into the hopper, where it is then drawn into the conveyor line by a fan or blower. The air flow carries the powder particles through the pipeline, and the system is designed to maintain a consistent flow rate to ensure reliable transport. The working principle can be categorized into two main types: pressure and vacuum systems.
Key Characteristics of Limestone Powder Pneumatic Conveying
Several characteristics define the performance and suitability of pneumatic conveying systems for limestone powder. Firstly, the system's efficiency in handling fine powders is a significant advantage, as it prevents dust accumulation and reduces the risk of material blockage. Secondly, the ability to transport materials over long distances without the need for intermediate storage or transfer points enhances operational flexibility. Additionally, the system's compact design allows for easy integration into existing industrial setups, minimizing space requirements. Another notable characteristic is the low maintenance cost associated with pneumatic conveying, as it has fewer moving parts compared to mechanical conveying systems. This makes it a cost-effective solution for long-term material handling needs.
Applications and Benefits in Industrial Settings
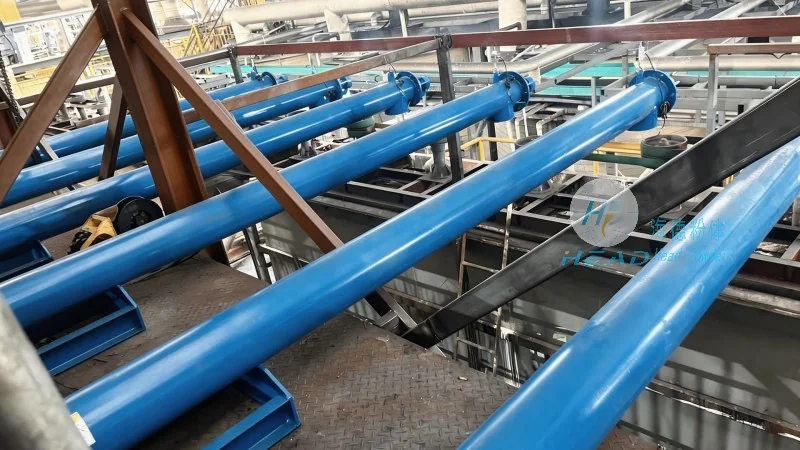
Pneumatic conveying systems for limestone powder find applications in various industries, including cement production, mining, and chemical processing. The benefits of using such systems include improved safety by reducing manual handling of powders, enhanced product quality through minimized contamination, and increased operational efficiency through automated material transport. The systems also contribute to environmental sustainability by reducing dust emissions and improving workplace safety.




