For industrial applications requiring efficient and safe material handling, the inert gas circulation material pneumatic conveying equipment has emerged as a critical solution. This technology is designed to transport bulk materials using a closed-loop system that incorporates inert gases, ensuring minimal contamination and optimal performance. The following sections will delve into the working principles and key features of this equipment, providing a comprehensive understanding for potential users and industry professionals.
Overview of Inert Gas Circulation Material Pneumatic Conveying Equipment
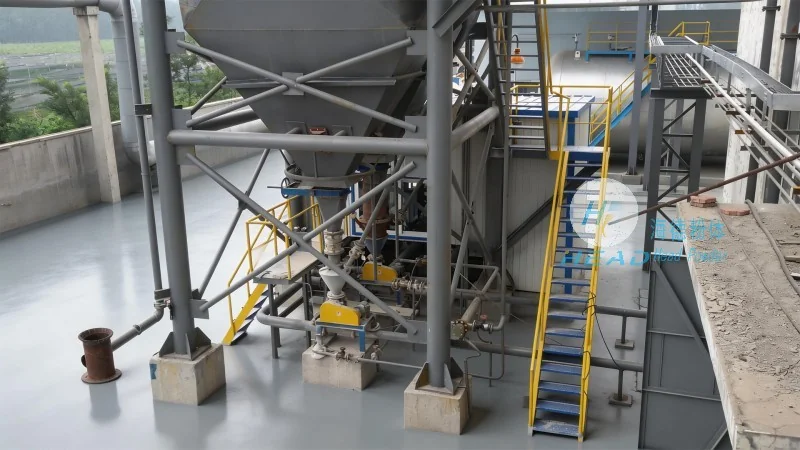
The inert gas circulation material pneumatic conveying equipment is a specialized system engineered to handle bulk materials in a controlled environment. Unlike traditional pneumatic conveying systems that may use air or other gases, this equipment utilizes inert gases—such as nitrogen or carbon dioxide—to create a safe and inert atmosphere. This approach is particularly valuable in industries where material purity is paramount, such as pharmaceuticals, food processing, and chemical manufacturing. The system typically consists of several key components, including a material feed hopper, a gas circulation loop, a conveying line, and a discharge unit. Each component works in tandem to ensure seamless material transport while maintaining the integrity of the conveyed product.
Working Principles of the Equipment
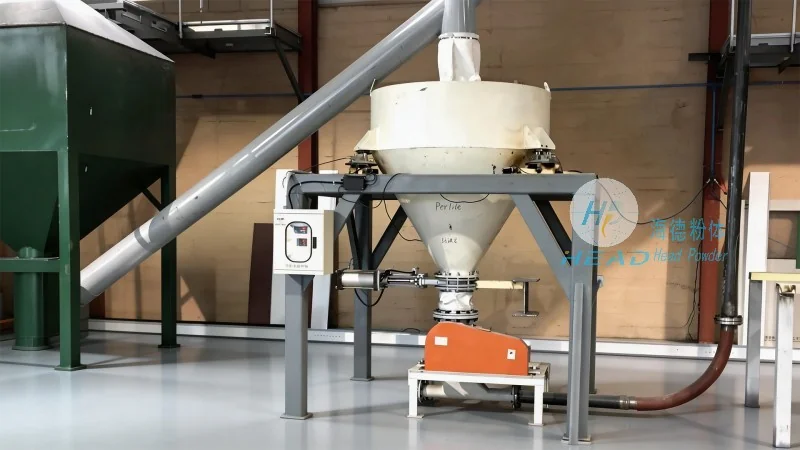
The operation of inert gas circulation material pneumatic conveying equipment is based on the principle of fluidization and gas-solid flow. The process begins with the material being fed into the hopper, where it is then introduced into the conveying line. Simultaneously, an inert gas is introduced into the system, creating a low-pressure or high-pressure environment depending on the specific design. The gas circulates through the system, carrying the material particles along the conveying line. The key to this process is the balance between gas velocity and particle size, which determines the conveying efficiency and the risk of material degradation. The equipment often incorporates control mechanisms to regulate gas flow, pressure, and material feed rate, ensuring consistent performance and preventing system overload. Additionally, the closed-loop design minimizes gas loss and maintains a stable operating environment, which is crucial for maintaining product quality and safety.
Key Features and Advantages
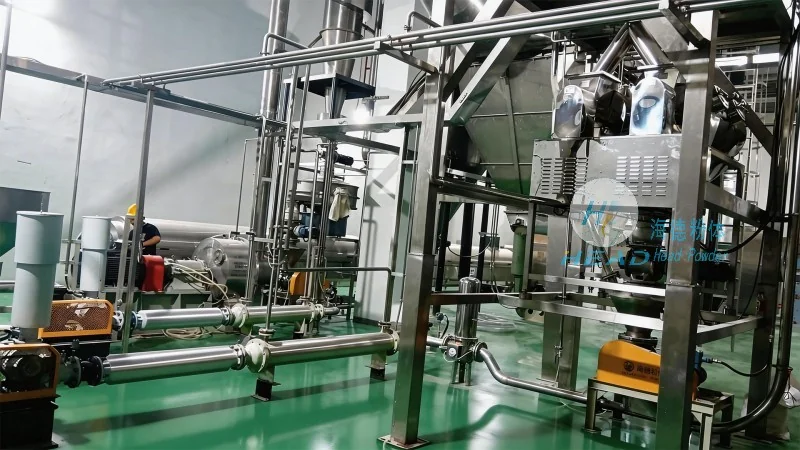
Several distinct features set the inert gas circulation material pneumatic conveying equipment apart from conventional systems. First, the use of inert gases provides a contamination-free environment, which is essential for industries where product purity is non-negotiable. This feature eliminates the risk of oxidation, moisture absorption, or chemical reactions that could compromise the material's quality. Second, the closed-loop system enhances energy efficiency by recycling the conveying gas, reducing operational costs and environmental impact. Third, the equipment offers high conveying capacity and flexibility, allowing it to handle a wide range of material types and particle sizes. It can transport materials over long distances with minimal pressure drop, making it suitable for large-scale industrial applications. Furthermore, the system is designed for easy maintenance and cleaning, with components that can be easily disassembled and sanitized, which is particularly important in industries like food and pharmaceuticals where hygiene is a top priority. The advanced control systems integrated into the equipment also enable precise monitoring and adjustment of operational parameters, ensuring optimal performance and reliability.
Applications and Industries
The inert gas circulation material pneumatic conveying equipment finds applications across various industries where bulk material handling is required. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements. The inert gas environment prevents contamination, ensuring that the final product meets regulatory standards. In the food processing sector, the equipment is employed to handle powders and granules, such as flour, sugar, and spices, maintaining product freshness and preventing spoilage. The chemical industry also benefits from this technology, as it can safely convey reactive or hazardous materials without the risk of ignition or chemical reactions. Additionally, the equipment is used in the mining and minerals sector to transport ores and concentrates, where the inert gas helps prevent oxidation and maintain material quality. The versatility of the system makes it suitable for a wide range of industrial processes, from manufacturing to logistics.
Conclusion and Company Information
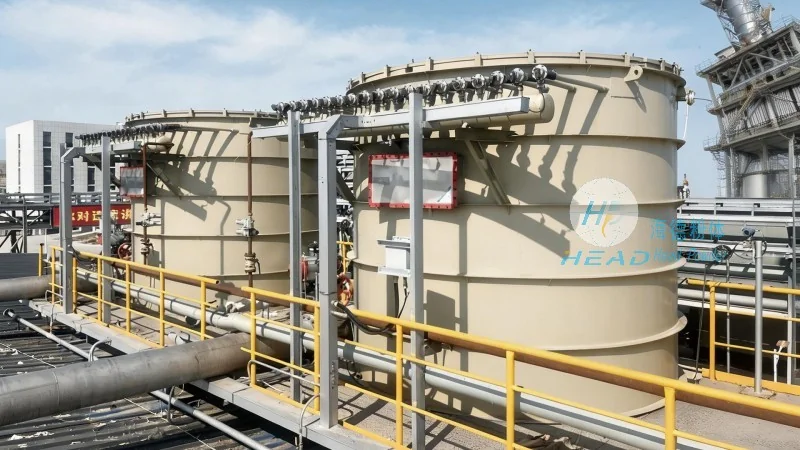
In summary, the inert gas circulation material pneumatic conveying equipment is a sophisticated solution for efficient and safe bulk material handling. Its working principles, which rely on inert gas circulation and controlled fluidization, ensure high conveying efficiency and product integrity. The key features, including contamination-free operation, energy efficiency, and flexibility, make it an ideal choice for industries with stringent quality and safety requirements. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing these advanced systems, leveraging years of experience to deliver customized solutions that meet the unique needs of each client. With a commitment to quality and innovation, HeadPowder continues to set industry standards for material handling technology. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art facility dedicated to research, development, and production of pneumatic conveying equipment. For businesses seeking reliable and efficient material handling solutions, the inert gas circulation material pneumatic conveying equipment from HeadPowder represents a superior choice.




