Phosphate calcium is a critical raw material in various industrial applications, and efficient handling of this material is essential for maintaining production efficiency and safety. Pneumatic conveying equipment, specifically designed for phosphate calcium, offers a reliable solution for transporting this material from one location to another. This article explores the working principle and key features of such equipment, highlighting how it enhances material handling processes in industrial settings.
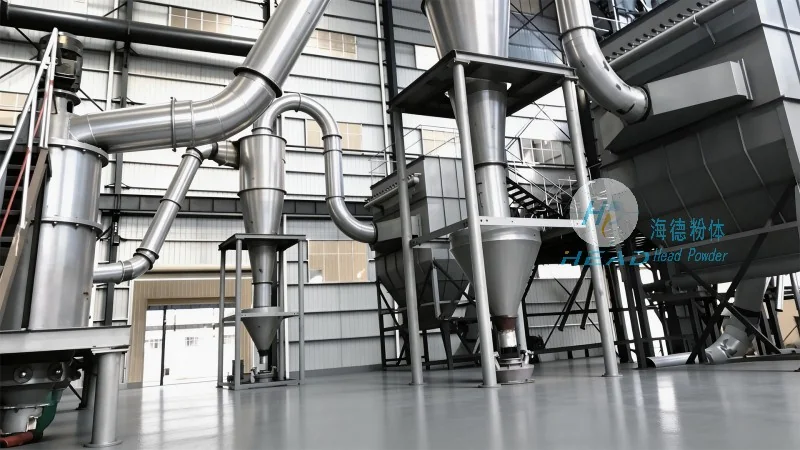
Understanding the Working Principle of Phosphate Calcium Pneumatic Conveying Equipment
The core of phosphate calcium pneumatic conveying equipment lies in its ability to transport bulk materials using a pressurized or vacuum system. The system typically operates by creating a flow of air or gas through a pipeline, which carries the phosphate calcium particles along with it. There are two main types of pneumatic conveying systems: pressure and vacuum. In pressure systems, a positive pressure is generated at the material source, pushing the material through the pipeline. Vacuum systems, on the other hand, create a negative pressure at the receiving end, drawing the material from the source. The choice between these systems depends on factors such as the distance to be covered, the material's properties, and the required flow rate.
For phosphate calcium, which is often a fine or powdery material, the equipment must be designed to handle the specific characteristics of this substance. This includes considerations for particle size, moisture content, and potential dust generation. The conveying process involves several key components: a material feeder, a conveying line, a separation or collection system, and a control unit. The material feeder ensures a consistent flow of phosphate calcium into the system, while the conveying line transports the material to the desired location. The separation system, such as a cyclone or filter, separates the material from the air stream, allowing the air to be recycled or vented. The control unit monitors and adjusts the system parameters to maintain optimal performance.
Key Features of Phosphate Calcium Pneumatic Conveying Equipment
When selecting pneumatic conveying equipment for phosphate calcium, several features are crucial for ensuring efficiency and reliability. One of the most important features is the ability to handle fine or powdery materials without clogging or blockages. This is achieved through the use of specialized components, such as flexible hoses or smooth pipeline interiors, which minimize the risk of material buildup. Another critical feature is the system's ability to maintain a consistent flow rate, even with varying material loads. This is essential for maintaining production continuity and preventing downtime.
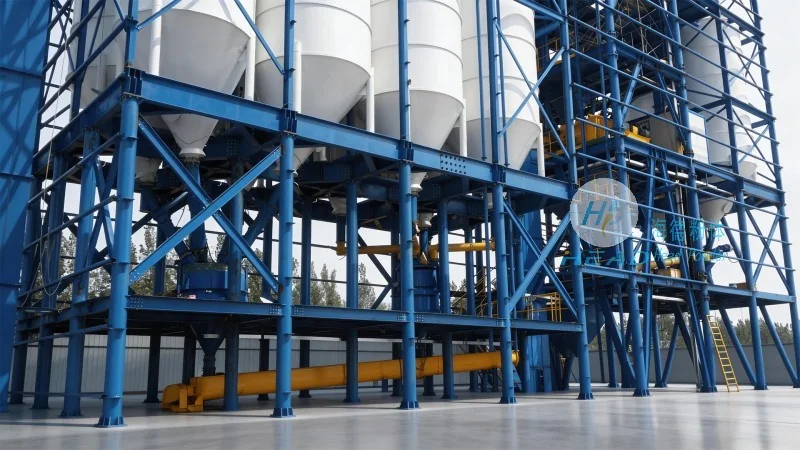
Energy efficiency is another key consideration for phosphate calcium pneumatic conveying equipment. Modern systems are designed to minimize energy consumption while maximizing conveying capacity. This includes features such as variable speed drives, which adjust the air flow based on the material load, and efficient air compressors or vacuum pumps. Additionally, the equipment should be equipped with advanced monitoring and control systems that allow for real-time adjustments to optimize performance and reduce energy waste.
Another important feature is the system's ability to handle different particle sizes and moisture levels. Phosphate calcium can vary in its physical properties, and the equipment must be able to accommodate these variations without compromising performance. This may involve adjustable feed rates, variable air velocities, or specialized separation technologies that can handle a wide range of material characteristics.
How Shandong HeadPowder Engineering Co., Ltd. Enhances Phosphate Calcium Handling
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of industrial material handling equipment, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of phosphate calcium applications. With years of experience in the industry, the company has developed a deep understanding of the unique challenges associated with handling this material, and their equipment is designed to address these challenges effectively.
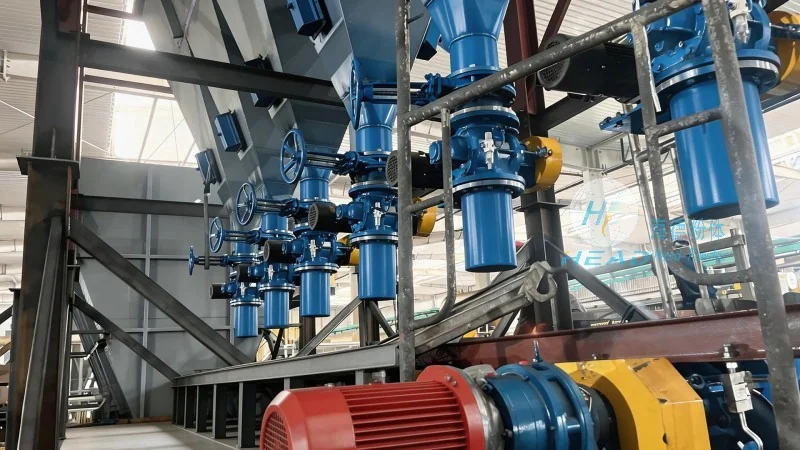
The company's phosphate calcium pneumatic conveying equipment is engineered to provide reliable and efficient material transport, ensuring that production processes run smoothly and safely. By incorporating advanced technologies and materials, the equipment is built to withstand the rigors of continuous operation, reducing maintenance requirements and increasing overall system reliability.
HeadPowder's commitment to quality and customer satisfaction is reflected in their comprehensive product range and dedicated support services. The company offers customized solutions to meet the specific requirements of each client, ensuring that the equipment is optimized for their particular application. This includes options for different conveying capacities, distances, and material characteristics, allowing for flexibility and adaptability in various industrial settings.
Conclusion: The Advantages of Phosphate Calcium Pneumatic Conveying Equipment
In conclusion, phosphate calcium pneumatic conveying equipment offers a highly effective solution for handling this critical material in industrial applications. By understanding the working principle and key features of such equipment, businesses can make informed decisions about their material handling systems, leading to improved efficiency, reduced costs, and enhanced safety. With the expertise and experience of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can access reliable and efficient equipment that meets their specific needs, ensuring long-term success in their operations.




