For industrial applications involving sulfur powder, efficient and reliable material handling is crucial. Pneumatic conveying systems offer a solution that addresses the unique challenges of transporting fine powders like sulfur. This article explores the working principle and key features of such equipment, highlighting how it meets the demands of modern industrial processes.
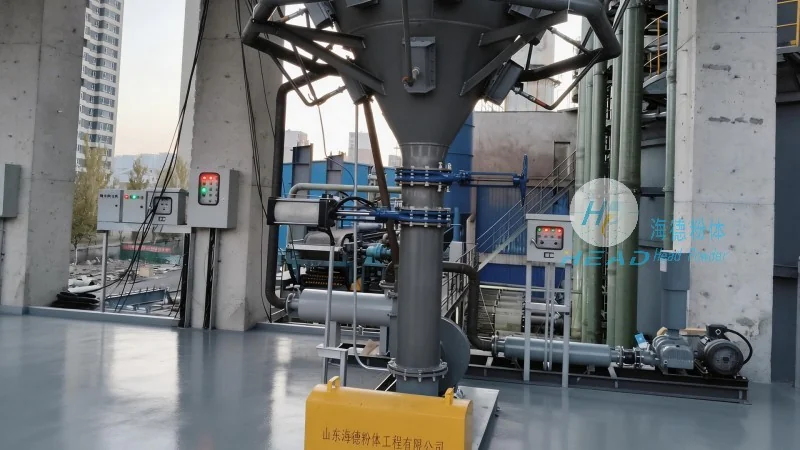
Working Principle of Pneumatic Conveying Systems
The core of a pneumatic conveying system for sulfur powder lies in its ability to transport material using air or gas as the conveying medium. The process typically involves a few key components: a hopper for material storage, a blower or compressor to generate the airflow, a pipeline system to guide the material, and a receiver or discharge point. When the system is activated, the blower creates a pressure differential, drawing sulfur powder from the hopper into the pipeline. The air flow carries the powder particles through the system, ensuring consistent and controlled transport. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational efficiency.
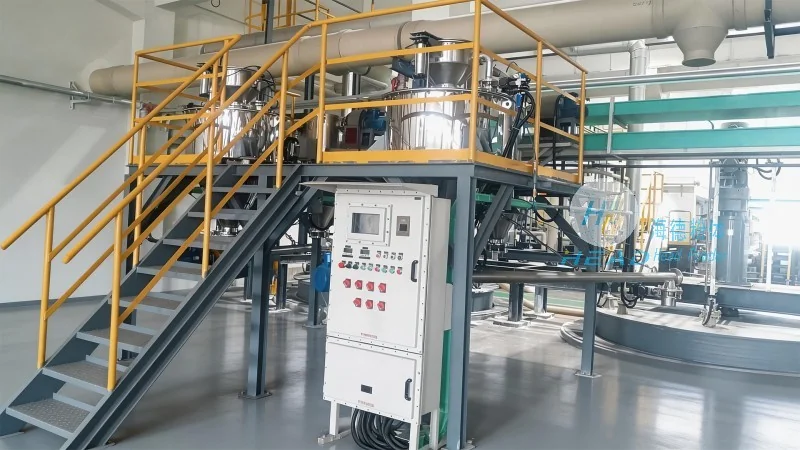
Key Features of Sulfur Powder Pneumatic Conveying Equipment
Several distinct features make pneumatic conveying equipment ideal for sulfur powder applications. Firstly, it provides a dust-free and enclosed transport environment, which is critical for maintaining product quality and safety in industrial settings. The system minimizes exposure to air, preventing oxidation or contamination of the sulfur powder. Secondly, it offers high flexibility in terms of layout and integration with existing production lines. The pipeline can be configured in various configurations, such as vertical, horizontal, or a combination, to suit the specific space and operational requirements of the facility. Thirdly, the equipment is designed for low maintenance, with components like the blower and pipeline being robust and durable. This reduces downtime and operational costs, making it a cost-effective solution for long-term use. Additionally, the system can handle varying flow rates and material loads, adapting to the dynamic needs of industrial processes.
Application Benefits and Performance
Implementing pneumatic conveying equipment for sulfur powder offers several performance benefits. The enclosed system ensures that the material remains contained, reducing the risk of spills or environmental contamination. This is particularly important for sulfur, which can be hazardous if not handled properly. The system also enhances process control, allowing for precise dosing and consistent material flow. This leads to improved product quality and reduced waste. Furthermore, the energy efficiency of pneumatic conveying systems contributes to lower operational costs over time. By minimizing the need for manual handling and reducing the risk of material degradation, the equipment provides a sustainable solution for industrial material transport.
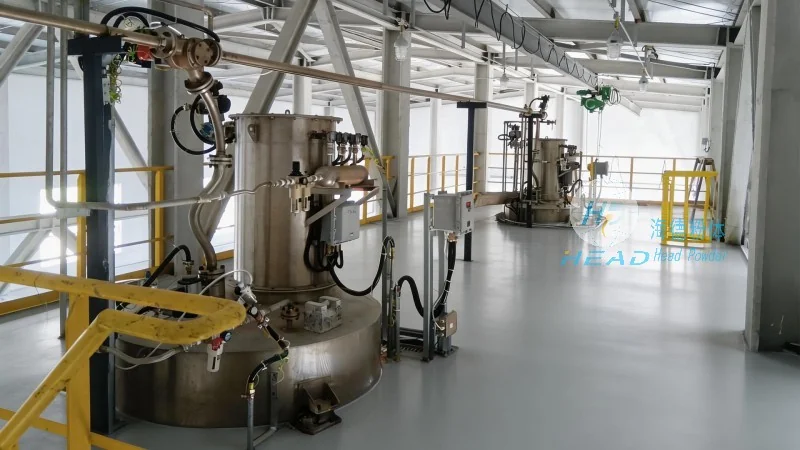
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and supply of advanced material handling equipment. With a focus on industrial applications involving fine powders, the company leverages decades of experience to develop solutions tailored to the unique needs of clients. HeadPowder's commitment to quality and innovation ensures that their pneumatic conveying systems meet the highest standards of performance and reliability. The company's headquarters is located in Shandong, China, where they maintain state-of-the-art facilities for research, development, and production. Their team of experts works closely with clients to understand their specific requirements and provide customized solutions that enhance operational efficiency and safety.




