Centralized bulk material pneumatic conveying is a key technology in material handling, offering efficient and flexible solutions for transporting powders and granules. This article explores the underlying principles of this system and highlights its distinctive working scenario characteristics, providing insights into how it enhances operational efficiency across various industries.
Understanding the Core Principles of Centralized Bulk Material Pneumatic Conveying
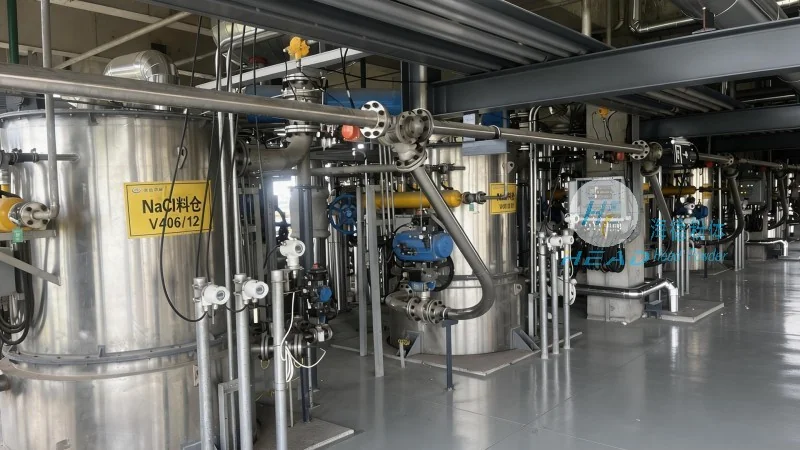
The fundamental principle of centralized bulk material pneumatic conveying involves using air as the medium to transport bulk materials. This system typically operates under either positive pressure (pressure pneumatic conveying) or negative pressure (vacuum pneumatic conveying). In positive pressure systems, air is forced through the conveying line, carrying the material from the source to the destination. Conversely, negative pressure systems draw air and material through the line using a vacuum, creating a suction effect. The choice between these two modes depends on factors such as material properties, distance, and the need for containment. Centralized systems, in particular, integrate multiple feeding points into a single, unified network, allowing for coordinated material flow management from a central control point.
Key Working Scenario Characteristics of Centralized Bulk Material Pneumatic Conveying
One of the most notable characteristics of centralized bulk material pneumatic conveying is its ability to handle multiple material sources simultaneously. This is achieved through a network of pipelines connected to various feed hoppers or silos, all controlled by a central system. The advantages of this approach include improved material tracking, reduced downtime, and enhanced safety, as operators can monitor and adjust the flow from a single interface. Additionally, centralized systems often incorporate advanced automation features, such as real-time monitoring of pressure, flow rates, and material levels, ensuring optimal performance and minimizing the risk of blockages or system failures.
Application Scenarios and Industry Use Cases
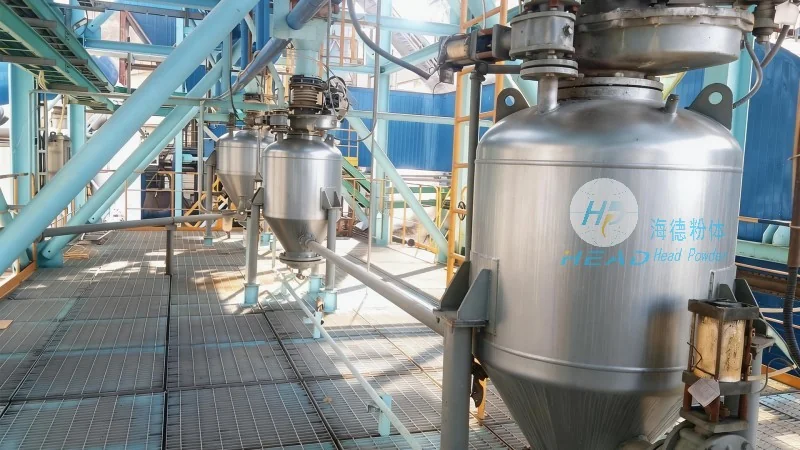
Centralized bulk material pneumatic conveying is widely applied across diverse industries, including chemical manufacturing, food processing, pharmaceuticals, and mining. In chemical plants, for instance, it enables the safe and efficient transport of hazardous powders, reducing exposure risks for personnel. In the food industry, the system ensures hygienic handling of ingredients, maintaining product quality and compliance with regulatory standards. Pharmaceutical applications benefit from the system's ability to handle sensitive materials, such as active pharmaceutical ingredients (APIs), with minimal contamination and precise dosing. Even in mining operations, centralized pneumatic conveying can transport raw materials from storage to processing facilities, optimizing logistics and reducing the need for manual handling.
Advantages and Benefits in Practical Operations
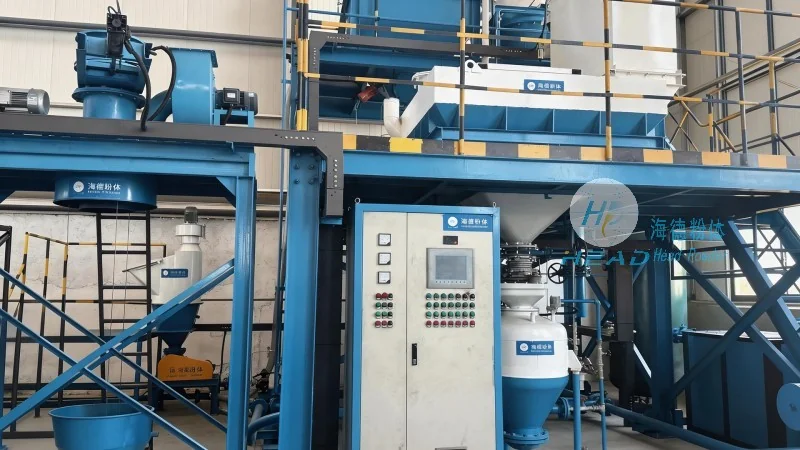
Implementing centralized bulk material pneumatic conveying offers several tangible benefits. First, it significantly reduces labor costs by automating material movement, eliminating the need for manual loading and unloading. Second, the system minimizes material loss and contamination, as the enclosed pipelines prevent dust and moisture from entering the material stream. Third, it enhances energy efficiency compared to traditional methods like belt conveyors, as the air flow can be optimized to match the material's specific conveying requirements. Furthermore, centralized systems provide better scalability, allowing businesses to expand their operations by adding more feed points or extending the conveying network without major overhauls.
Conclusion and Company Overview
Centralized bulk material pneumatic conveying represents a sophisticated solution for modern material handling challenges. By integrating advanced technology with centralized control, this system optimizes efficiency, safety, and cost-effectiveness in various industrial applications. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of each client. With operations based in Shandong, China, the company leverages years of expertise to deliver reliable and efficient solutions that meet the highest industry standards. Whether for new installations or system upgrades, HeadPowder's commitment to quality and innovation ensures that clients achieve superior performance and long-term operational success.




