HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading provider of industrial solutions specializing in pneumatic conveying technology. Based in Shandong, China, the company has established itself as a trusted partner for businesses seeking efficient and reliable material handling solutions. This article explores the fundamental principles of automatic bulk material pneumatic conveying systems and highlights the key working scene characteristics that make them indispensable in modern industrial applications.
The Fundamental Principle of Pneumatic Conveying Systems
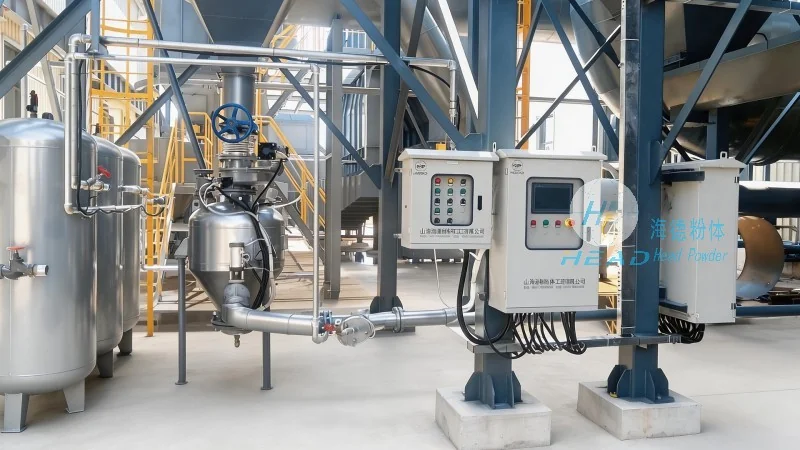
Pneumatic conveying systems operate on the principle of transporting bulk materials through a pipeline using air or other gases. Unlike traditional mechanical conveyors, these systems utilize the force of compressed air to move powders, granules, and other particulate materials from one location to another. The core components typically include a hopper for material storage, a blower or compressor to generate the necessary air pressure, a pipeline network to guide the material flow, and a discharge point where the material is released. The system works by creating a pressure differential: the blower draws air into the system, and as it passes through the material, it lifts and propels the particles along the pipeline. This process is highly efficient for handling fine or abrasive materials that might be difficult to transport with mechanical means.
Key Working Scene Characteristics of Pneumatic Conveying Systems
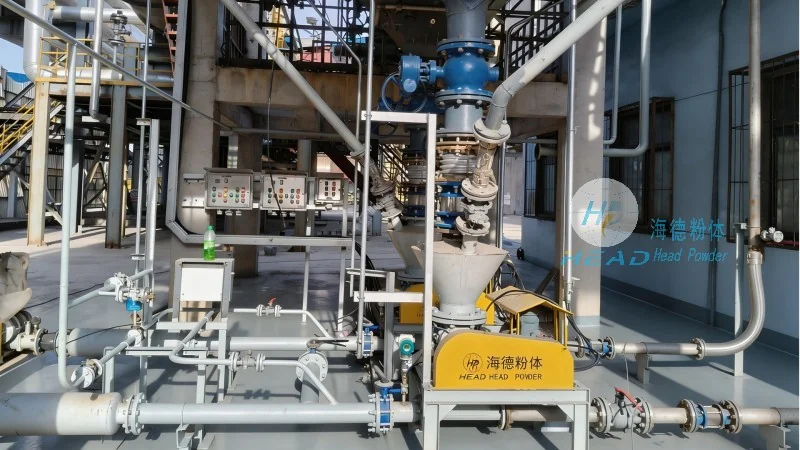
The working scene characteristics of pneumatic conveying systems are tailored to meet diverse industrial needs, offering flexibility and adaptability across various applications. One of the primary advantages is the ability to handle a wide range of materials, from fine powders to coarse granules, without the need for additional equipment like buckets or belts. This makes them ideal for industries such as pharmaceuticals, food processing, chemicals, and mining, where material purity and contamination control are critical. Another notable characteristic is the system's compact design, which allows for installation in confined spaces, reducing the footprint required for material handling operations. The flexibility in pipeline layout also enables the integration of multiple feeding and discharge points, facilitating complex material flow paths within a facility. Additionally, pneumatic conveying systems are known for their low maintenance requirements compared to mechanical conveyors, as they have fewer moving parts and are less susceptible to wear and tear from abrasive materials. This contributes to lower operational costs and increased system longevity.
Application Scenarios and Operational Efficiency
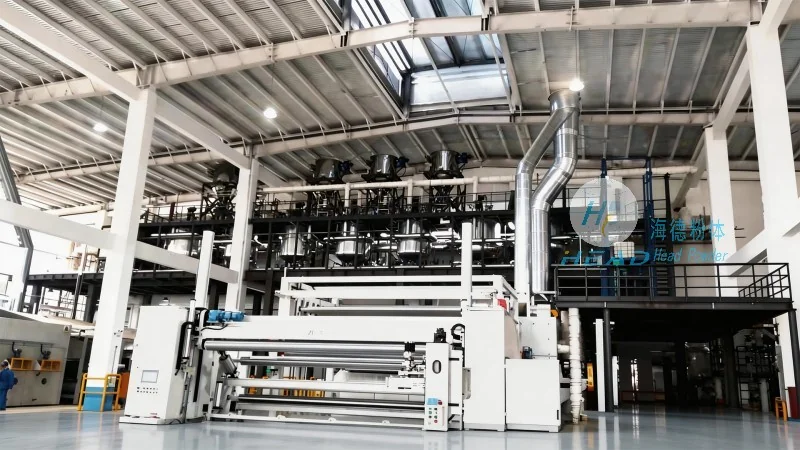
The working scene characteristics of pneumatic conveying systems are evident in their practical applications across various industries. In the pharmaceutical industry, for example, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with strict purity standards. The enclosed pipeline design prevents contamination and ensures that materials remain sterile, meeting regulatory requirements. Similarly, in food processing, pneumatic conveyors are employed to handle powders like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. The ability to control air pressure and flow rates allows for precise dosing and mixing, which is crucial for product consistency. In the chemical industry, these systems are utilized for transporting abrasive or corrosive materials, such as cement, limestone, or acids, where mechanical conveyors might cause wear or damage. The system's ability to handle these challenging materials without degradation ensures reliable performance and reduces downtime. Furthermore, the compact and flexible design of pneumatic conveying systems makes them suitable for retrofitting into existing facilities, enabling businesses to upgrade their material handling capabilities without major structural changes. This adaptability is particularly valuable in industries where space is limited or where existing infrastructure needs to be optimized.
Conclusion: HeadPowder's Commitment to Industrial Excellence
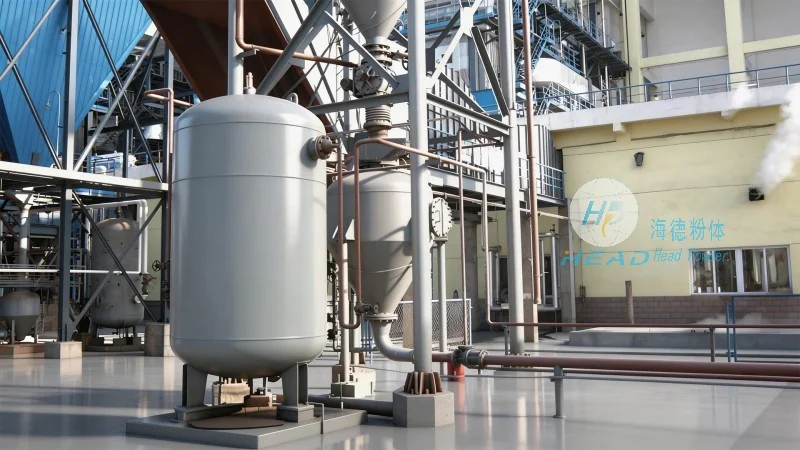
HeadPowder Engineering Co., Ltd., based in Shandong, China, exemplifies the innovation and reliability of pneumatic conveying technology. By leveraging the fundamental principles of automatic bulk material transport, the company's systems offer enhanced efficiency, flexibility, and cost-effectiveness for a wide range of industrial applications. The working scene characteristics, including material versatility, compact design, and low maintenance, make these systems a preferred choice for businesses seeking to optimize their material handling processes. As industries continue to evolve and demand higher standards of efficiency and safety, HeadPowder remains at the forefront of providing tailored solutions that meet the unique needs of each client. With a focus on quality and customer satisfaction, the company ensures that its pneumatic conveying systems not only meet but exceed industry expectations, contributing to the success and growth of its partners.




