Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in dust removal and powder conveying solutions. The company focuses on providing advanced equipment for industrial applications, including pulse dust removal systems and powder conveying devices. This article explores the operational principles of pulse dust removal powder conveying equipment and highlights its key features in various working environments.
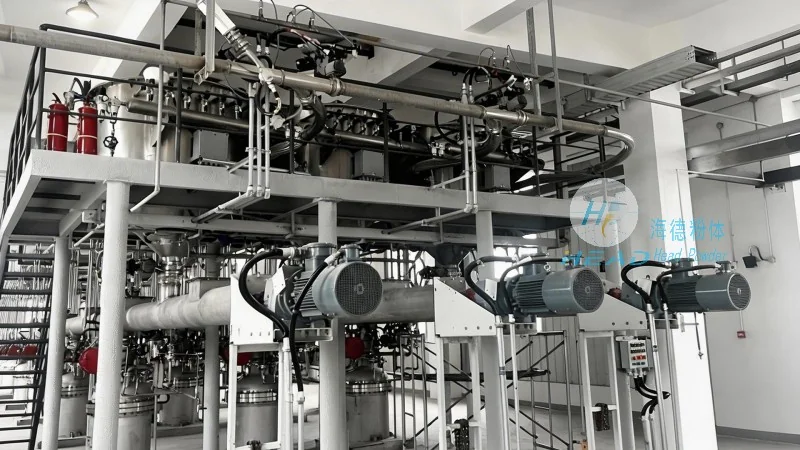
Overview of Pulse Dust Removal Powder Conveying Equipment
Pulse dust removal powder conveying equipment is a sophisticated system designed to handle fine powders while simultaneously removing airborne dust. It integrates dust collection and material transport functions, making it essential in industries such as chemical manufacturing, metallurgy, and building materials. The equipment operates by combining filtration and pneumatic conveying technologies, ensuring both high efficiency in dust removal and reliable material transport. The system typically includes a dust collector, a conveying pipeline, and a control unit, all working together to achieve optimal performance.
Working Principle of the Equipment
The core of pulse dust removal powder conveying equipment is the pulse jet cleaning mechanism. The dust collector, equipped with filter bags or cartridges, captures particles as they pass through the filtration media. Over time, dust accumulates on the filter surface, increasing pressure drop and reducing airflow. To maintain efficiency, the system uses a pulse jet valve to release compressed air into the filter bags. This rapid burst dislodges accumulated dust, which falls into the hopper for collection. Simultaneously, a blower creates negative pressure in the pipeline, drawing fine powder from the source and transporting it to the destination. The integration of dust removal and material transport makes the system highly efficient and versatile.
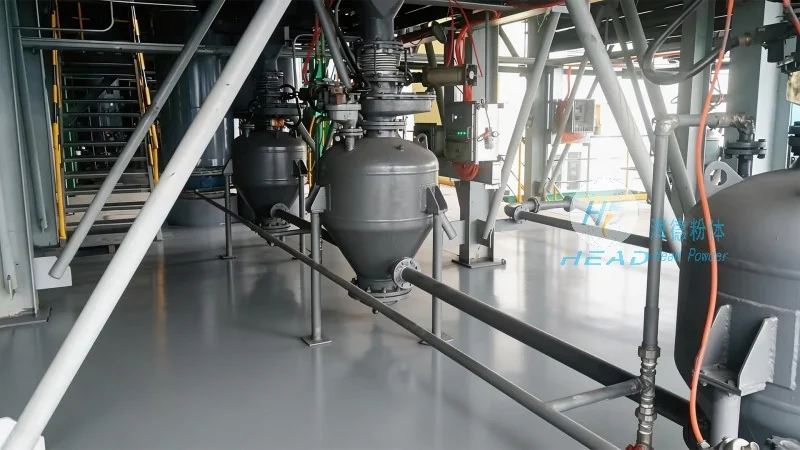
Key Characteristics in Working Scenes
The performance of pulse dust removal powder conveying equipment is influenced by the working environment and application. The following are the main characteristics observed in typical industrial settings:
1. High Efficiency in Dust Removal
In industries where air quality is critical, such as pharmaceuticals or food processing, the pulse dust removal system excels. The filter media (synthetic or glass fibers) achieves over 99% removal rates for particles as small as 1 micron. The automated pulse jet cleaning ensures the filter remains clean, preventing clogging and maintaining consistent airflow. This is crucial for meeting strict environmental regulations and ensuring product quality.
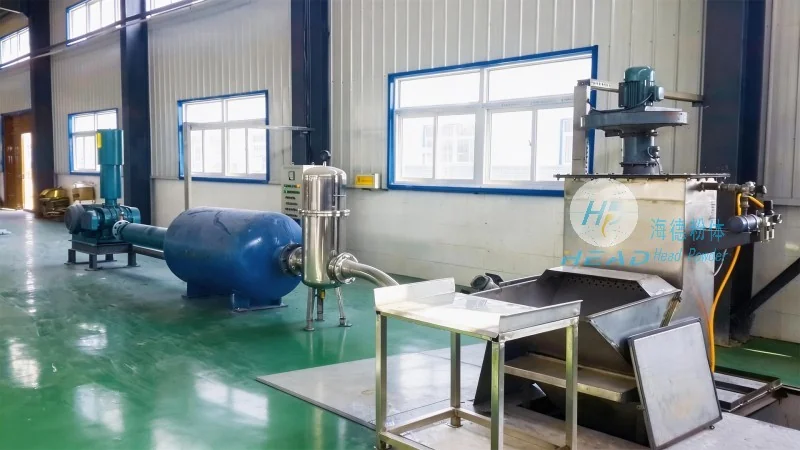
2. Reliable Powder Conveying Performance
The pneumatic conveying system handles diverse powders, from free-flowing cement to cohesive plastic resin. The blower provides sufficient air velocity for long-distance transport (up to several hundred meters) with minimal loss and high throughput. In cement plants or chemical factories, it efficiently transports powders while minimizing material waste. The system’s adaptability to dry and slightly moist powders makes it suitable for various production processes.
3. Low Maintenance and Long Service Life
One of the equipment’s advantages is low maintenance. The automated pulse jet cleaning reduces manual intervention, lowering labor costs. Filter bags are durable, with anti-static and anti-corrosion properties to withstand harsh conditions. Regular maintenance (e.g., replacing filter bags or checking blower performance) is straightforward, extending the equipment’s service life to over 10 years with proper care. This makes it a cost-effective solution for industrial operations.
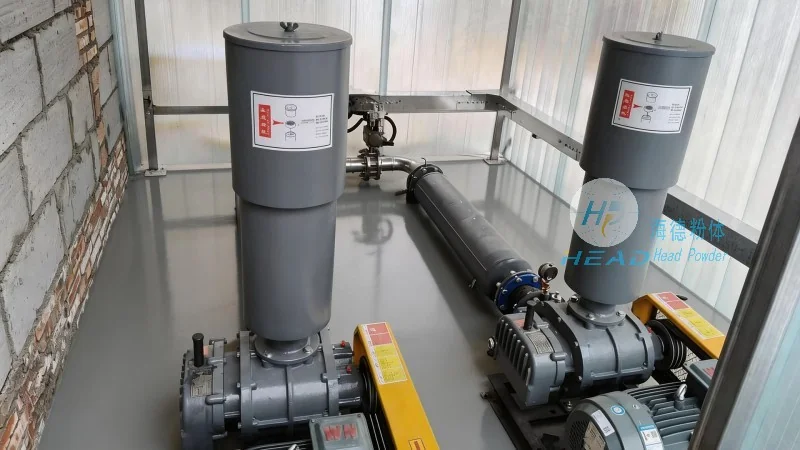
4. Adaptability to Different Industries
The equipment’s versatility allows application in multiple industries. In the chemical sector, it transports reactive powders while ensuring safety and preventing dust explosions. In metallurgy, it handles metal powders and dust from smelting processes, improving working conditions. In building materials, it’s essential for transporting cement and gypsum. The modular design enables customization of filter types, blower capacity, and pipeline dimensions to meet specific application needs.
Conclusion
Pulse dust removal powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd., offers a cutting-edge solution for industrial dust management and material transport. By combining efficient dust removal with reliable pneumatic conveying, the equipment enhances productivity while maintaining a safe and clean environment. Its adaptability to various industries and working conditions, along with low maintenance requirements, makes it an ideal choice for modern industrial applications. As industries prioritize sustainability and operational efficiency, such equipment plays a crucial role in meeting these demands, ensuring long-term success and compliance with environmental regulations.




