HeadPowder, a leading provider of industrial powder handling solutions, specializes in advanced equipment designed to streamline the process of feeding and conveying bulk powders from tonne bags. This article explores the core principles behind the operation of automatic tonne bag feeding and powder conveying systems, as well as the key working scene characteristics that make them indispensable in modern industrial applications.
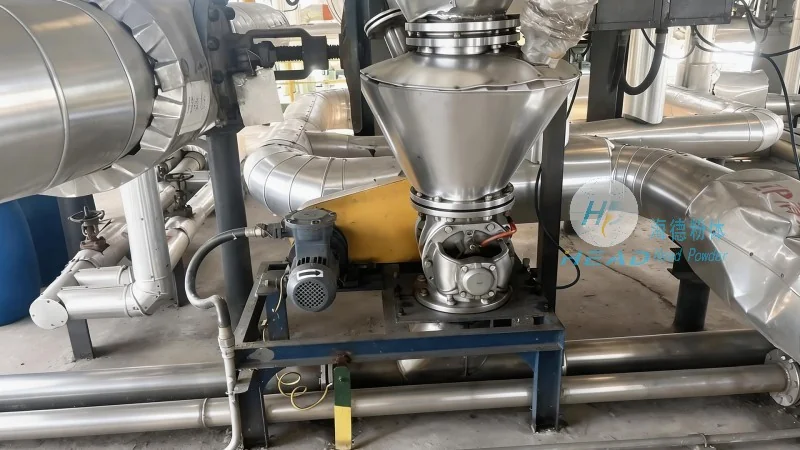
Company Profile and Background
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has built a strong reputation for delivering high-quality, reliable, and efficient powder handling equipment tailored to meet the diverse needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder has become a trusted partner for businesses seeking to optimize their material handling processes.
Understanding Tonne Bag Feeding Systems
The automatic tonne bag feeding system is a critical component in powder handling operations, designed to efficiently extract and transfer bulk powders from large tonne bags. These systems typically consist of several key elements, including a bag opening mechanism, a hopper or container for collecting the material, and a conveying system to transport the powder to the next stage of processing. The principle of operation involves the controlled opening of the tonne bag, allowing the powder to flow into the hopper under gravity or with the assistance of a vacuum or pressure system. This method ensures minimal material loss and maximizes the utilization of the bulk material.
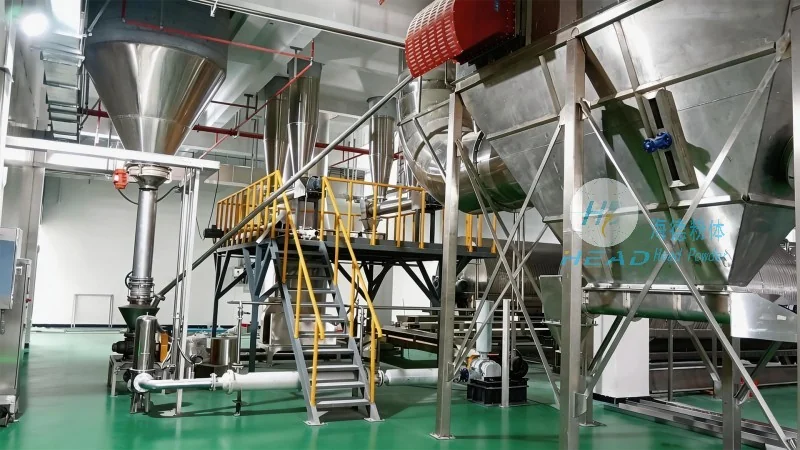
Core Working Principles of the Equipment
The automatic tonne bag feeding and powder conveying equipment operates based on a combination of mechanical and pneumatic principles. The system begins with the placement of a tonne bag onto a designated feeding platform. A mechanical or pneumatic device then opens the bag, either by cutting the top or using a valve to release the contents. The powder is then drawn into a hopper or a storage bin through a hopper lid or a sealed inlet. From there, a conveying system—such as a screw conveyor, pneumatic conveyor, or a combination of both—transports the powder to the processing unit. The control system, often integrated with sensors and automation technology, monitors the flow rate, bag level, and system performance, ensuring consistent and reliable operation. This automation minimizes human intervention, reduces labor costs, and enhances safety in the workplace.
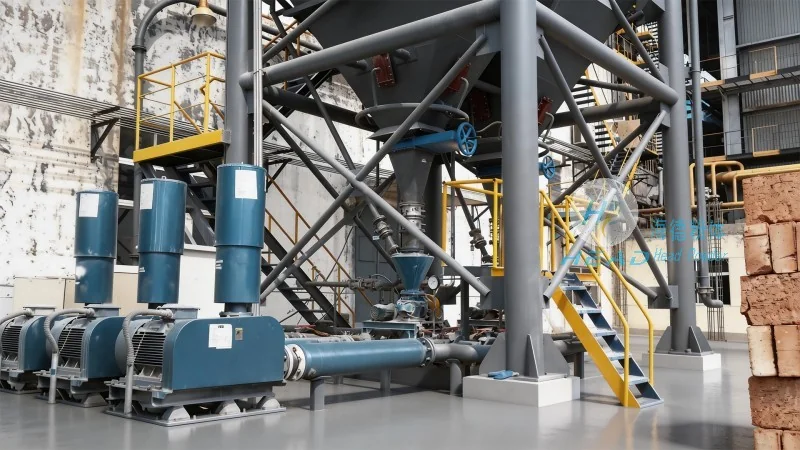
Key Working Scene Characteristics
The working scene characteristics of the automatic tonne bag feeding and powder conveying equipment are tailored to meet the demands of various industrial environments. These systems are designed to handle a wide range of powder types, including fine powders, granules, and bulk materials, with varying densities and flow properties. The equipment is built to withstand harsh operating conditions, such as high temperatures, dust, and moisture, ensuring long-term durability and reliability. In addition, the compact design of these systems allows for easy integration into existing production lines, minimizing the need for extensive modifications to the facility. The automation and precision of the equipment also contribute to improved product quality and reduced waste, making it a valuable asset for any industrial operation.
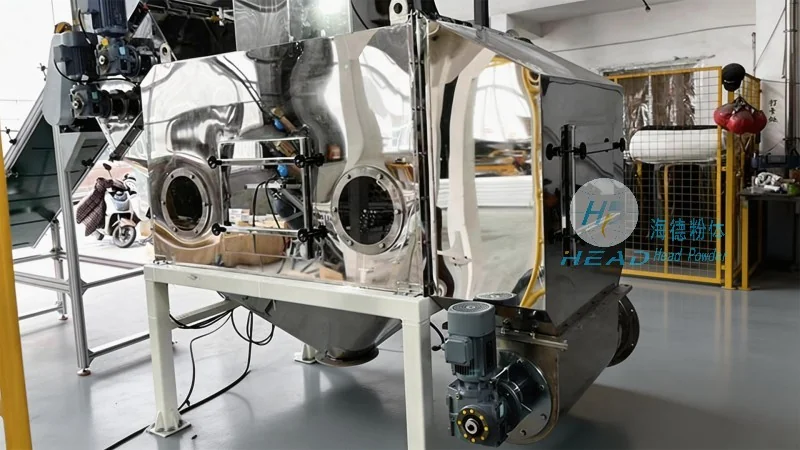
Applications and Industry Impact
The automatic tonne bag feeding and powder conveying equipment is widely used across multiple industries, including pharmaceuticals, food processing, chemicals, and mining. In the pharmaceutical industry, for example, these systems are crucial for handling sensitive powders, ensuring that the material is transferred without contamination or degradation. In the food industry, the equipment is used to process ingredients such as flour, sugar, and spices, maintaining hygiene and product quality. The chemical industry relies on these systems for handling various chemicals, from powders to granules, while the mining industry uses them to transport raw materials from storage to processing plants. The consistent and reliable operation of the equipment helps to improve overall productivity and efficiency in these industries, contributing to cost savings and enhanced operational performance.
Conclusion and Future Outlook
Automatic tonne bag feeding and powder conveying equipment, as provided by HeadPowder, represents a significant advancement in industrial material handling. By combining advanced automation, precision control, and robust design, these systems offer a solution to the challenges of efficiently handling bulk powders from tonne bags. The working scene characteristics, including adaptability to various powder types, durability in harsh environments, and ease of integration, make them a versatile choice for modern industrial applications. As industries continue to seek more efficient and reliable solutions, the demand for such equipment is expected to grow, further solidifying its role in the future of industrial processing.




