Gravity dust removal material conveying systems represent a critical component in industrial processes, particularly in environments where efficient handling of bulk materials and air purification are paramount. These systems are designed to combine material transport with dust collection, offering a cost-effective solution for industries such as power generation, cement production, and chemical processing. The core principle of these systems leverages gravity to facilitate material movement while simultaneously capturing airborne particles, making them an essential tool for maintaining air quality and operational efficiency.
The Fundamental Principle of Gravity Dust Removal
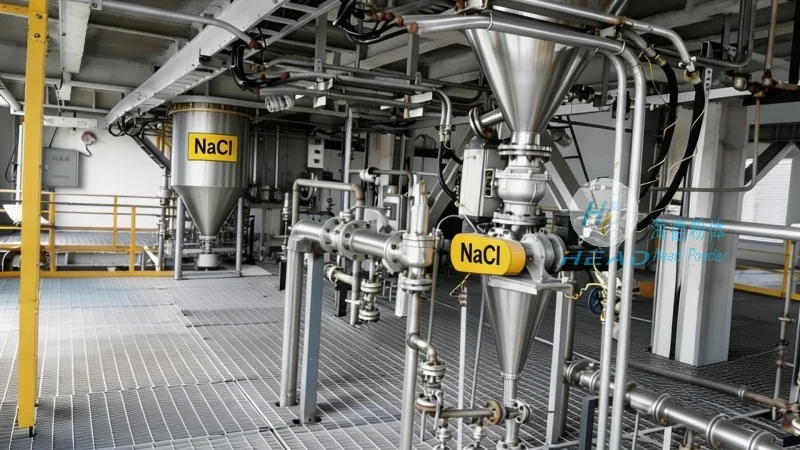
The operation of gravity dust removal material conveying systems is based on the principle of gravity-assisted material flow combined with air filtration. In these systems, bulk materials are fed into a vertical or inclined duct, where the material's weight causes it to move downward under the influence of gravity. Simultaneously, the system incorporates a dust collection mechanism, typically involving a hopper or cyclone, which traps fine particles from the air as the material flows. This dual functionality ensures that the material is conveyed while contaminants are removed, preventing dust dispersion into the surrounding environment. The design often includes a series of components such as feed hoppers, conveying chutes, and dust collection chambers, all working in tandem to achieve the desired outcome.
Key Working Scene Characteristics
The effectiveness of gravity dust removal material conveying systems is heavily influenced by the specific working environment and operational conditions. Several key characteristics define their performance and suitability in various industrial settings:
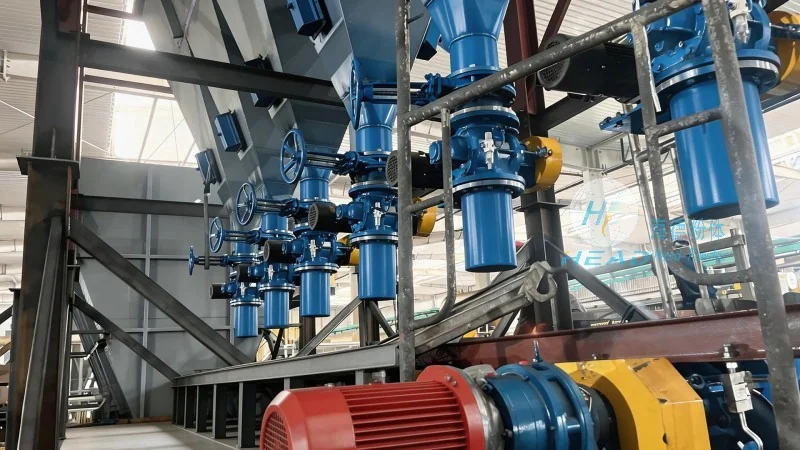
1. **Vertical Conveying Efficiency**: In applications where vertical space is limited or vertical transport is required, these systems excel. The use of gravity reduces the need for mechanical power, making vertical conveyance both energy-efficient and cost-effective. This is particularly advantageous in facilities where horizontal space is constrained, such as in power plants or industrial plants with compact layouts.
2. **Dust Control and Air Quality Management**: A primary advantage of these systems is their ability to maintain high air quality by capturing dust particles during material transport. The integrated dust collection mechanisms, often including bag filters or cyclones, ensure that fine particulates are retained, preventing pollution and complying with environmental regulations. This is crucial in industries where air emissions are strictly monitored, such as cement manufacturing or chemical processing.
3. **Material Compatibility and Handling**: Gravity dust removal systems are versatile and can handle a wide range of materials, including powders, granules, and bulk solids. The design accommodates different material densities and flow characteristics, making them suitable for diverse applications. For instance, in power plants, these systems are used to transport fly ash from boilers, while in cement plants, they handle raw materials and clinker. The ability to handle abrasive or corrosive materials without significant wear on components further enhances their operational reliability.
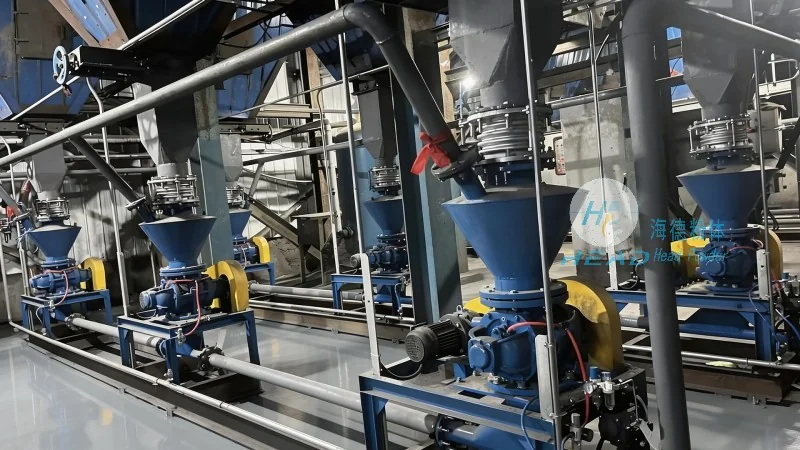
4. **Space Optimization and Installation Flexibility**: These systems are designed for easy installation and can be integrated into existing industrial setups with minimal disruption. Their compact design allows for vertical or inclined configurations, making them ideal for facilities with limited horizontal space. The modular nature of the components enables customization to fit specific plant layouts, ensuring that the system can be adapted to meet the unique requirements of each operation.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of industrial material handling and dust removal solutions. With operations based in Shandong, China, the company specializes in designing, manufacturing, and implementing advanced gravity dust removal material conveying systems tailored to the needs of various industries. HeadPowder's commitment to innovation and quality ensures that their systems meet the highest standards of efficiency, reliability, and environmental compliance. By leveraging decades of experience in the field, the company delivers customized solutions that enhance operational performance while reducing environmental impact.




