For industrial applications involving calcium nitrite, the efficient and reliable transportation of this material is crucial. The calcium nitrite material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., a leading company based in Shandong, China, is engineered to meet these demands. This system integrates advanced technology and robust design to ensure safe and effective material transport, supporting various industrial processes where calcium nitrite is utilized.
Overview of the Calcium Nitrite Material Handling System
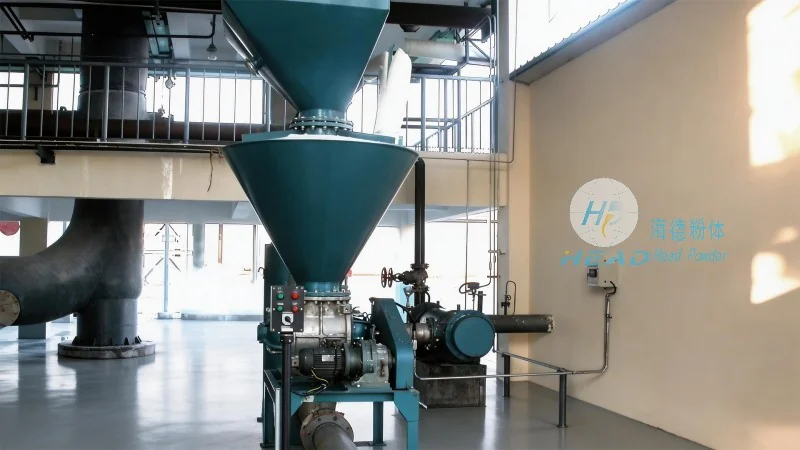
The calcium nitrite material handling system is a comprehensive solution designed to handle the transportation of calcium nitrite, a chemical compound widely used in industrial applications such as water treatment, food preservation, and chemical synthesis. The system comprises several key components, including storage silos, conveying equipment, control systems, and safety mechanisms, all working in harmony to facilitate the smooth flow of material from storage to processing or distribution points. HeadPowder, as the manufacturer, emphasizes the importance of durability, efficiency, and safety in its design, ensuring that the system can operate under demanding conditions while maintaining high performance standards.
Operation Process of the Calcium Nitrite Material Handling System
The operation process of the calcium nitrite material handling system begins with the loading of material into the storage silo. The system uses a hopper or loading chute to feed the material into the silo, where it is stored under controlled conditions to prevent degradation or caking. Once the material is ready for transport, the control system initiates the conveying process. The conveying equipment, typically a screw conveyor or pneumatic system, moves the material from the silo to the discharge point. The system is equipped with sensors and monitoring devices that track the material level, flow rate, and pressure, ensuring that the operation is conducted safely and efficiently. The discharge point may be connected to a processing unit or a packaging system, where the material is further processed or prepared for distribution. Throughout the operation, the control system continuously adjusts parameters to maintain optimal performance, such as adjusting the speed of the conveyor or the pressure in the pneumatic system to accommodate variations in material load or flow.
Working Principle of the Calcium Nitrite Material Handling System
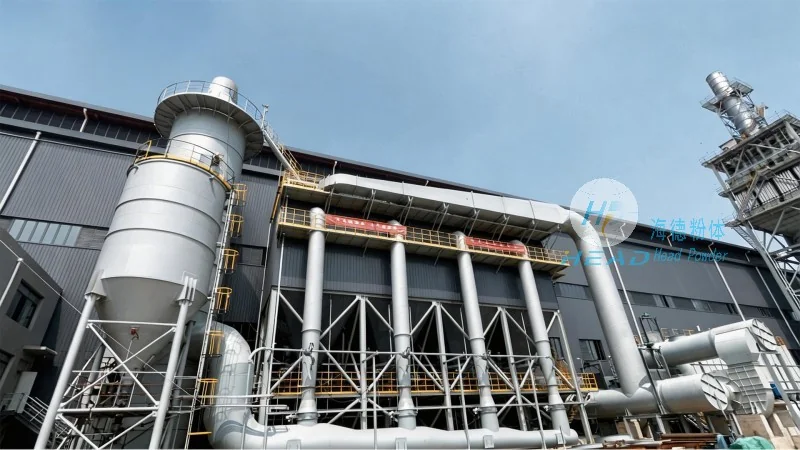
The working principle of the calcium nitrite material handling system is based on the principles of mechanical and pneumatic conveying, tailored to handle the specific properties of calcium nitrite. The system utilizes a combination of gravity and mechanical force to move the material through the conveying line. In the case of a screw conveyor, the rotating screw blade pushes the material forward, while the hopper and silo maintain a consistent material level. For pneumatic systems, the material is carried by a stream of air or gas, which is introduced into the conveying line through a blower or compressor. The system is designed to handle both dry and slightly moist calcium nitrite, with appropriate modifications to the conveying equipment to prevent material buildup or blockages. The control system plays a critical role in regulating the flow, ensuring that the material is transported at a consistent rate without causing excessive wear on the equipment. Safety features, such as pressure relief valves and emergency stop buttons, are integrated into the system to prevent accidents and protect personnel. The overall design of the system prioritizes energy efficiency, with optimized conveying speeds and minimal energy consumption, making it an economical choice for industrial applications.
Key Features and Benefits of the Calcium Nitrite Material Handling System
Shandong HeadPowder Engineering Co., Ltd. has incorporated several key features into the calcium nitrite material handling system to enhance its performance and reliability. These features include: advanced control systems with real-time monitoring capabilities, robust construction to withstand harsh industrial environments, and flexible design that can be customized to meet specific customer requirements. The system offers several benefits, including improved material handling efficiency, reduced downtime due to maintenance, and enhanced safety for operators. By using this system, industrial facilities can ensure consistent and reliable supply of calcium nitrite, supporting their production processes and maintaining compliance with safety regulations. The system's durability and low maintenance requirements also contribute to long-term cost savings, making it a valuable investment for businesses in the chemical and industrial sectors.
Application Examples and Industry Impact
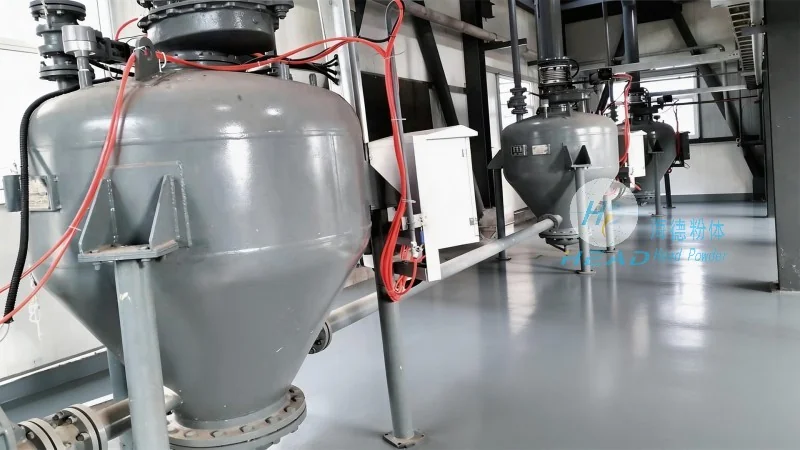
The calcium nitrite material handling system is widely used in various industries where calcium nitrite is a critical component. In the water treatment industry, the system is used to transport calcium nitrite to water treatment plants, where it is added to the water supply to control corrosion and scale formation. In the food industry, the system is used to deliver calcium nitrite to food processing facilities, where it is used as a preservative in meat products. In the chemical industry, the system is used to transport calcium nitrite to chemical synthesis plants, where it is used as a raw material in the production of other chemicals. The system's ability to handle large volumes of material efficiently and safely has a significant impact on the productivity and profitability of these industries. By ensuring a consistent supply of calcium nitrite, the system helps to maintain production schedules and meet customer demands, contributing to the overall success of the businesses.
Conclusion and Future Developments
The calcium nitrite material handling system developed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in material handling technology for calcium nitrite applications. The system's operation process and working principle are designed to provide reliable and efficient transportation of the material, supporting various industrial processes. With its robust design, advanced control systems, and safety features, the system meets the high standards of industrial applications. As technology continues to evolve, HeadPowder is committed to further improving the system, incorporating new materials and technologies to enhance performance and reduce costs. The future of the calcium nitrite material handling system looks promising, with continued focus on innovation and customer satisfaction. By leveraging the expertise of HeadPowder, industrial facilities can ensure that their material handling processes are optimized, efficient, and safe, contributing to the overall success of their operations.




