Aluminum sulfate, commonly known as alum, is a widely used chemical compound in various industrial applications, including water treatment, paper manufacturing, and chemical processing. The efficient and safe handling of aluminum sulfate is crucial for industrial operations, and pneumatic conveyors have emerged as a reliable solution for transporting this material. This article provides an overview of the pneumatic conveyor system designed for aluminum sulfate, detailing its structural components and operational principles.
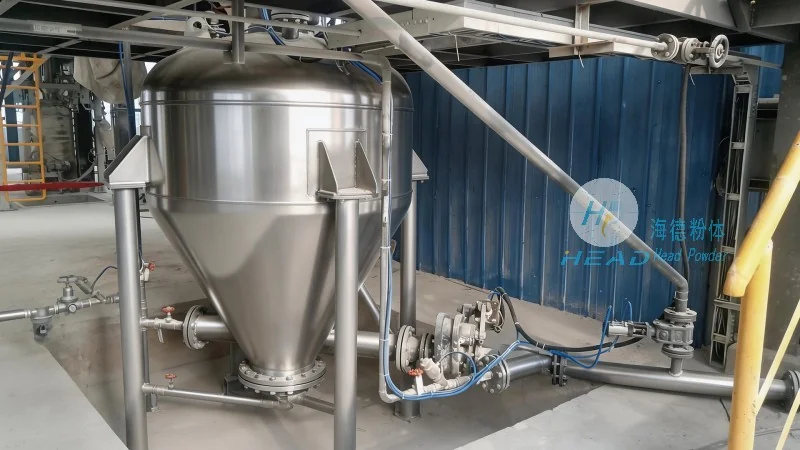
Structural Components of the Aluminum Sulfate Pneumatic Conveyor
The aluminum sulfate pneumatic conveyor system consists of several key components that work in tandem to facilitate material transport. The primary components include a hopper for material storage, a feeder mechanism to control the flow of aluminum sulfate into the conveyor, a pipeline system for transporting the material, and a receiver for depositing the material at the destination. The hopper is typically designed with a sloped bottom to ensure smooth material discharge, while the feeder may employ a rotary valve or screw mechanism to regulate the flow rate. The pipeline system is usually made of corrosion-resistant materials such as stainless steel or PVC to withstand the chemical properties of aluminum sulfate. The receiver is equipped with a discharge valve to allow controlled unloading of the material.
Working Principle of the Pneumatic Conveyor
The pneumatic conveyor operates on the principle of using air pressure to move aluminum sulfate particles through the pipeline. The system can be classified as either a positive pressure or negative pressure (vacuum) system. In a positive pressure system, compressed air is introduced into the hopper, forcing the aluminum sulfate into the pipeline. The air and material mixture travels through the pipeline to the receiver, where the air is separated from the material and recirculated. In a negative pressure system, a vacuum is created at the receiver, drawing the aluminum sulfate and air mixture from the hopper through the pipeline. The air serves as the carrier medium, transporting the aluminum sulfate particles efficiently. The velocity of the air and the size of the particles determine the optimal air flow rate for effective conveying.
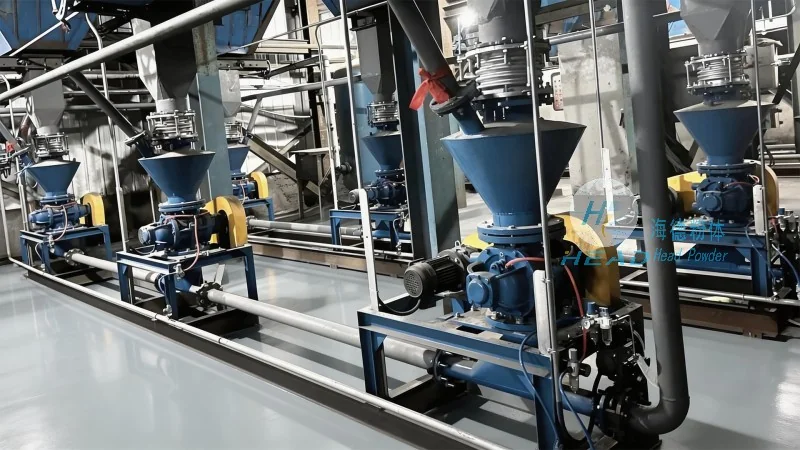
Advantages of Using a Pneumatic Conveyor for Aluminum Sulfate
Employing a pneumatic conveyor for aluminum sulfate offers several advantages over traditional methods like belt conveyors or bucket elevators. One of the key benefits is the ability to handle the material in a closed system, minimizing dust generation and environmental contamination. This is particularly important for aluminum sulfate, which can be a respiratory irritant if not handled properly. The closed system also prevents material loss and cross-contamination, ensuring product purity. Additionally, pneumatic conveyors are highly flexible and can be easily integrated into existing industrial layouts, allowing for changes in material flow direction or destination without major modifications. The system is also relatively compact, requiring less floor space compared to other bulk material handling equipment. Furthermore, the conveying process is continuous and can be automated, improving operational efficiency and reducing labor costs.
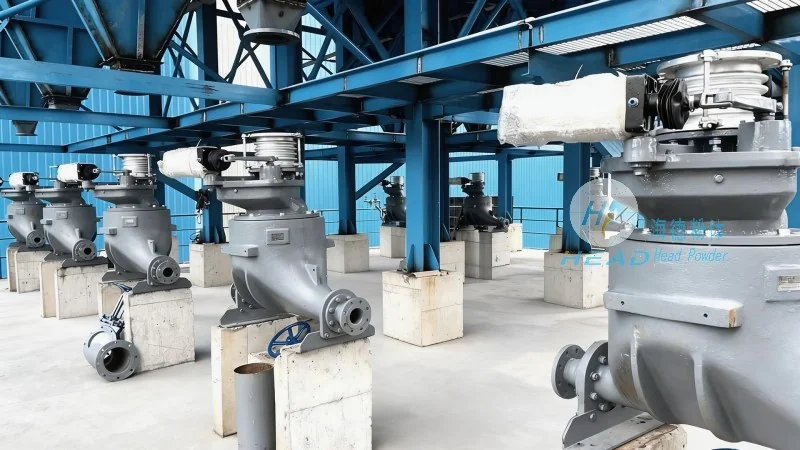
Application Examples and Operational Considerations
The aluminum sulfate pneumatic conveyor is widely used in various industrial settings. For instance, in water treatment plants, it is used to transport aluminum sulfate slurry to the treatment tanks. In paper mills, it is employed to move the chemical to the paper-making process. The system's performance depends on several factors, including the particle size distribution of the aluminum sulfate, the moisture content, and the desired conveying distance. Proper sizing of the hopper, feeder, and pipeline is essential to ensure smooth operation and prevent blockages. Regular maintenance, such as cleaning the pipeline and checking the air filter, is necessary to maintain the system's efficiency and longevity. The choice between positive and negative pressure systems depends on the specific application requirements, such as the distance to be covered and the material characteristics.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of bulk material handling equipment, including pneumatic conveyors. With a focus on innovation and quality, the company has developed advanced solutions tailored to the needs of various industries. The company's expertise in material handling systems ensures that clients receive reliable and efficient equipment for their aluminum sulfate transportation needs. Headpowder's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the chemical and industrial sectors.




