HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced dust-free metering pneumatic conveying systems. These systems are engineered to handle a wide range of powders and bulk materials with precision and efficiency, ensuring minimal contamination and optimal performance in industrial applications.
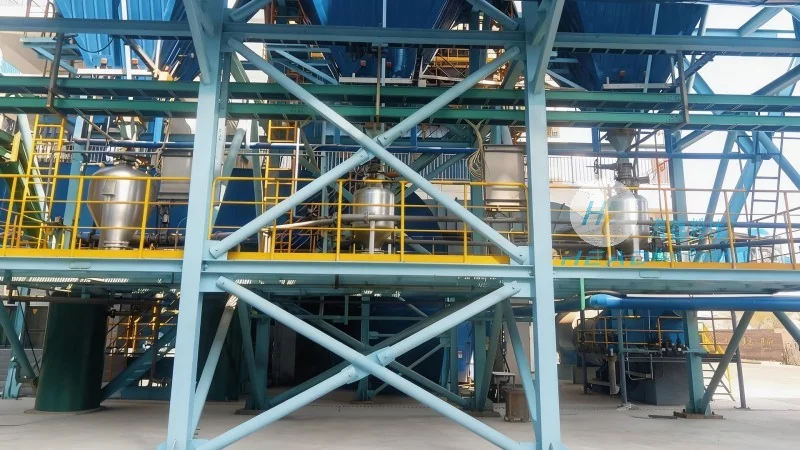
Overview of the Dust-Free Metering Pneumatic Conveying System
The dust-free metering pneumatic conveying system is a sophisticated piece of equipment designed to transport powders and granular materials in a controlled, clean environment. At the core of this system is a metering device that accurately measures the material flow rate, ensuring consistent and reliable delivery. The system integrates various components, including a dust collector, a conveying pipeline, and a control unit, all working in harmony to achieve seamless material transfer.
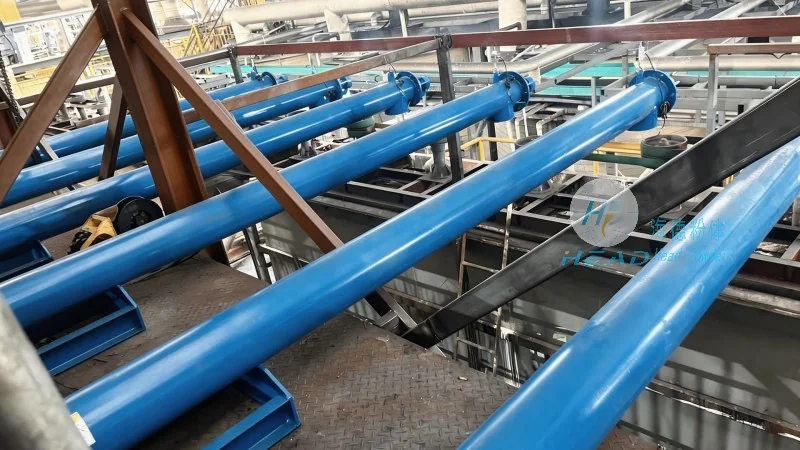
Structural Components and Working Principles
The system's structure comprises several key components, each playing a crucial role in the overall operation. The metering unit, typically a rotary valve or a positive displacement pump, regulates the material flow by measuring and controlling the volume of material being conveyed. The conveying pipeline, often made of stainless steel or other corrosion-resistant materials, transports the material from the source to the destination. A dust collector is integrated to capture any airborne particles, maintaining a clean and safe working environment. The control unit monitors and adjusts the system parameters in real-time, ensuring optimal performance and preventing operational issues.
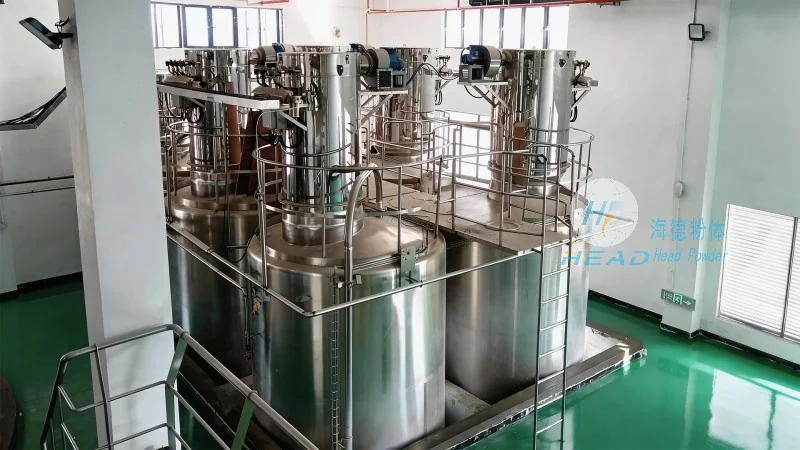
Key Features and Benefits
HeadPowder's dust-free metering pneumatic conveying systems offer several advantages that make them ideal for industries requiring high-purity material handling. The systems are designed to minimize product contamination, which is critical in pharmaceutical, food, and chemical industries. The precise metering capability ensures accurate dosing, improving process efficiency and reducing waste. Additionally, the dust-free design enhances workplace safety by reducing airborne particulates, complying with environmental regulations and improving overall operational health.
Application Scenarios
These systems are widely used in various industrial sectors, including pharmaceutical manufacturing, food processing, chemical production, and cement processing. In pharmaceutical applications, the dust-free design ensures that the materials remain sterile and free from contaminants, meeting stringent regulatory requirements. In food processing, the system maintains product purity and safety, adhering to food safety standards. In chemical industries, the system handles reactive or hazardous materials with precision, minimizing the risk of accidents and ensuring product quality. The versatility of the system allows it to adapt to different material types and processing requirements, making it a reliable solution for diverse industrial needs.
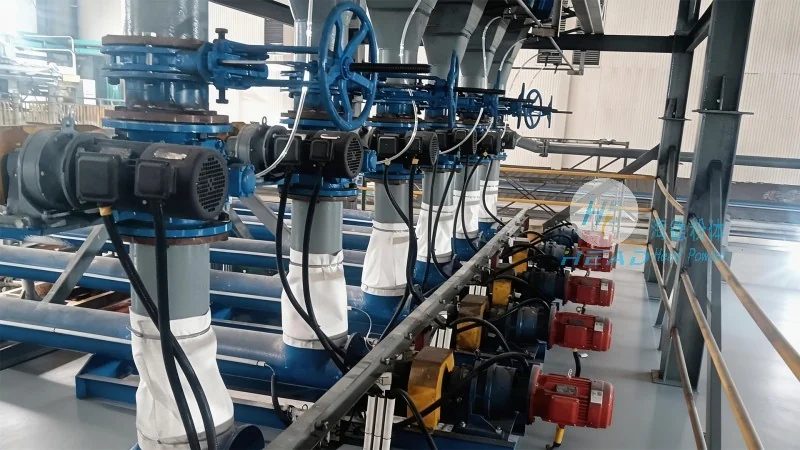
Technical Specifications and Customization Options
HeadPowder provides customizable solutions tailored to specific customer requirements. The systems can be configured with different metering devices, pipeline sizes, and material handling capacities to suit various applications. Technical specifications include flow rates ranging from a few kilograms per hour to several tons per hour, depending on the system's design. The materials used in the construction, such as stainless steel, are selected for their durability and resistance to corrosion, ensuring long-term performance. The control systems are equipped with advanced features, including real-time monitoring, alarm functions, and data logging, enhancing operational control and maintenance efficiency.




