For industries dealing with oxidized vanadium powders, efficient and reliable powder handling is crucial. The oxidized vanadium powder conveying system is a specialized solution designed to manage the transportation of these materials with precision and safety. This article explores the fundamental aspects of such systems, including their design principles and operational benefits.
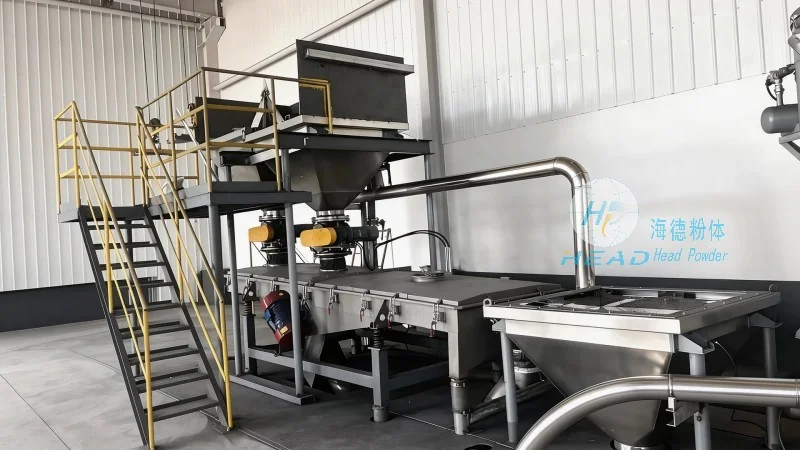
Understanding the Oxidized Vanadium Powder Conveying System
The oxidized vanadium powder conveying system is engineered to handle the unique challenges associated with transporting vanadium oxide powders. These materials are often used in various industrial applications, including chemical processing, battery manufacturing, and catalyst production. The system is designed to ensure that the powder is moved from one location to another without degradation, contamination, or loss. Key components typically include feeding mechanisms, conveying equipment, and control systems that work in tandem to maintain the integrity of the material throughout the process.
Design Principles of the Oxidized Vanadium Powder Conveying System
The design of an oxidized vanadium powder conveying system follows several critical principles to ensure optimal performance. First, the system must be capable of handling the specific physical properties of vanadium oxide powders, such as particle size, density, and flow characteristics. This involves selecting appropriate equipment like screw conveyors, pneumatic conveyors, or bucket elevators, depending on the application requirements. Second, the system must prioritize safety and environmental compliance, as vanadium compounds can be hazardous if not handled properly. This includes features like dust collection systems, explosion-proof designs, and material containment measures. Third, the design emphasizes energy efficiency and operational reliability, minimizing downtime and maintenance costs. The integration of advanced control technologies, such as variable frequency drives and real-time monitoring, further enhances the system's performance and adaptability.
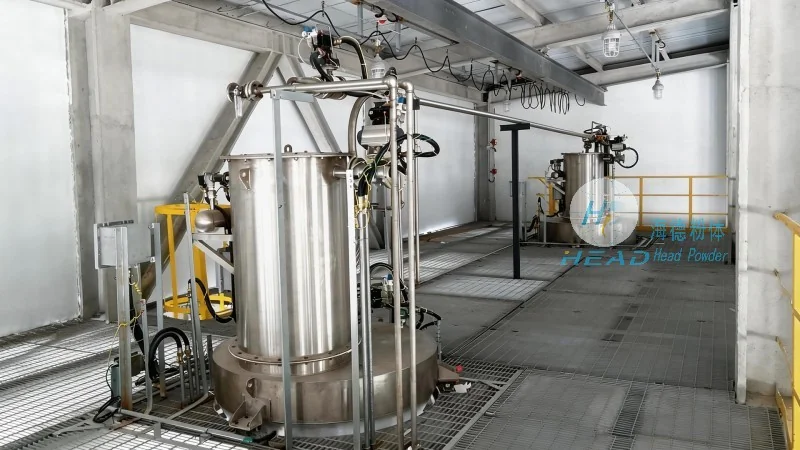
Key Components and Their Functions
Several key components make up an effective oxidized vanadium powder conveying system. The feeding unit, often a hopper or a rotary valve, ensures a consistent and controlled flow of the powder into the conveying equipment. The conveying mechanism, which could be a screw conveyor, pneumatic pipeline, or bucket elevator, transports the powder from the source to the destination. The control system, including sensors and programmable logic controllers (PLCs), monitors the process parameters and adjusts the operation as needed. Additionally, dust suppression and filtration systems are critical to maintaining air quality and preventing dust-related hazards. Each component is carefully selected and integrated to ensure the system operates smoothly and meets the specific needs of the application.
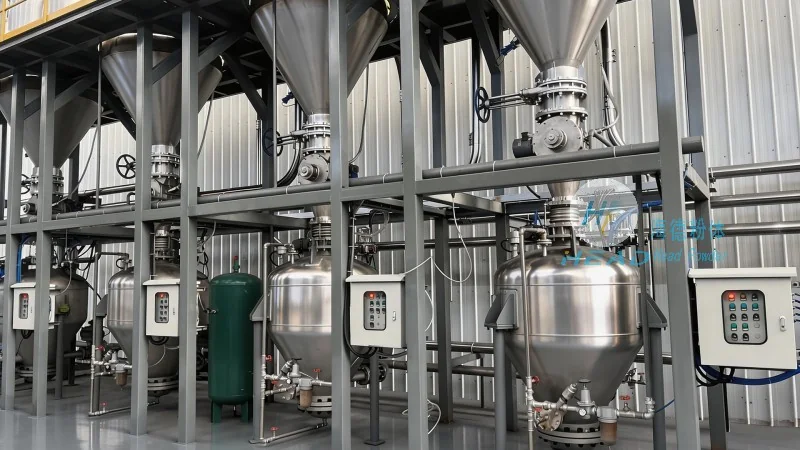
Applications and Benefits
Oxidized vanadium powder conveying systems are widely used in various industries due to their versatility and efficiency. In the chemical industry, they are used to transport vanadium oxide powders for the production of vanadium pentoxide, a key component in battery cathodes. In the battery manufacturing sector, these systems ensure the precise delivery of vanadium compounds to production lines, improving product quality and consistency. The benefits of using such systems include improved material handling efficiency, reduced risk of contamination and loss, enhanced safety through proper containment, and lower operational costs over time. By leveraging advanced design principles and components, these systems provide a reliable solution for industries that rely on vanadium oxide powders.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of specialized powder handling systems. With a focus on innovation and quality, the company designs and produces equipment tailored to the unique needs of various industries. Headpowder's expertise in oxidized vanadium powder conveying systems reflects their commitment to providing reliable, efficient, and safe solutions for their clients. Based in Shandong, China, the company leverages local manufacturing capabilities and global market knowledge to deliver high-performance systems that meet international standards. Their products are known for durability, precision, and adaptability, making them a trusted choice for businesses requiring advanced powder handling solutions.




