The rice husk ash material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder), is a specialized solution designed to efficiently transport and manage rice husk ash, a byproduct commonly used in power generation and other industrial applications. HeadPowder, a leading manufacturer based in Shandong, China, has focused on optimizing material handling processes for agricultural and industrial waste, ensuring high efficiency and reliability in its systems.
Working Principle of the Rice Husk Ash Material Handling System
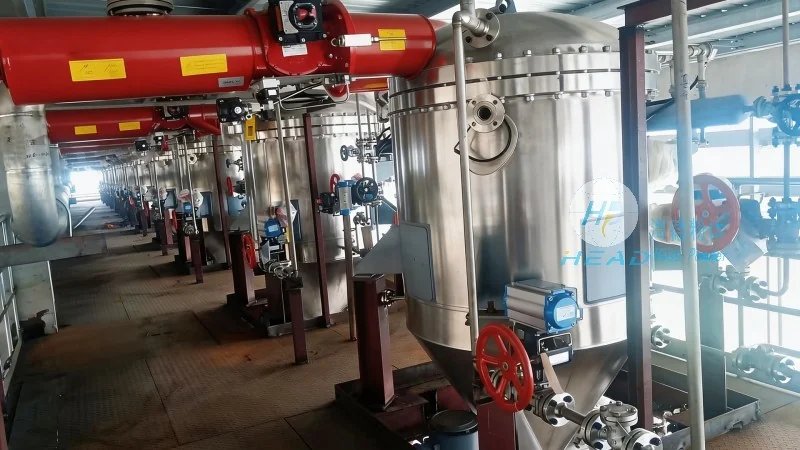
The system operates on a combination of mechanical and pneumatic principles, tailored to handle the unique characteristics of rice husk ash. The core components include a hopper for material storage, a conveyor system (such as belt or screw conveyors) for primary transport, and a pneumatic conveying unit for long-distance or complex routing. The hopper is equipped with a feeding mechanism that ensures a consistent flow of ash into the conveyor. The conveyor transports the material to the pneumatic unit, where air is introduced to create a slurry or dust stream that is then directed to the target location. This integrated approach minimizes material degradation and maximizes throughput, making it suitable for large-scale operations. The feeding mechanism, often a rotary valve or vibratory feeder, regulates the flow rate to match the conveyor's capacity, preventing overloading and ensuring smooth operation. The conveyor system, selected based on the ash's bulk density and flowability, may use belt conveyors for horizontal or slight incline transport or screw conveyors for vertical lifting. The pneumatic unit, typically a positive displacement blower or rotary airlock, generates the necessary air pressure to move the ash through the pipeline. The pipeline is designed with appropriate diameter and slope to maintain the flow, with bends and elbows minimized to reduce pressure loss and material deposition.
Key Features of the Rice Husk Ash Material Handling System
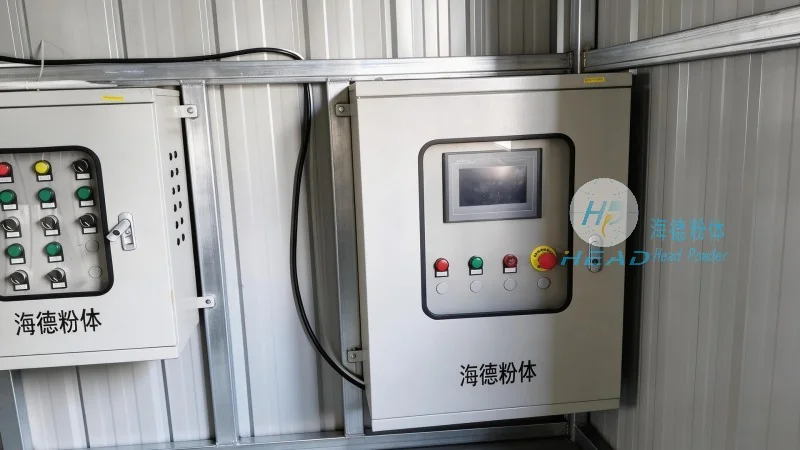
Several distinctive features set this system apart in the market. Firstly, the system is designed with low maintenance in mind, featuring durable components that can withstand the abrasive nature of rice husk ash. The conveyor and pneumatic units are constructed from corrosion-resistant materials, such as stainless steel or high-grade alloys, reducing the need for frequent repairs and extending the equipment's service life. Secondly, the system offers high efficiency in material transport, with adjustable speed controls that allow operators to optimize throughput based on production demands. This flexibility is crucial for adapting to varying ash volumes and processing rates, such as during peak power generation periods or seasonal agricultural waste processing. Thirdly, the system incorporates advanced control systems that monitor pressure, flow, and temperature in real-time, providing operators with immediate feedback and enabling proactive maintenance. These systems may include sensors and a central control panel that alerts operators to potential issues, such as blockages or pressure drops, allowing for quick intervention. Additionally, the design prioritizes safety, with enclosed structures and emergency shut-off mechanisms to prevent dust emissions and ensure a secure working environment. The system may also include dust collection and filtration components to comply with environmental regulations, further enhancing its safety and reliability.
Application Scenarios and Practical Benefits
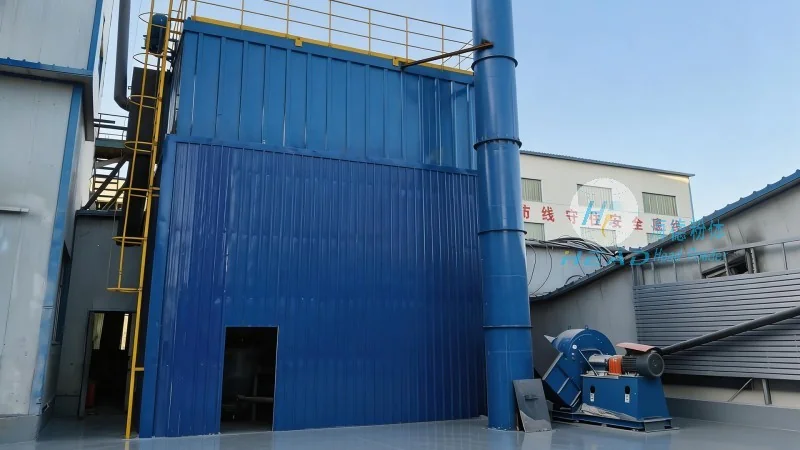
The rice husk ash material handling system is widely used in power plants, biomass energy facilities, and agricultural processing plants. In power plants, it efficiently transports ash from combustion chambers to storage silos, reducing manual handling risks and improving operational safety. For example, in coal-fired power plants, rice husk ash is often used as a co-fuel, and the system ensures a continuous supply of ash to the boiler, enhancing energy efficiency. In biomass energy facilities, the system supports the continuous supply of ash to combustion systems, enhancing energy production efficiency. The practical benefits of this system include reduced labor costs, as automated transport reduces the need for manual handling, and minimized material loss, as the system is designed to prevent spillage and degradation. Additionally, improved environmental compliance due to lower dust emissions is a key advantage, as the enclosed design and filtration systems reduce air pollution. HeadPowder's commitment to quality and innovation has made this system a preferred choice for industries seeking reliable and sustainable material handling solutions, with many clients reporting increased operational efficiency and reduced maintenance costs after implementing the system.




