For industrial applications that involve the transportation of cement, gray mineral powders, and similar bulk materials, efficient material handling systems are crucial for maintaining productivity and operational safety. The equipment designed for these tasks, such as conveyor systems, pneumatic conveyors, and bulk material handling solutions, plays a vital role in ensuring smooth material flow from storage to processing or packaging stages. This article will explore the working principles and key features of such systems, providing insights into how they enhance operational efficiency in industrial settings.
Working Principle of Cement and Mineral Powder Material Handling Systems
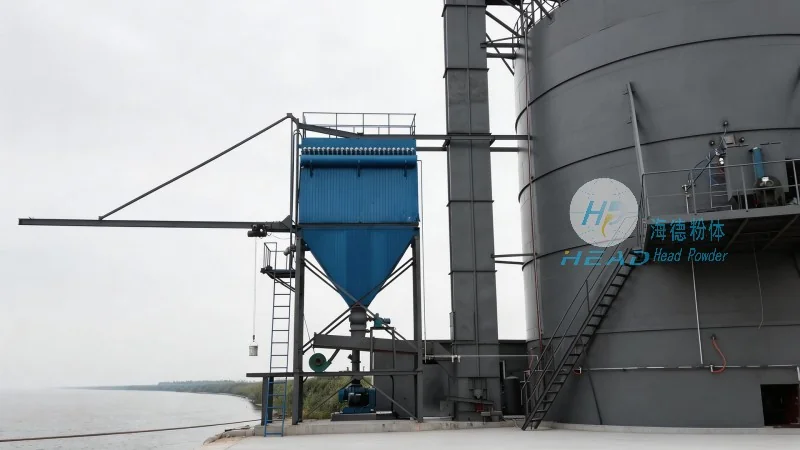
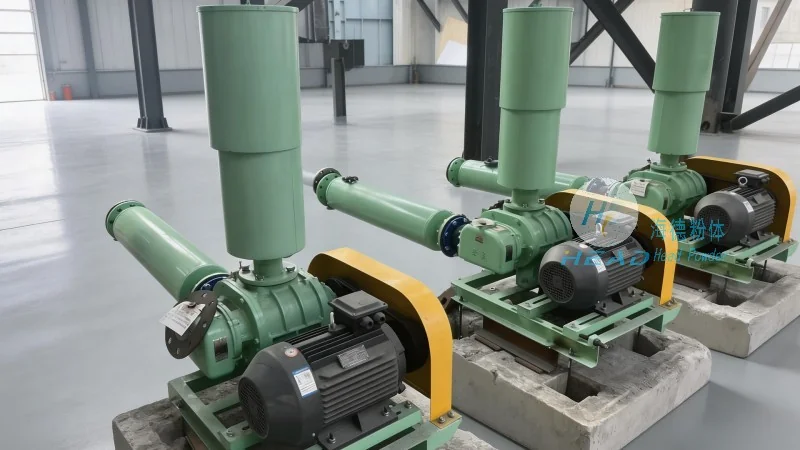
The core working principle of cement and mineral powder material handling systems revolves around the efficient transfer of bulk materials from one location to another. These systems typically employ mechanical or pneumatic mechanisms to move materials through pipelines, conveyor belts, or storage silos. For example, pneumatic conveying systems use air pressure to transport powders in a closed system, while mechanical conveyors rely on belts, rollers, or buckets to move materials along a designated path. The process begins with material loading from a hopper or storage silo, where the system draws the powder into the conveying line. The system then uses either positive pressure (blowing air into the line) or negative pressure (sucking air out of the line) to propel the material forward. This method ensures that the material is transported without spillage and with minimal dust generation, which is critical for maintaining a clean and safe working environment.
Key Features of Cement and Mineral Powder Material Handling Systems
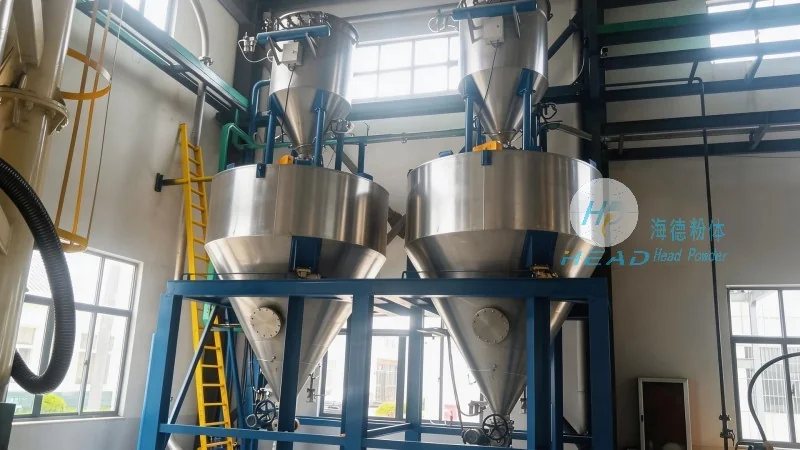
Several key features distinguish high-quality cement and mineral powder material handling systems, making them suitable for demanding industrial applications. Firstly, durability and corrosion resistance are essential, as these systems often handle abrasive materials that can wear down equipment over time. Materials like stainless steel or specialized coatings are commonly used to protect components from corrosion and wear. Secondly, the systems are designed for low maintenance, with features such as easy access to components for cleaning and repair, and self-cleaning mechanisms to prevent material buildup. This reduces downtime and operational costs, which is a significant advantage for industrial operations. Thirdly, energy efficiency is a critical feature, as these systems consume power to operate. Modern systems incorporate energy-saving technologies, such as variable frequency drives (VFDs), which adjust motor speed based on the material load, reducing energy consumption during low-demand periods. Additionally, the systems are equipped with advanced control systems that allow for precise monitoring and adjustment of material flow rates, ensuring optimal performance and minimizing waste.
Application Scenarios and Benefits
Cement and mineral powder material handling systems are widely used in various industries, including cement production, mining, and chemical processing. In cement plants, these systems are essential for transporting raw materials like limestone and clay from storage to the grinding and mixing stages. In mining operations, they help move mineral powders from processing facilities to storage or transportation points. The benefits of using these systems extend beyond efficiency; they also contribute to improved safety and environmental compliance. By minimizing dust emissions and preventing material spillage, these systems help maintain a safe working environment and reduce the risk of environmental contamination. Furthermore, the consistent material flow provided by these systems ensures that downstream processes, such as mixing or packaging, operate smoothly, reducing the likelihood of production delays or quality issues.
Conclusion
In conclusion, cement and mineral powder material handling systems are sophisticated pieces of equipment that play a critical role in modern industrial operations. Their working principles, which often involve pneumatic or mechanical conveying methods, ensure efficient and safe material transfer. The key features, including durability, low maintenance, energy efficiency, and advanced control systems, make these systems reliable and cost-effective solutions for bulk material handling. For industries that rely on the consistent and safe transportation of cement and mineral powders, investing in high-quality material handling systems is essential for maintaining productivity and operational excellence. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems, catering to the diverse needs of industrial clients in China and beyond.




