Styrene, a critical monomer in the production of polystyrene and other polymers, requires efficient and reliable material handling systems to ensure smooth industrial processes. The equipment designed for transporting styrene must meet stringent safety and performance standards, as the material is both flammable and volatile. This article explores the working principle and key features of styrene material handling systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field.
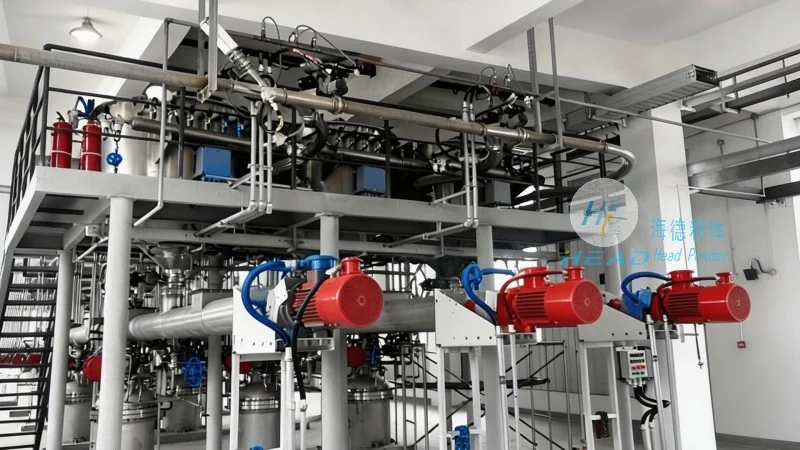
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional enterprise based in Shandong, China. With years of experience in the engineering and manufacturing of material handling solutions, the company specializes in designing and producing equipment tailored for various industrial applications, including the safe and efficient transport of styrene and other hazardous materials. HeadPowder's commitment to quality and innovation has established it as a trusted partner in the chemical and polymer processing industries.
Working Principle of Styrene Material Handling Systems
The working principle of styrene material handling systems typically involves several integrated components working in concert to ensure safe and efficient transport. The system generally includes storage tanks, pumps, pipelines, and control systems. The process begins with the storage of styrene in specialized tanks, which are designed to prevent leaks and maintain the material's stability. From the storage tanks, the styrene is pumped through pipelines using high-performance pumps, which are equipped with safety features such as pressure relief valves and temperature sensors to monitor and regulate the flow. The pipelines are often made of corrosion-resistant materials like stainless steel or special polymers to withstand the chemical properties of styrene. Control systems, including automated valves and monitoring devices, ensure precise control over the flow rate and direction, preventing overfilling or underflow. Additionally, the system may incorporate ventilation and fire suppression mechanisms to mitigate risks associated with the flammable nature of styrene. Overall, the working principle focuses on maintaining a controlled environment, ensuring the material is transported safely and efficiently from storage to processing units.
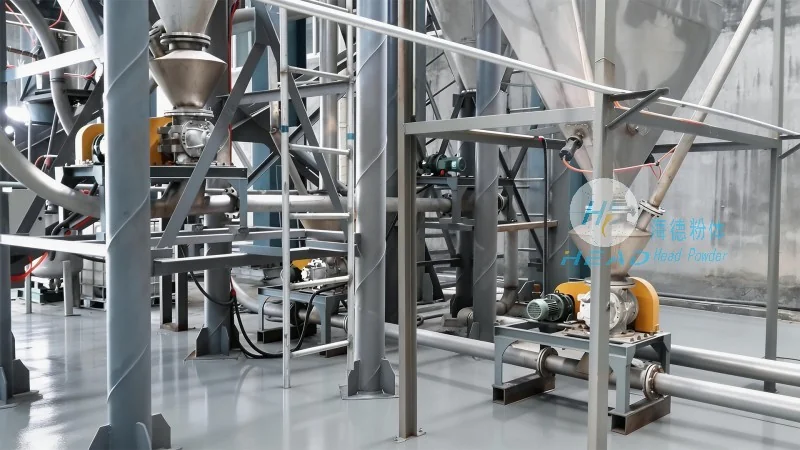
Key Features of Styrene Material Handling Equipment
Styrene material handling equipment from Shandong HeadPowder Engineering Co., Ltd. is characterized by several key features that enhance performance, safety, and reliability. One of the primary features is the use of advanced materials for construction, such as stainless steel and specialized alloys, which provide excellent resistance to corrosion and chemical degradation. The equipment is also designed with safety in mind, incorporating features like explosion-proof motors, fire-resistant coatings, and automatic shut-off systems to prevent accidents. Another important feature is the integration of automation and control systems, which allow for precise monitoring and adjustment of the transport process. This includes real-time data on flow rates, pressure, and temperature, enabling operators to make informed decisions and maintain optimal conditions. The systems are also engineered for durability and low maintenance, with modular components that can be easily replaced or repaired, reducing downtime and operational costs. Furthermore, the equipment is compliant with international safety standards, ensuring that it meets the regulatory requirements for handling hazardous materials like styrene. These features collectively contribute to the effectiveness and reliability of styrene material handling systems, making them essential for industrial applications.
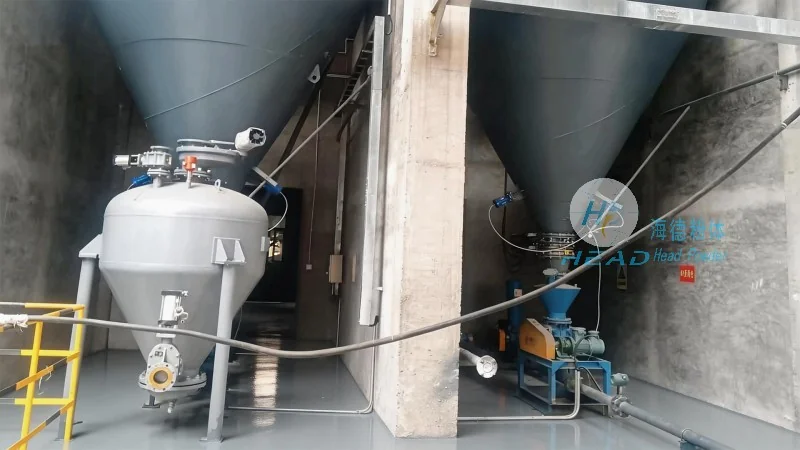
Applications and Benefits
The applications of styrene material handling systems are widespread across various industries, including the petrochemical, polymer manufacturing, and chemical processing sectors. In these industries, the equipment is used to transport styrene from storage facilities to reactors, where it is polymerized into polystyrene and other products. The benefits of using advanced material handling systems include improved safety, reduced operational risks, and enhanced efficiency. By ensuring the safe and efficient transport of styrene, these systems minimize the potential for accidents, such as leaks or fires, which can cause significant damage to equipment and the environment. Additionally, the precise control over flow rates and pressure helps maintain consistent product quality, leading to higher yields and better performance in downstream processes. The durability and low maintenance requirements of the equipment also contribute to long-term cost savings, as they require less frequent repairs and replacements. Overall, the use of specialized styrene material handling systems from HeadPowder provides significant advantages in terms of safety, efficiency, and cost-effectiveness for industrial operations.
Conclusion
In conclusion, the working principle and features of styrene material handling systems are critical for ensuring the safe and efficient transport of this vital monomer in industrial applications. Shandong HeadPowder Engineering Co., Ltd. has demonstrated expertise in designing and manufacturing high-quality equipment that meets the stringent requirements of the industry. By incorporating advanced materials, safety features, and automation, the company's systems provide reliable performance and contribute to the overall success of industrial processes. As the demand for polystyrene and other styrene-based products continues to grow, the importance of efficient material handling systems will only increase, making HeadPowder's solutions a valuable asset for businesses in the chemical and polymer sectors.




