Working Principle and Features of the Rice Husk Ash Material Conveying System Equipment
Release time:2026-09-18 00:01:33
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For industries dealing with rice husk ash, efficient material handling is crucial for operational efficiency and safety. The rice husk ash material conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., offers a reliable solution tailored to the unique challenges of handling this specific material. This article explores the working principle and key features of this system, providing insights into how it enhances productivity and operational stability.
Working Principle of the Rice Husk Ash Material Conveying System
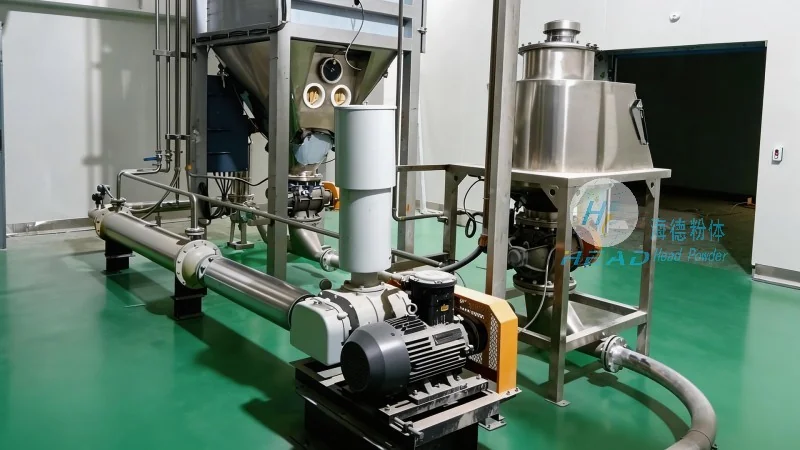
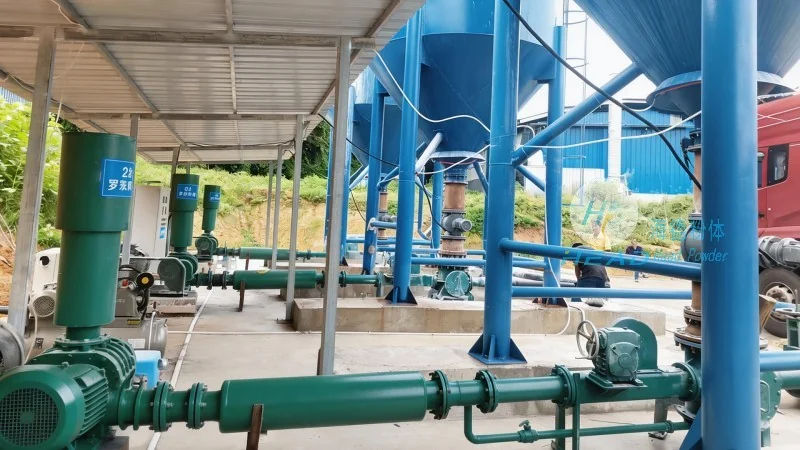
The rice husk ash material conveying system operates on a combination of mechanical and pneumatic principles, designed to handle the abrasive and lightweight nature of rice husk ash. The system typically includes a series of components such as feed hoppers, conveyor belts or screw conveyors, and dust collection units. The feed hopper collects the raw rice husk ash and feeds it into the primary conveyor mechanism. Depending on the system design, a screw conveyor or a belt conveyor may be used to transport the material horizontally or vertically. The conveying process is driven by electric motors, which ensure consistent and adjustable speed control. To manage dust and maintain air quality, the system incorporates advanced dust filtration and collection systems. These components work in tandem to ensure that the material is transported efficiently while minimizing environmental impact and health risks associated with airborne particles.
Key Features of the Rice Husk Ash Material Conveying System
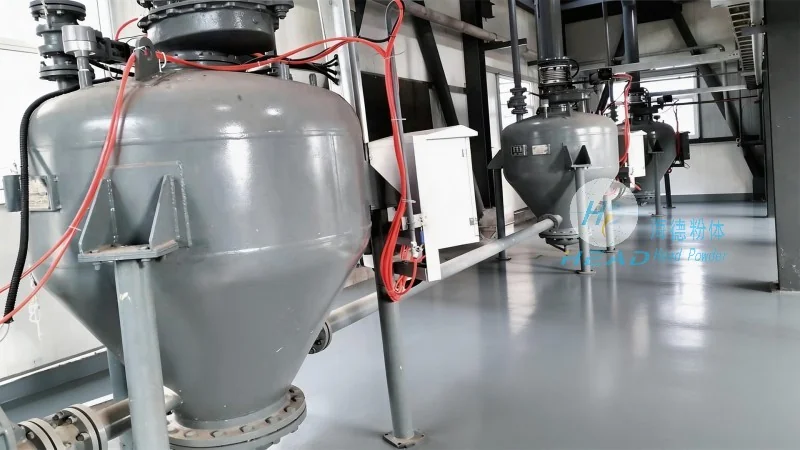
Shandong HeadPowder Engineering Co., Ltd. has integrated several advanced features into the rice husk ash material conveying system to enhance its performance and user experience. One of the standout features is the adjustable speed control, which allows operators to modify the conveying rate based on the material flow and processing requirements. This flexibility is particularly beneficial in dynamic production environments where material volumes may vary. The system also includes robust material handling components, such as heavy-duty belts or screws, which are designed to withstand the abrasive properties of rice husk ash, reducing wear and tear and extending the equipment's lifespan. Additionally, the dust control mechanisms are engineered to meet stringent environmental standards, ensuring compliance with local regulations while protecting the health of workers. The system's modular design facilitates easy maintenance and component replacement, minimizing downtime and operational costs. Furthermore, the integration of sensors and monitoring systems provides real-time data on the system's performance, enabling proactive maintenance and optimizing operational efficiency.
Benefits and Applications
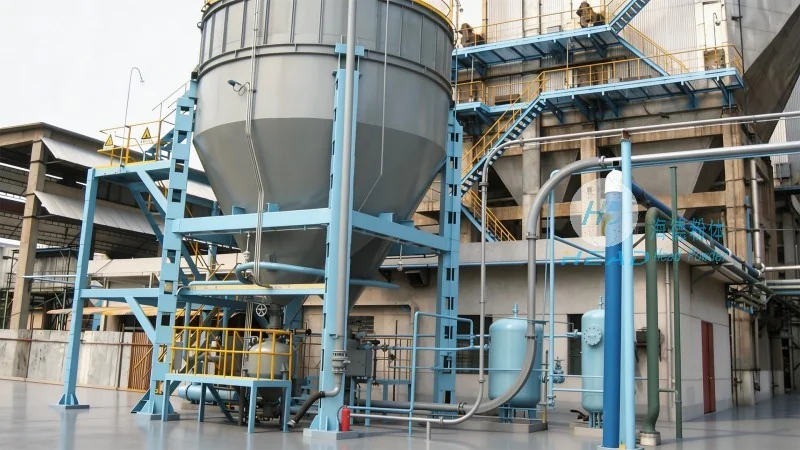
The rice husk ash material conveying system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits for industries that process rice husk ash, including power plants, biomass energy facilities, and agricultural processing plants. The system's efficiency in material handling reduces labor costs and improves overall production throughput. The advanced dust control features enhance workplace safety and environmental sustainability, aligning with modern industrial standards. The system's adaptability allows it to be customized for various applications, from small-scale processing to large-scale industrial operations. By leveraging the expertise of Shandong HeadPowder Engineering Co., Ltd., users can achieve reliable and cost-effective material handling solutions that meet their specific operational needs.




