Positive pressure dense phase powder pneumatic conveying systems are advanced industrial equipment designed to transport bulk powders efficiently and reliably. This technology has become increasingly important in various industries, including chemical, food, pharmaceutical, and mining, due to its ability to handle a wide range of powder characteristics while minimizing material degradation and system wear. Understanding the working principle and key features of such systems is crucial for selecting the right equipment for specific applications.
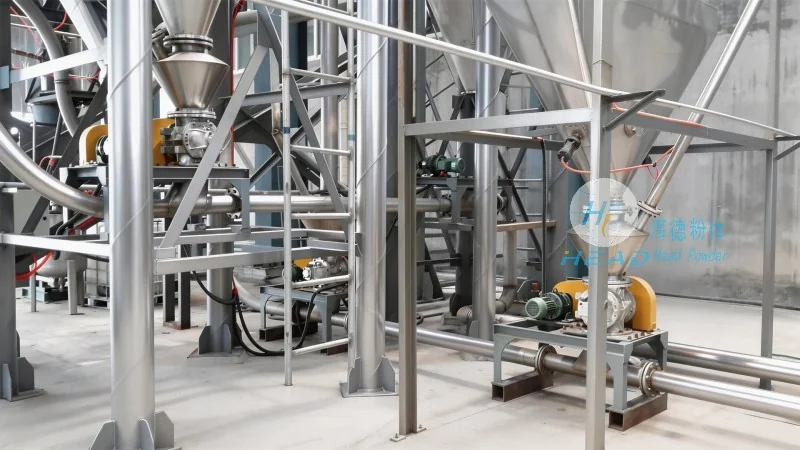
Working Principle of Positive Pressure Dense Phase Powder Pneumatic Conveying Equipment
The core of a positive pressure dense phase powder pneumatic conveying system lies in its ability to transport powders in a dense, slurry-like state rather than as individual particles suspended in air. This is achieved by maintaining a high pressure within the conveying line, typically ranging from 0.5 to 2.0 bar above atmospheric pressure. The system operates by injecting air or gas into the material at the inlet, creating a high-pressure environment that forces the powder to move through the pipeline. The dense phase ensures that the powder particles are closely packed, reducing the risk of segregation and improving the overall conveying efficiency.
At the source, the powder is fed into a hopper or feeder, which controls the flow rate. The feeder then delivers the powder into a pressure vessel or a high-pressure pump, where it is mixed with the conveying medium (usually air or nitrogen). The mixture is then pressurized and sent through the pipeline to the discharge point. The pressure differential between the inlet and outlet drives the material forward, and the system is designed to maintain a consistent pressure throughout the conveying line to ensure smooth operation.
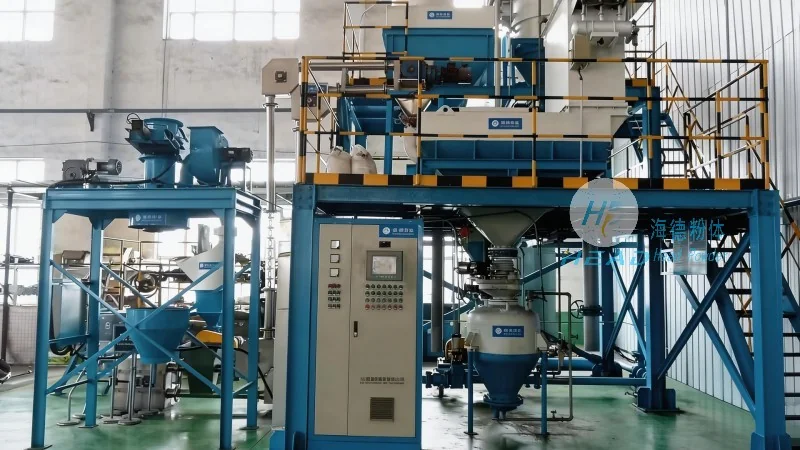
Key Features and Advantages of Positive Pressure Dense Phase Powder Pneumatic Conveying Systems
Positive pressure dense phase powder pneumatic conveying systems offer several distinct advantages over traditional pneumatic conveying methods. One of the most significant benefits is the ability to handle abrasive and corrosive powders without causing excessive wear on the system components. The dense phase operation reduces the impact of individual particles on the pipeline walls, extending the service life of the equipment.
Another key feature is the high conveying capacity. These systems can transport large volumes of powder at a relatively low air velocity, which minimizes energy consumption compared to dilute phase systems. This efficiency is particularly important for long-distance or high-volume applications, where energy costs can be a major factor.
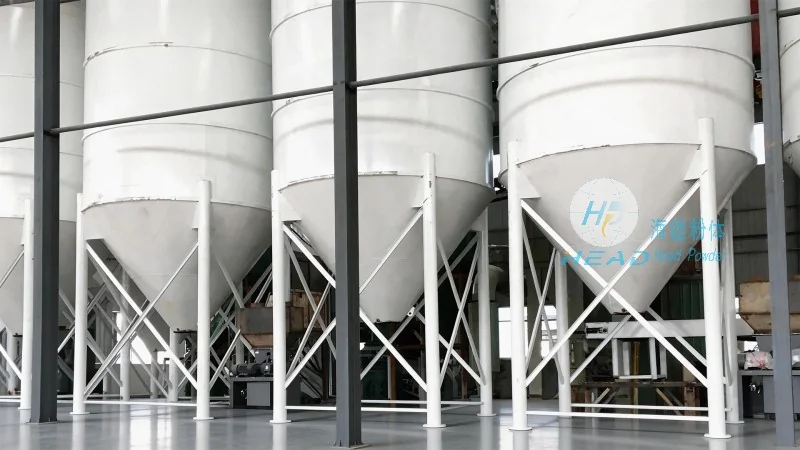
Furthermore, the positive pressure design ensures that the conveying line is always under pressure, preventing the ingress of contaminants such as dust or moisture. This is critical in industries where product purity is paramount, such as pharmaceuticals or food processing. The system also allows for easy integration with other processing equipment, as the discharge can be controlled and directed to specific locations without the need for additional handling steps.
Applications and Industries Utilizing Positive Pressure Dense Phase Powder Pneumatic Conveying Systems
Due to their versatility and efficiency, positive pressure dense phase powder pneumatic conveying systems are widely used across various industries. In the chemical industry, they are employed to transport raw materials and finished products, such as powders used in the production of fertilizers, paints, and plastics. The pharmaceutical industry benefits from the system's ability to maintain sterile conditions and prevent cross-contamination, making it suitable for transporting active pharmaceutical ingredients (APIs) and other sensitive materials.
In the food and beverage sector, these systems are used to convey ingredients like flour, sugar, and spices while preserving the quality and freshness of the products. The low air velocity and gentle handling of the dense phase operation prevent product degradation, ensuring that the final product meets quality standards. The mining industry also utilizes positive pressure dense phase systems to transport bulk materials such as coal, ore, and minerals from storage facilities to processing plants.
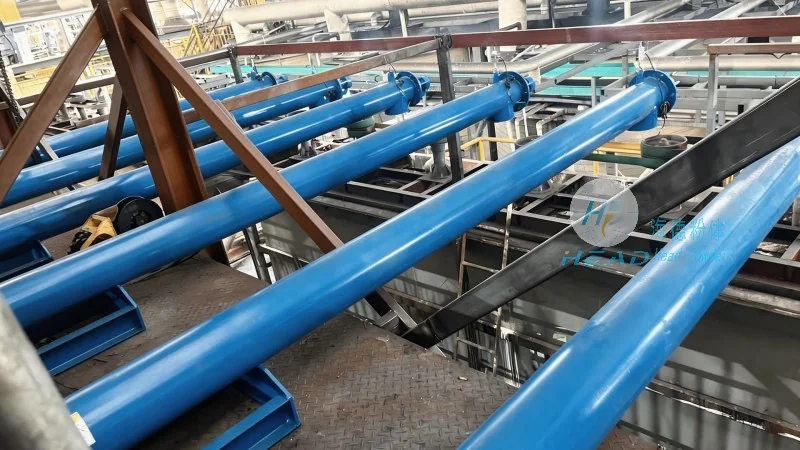
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of industrial conveying equipment, specializes in the design, development, and production of positive pressure dense phase powder pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's products are engineered to meet the specific needs of various industries, ensuring optimal performance and durability.
HeadPowder is headquartered in Shandong, China, and serves clients globally with a focus on providing customized solutions tailored to individual application requirements. The company's team of experienced engineers and technicians work closely with customers to understand their operational challenges and develop tailored conveying systems that enhance productivity and reduce operational costs.




