HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced air-powered conveyors tailored for transporting bulk materials such as coal gangue, limestone, and other similar powders and granules. This article explores the fundamental working principles and key features of these efficient conveying systems, highlighting how they enhance material handling processes in industrial applications.
Understanding the Working Principle of Air-Powered Conveyors
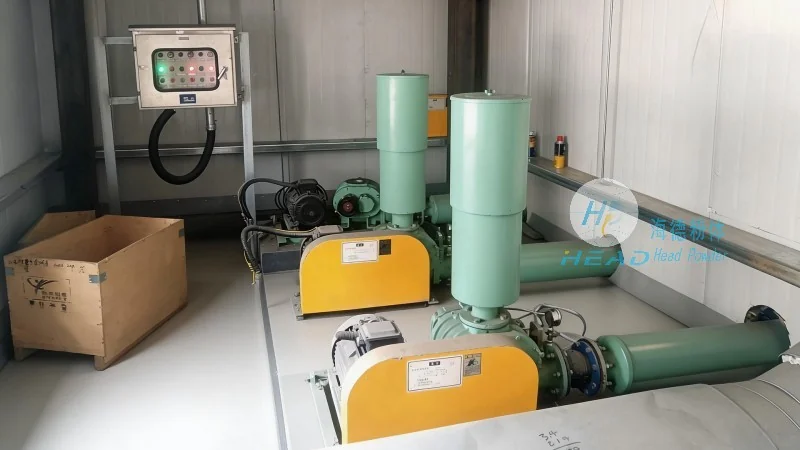
The core mechanism of an air-powered conveyor, also known as a pneumatic conveyor, relies on the movement of air to transport bulk materials. These systems typically operate by creating a pressure differential between the inlet and outlet, which propels the material through a pipeline. The process begins with the material being fed into the inlet hopper, where it is then drawn into the conveyor by a vacuum or pressure source. As the air flows through the pipeline, it carries the material particles along, ensuring a continuous and controlled flow. The design of the conveyor, including the type of air flow (positive or negative pressure) and the configuration of the pipeline, is crucial in determining the efficiency and suitability for specific materials.
For materials like coal gangue and limestone, which are often abrasive and have varying particle sizes, the air-powered conveyor's ability to handle such characteristics is particularly important. The system's design incorporates features such as flexible hoses or rigid pipes, depending on the application requirements. The air flow is managed by a blower or vacuum pump, which adjusts the pressure to maintain optimal material transport. This mechanism ensures that the material is conveyed without excessive friction or blockage, reducing wear and tear on the equipment and extending its operational lifespan.
Key Features of Air-Powered Conveyors for Bulk Materials
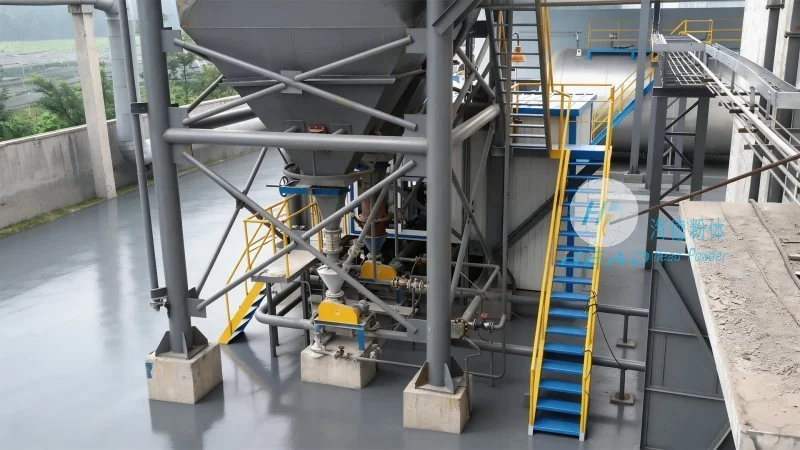
HeadPowder's air-powered conveyors for coal gangue and limestone are equipped with several distinctive features that enhance their performance and reliability. One of the primary advantages is the ability to transport materials over long distances with minimal energy consumption. Unlike traditional mechanical conveyors, which require moving parts and continuous power for operation, pneumatic systems use compressed air, which can be more energy-efficient for certain applications. This makes them suitable for industries where cost-effectiveness and energy savings are critical factors.
Another notable feature is the system's versatility in handling diverse material types. Whether dealing with fine powders, coarse granules, or mixed materials, the air-powered conveyor can adapt to varying particle sizes and densities. The design allows for easy integration with other processing equipment, such as crushers, screens, and storage silos, creating a seamless material handling workflow. This adaptability is essential in industrial settings where materials may need to be transferred between different stages of production.
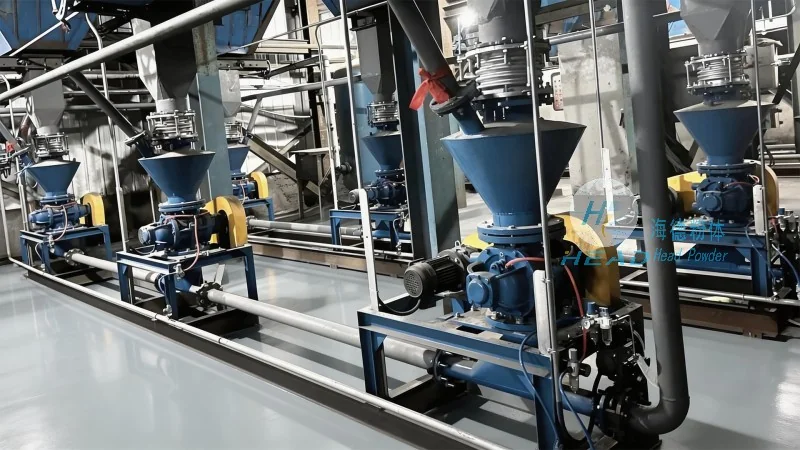
The construction of these conveyors also emphasizes durability and low maintenance. The use of high-quality materials, such as stainless steel or corrosion-resistant alloys, ensures that the equipment can withstand the harsh conditions associated with coal gangue and limestone processing. The absence of moving parts in the conveying line reduces the risk of mechanical failure and simplifies maintenance procedures. This results in lower operational costs and increased uptime for the system.
Applications and Benefits in Industrial Settings
HeadPowder's air-powered conveyors are widely used in various industrial applications, including mining, construction, and chemical processing. In mining operations, they are essential for transporting coal gangue from extraction sites to processing facilities, ensuring a smooth and efficient supply chain. The ability to handle large volumes of material with minimal human intervention makes these systems highly effective in reducing labor costs and improving operational efficiency.
In the construction industry, limestone is often used as a raw material for cement production. The air-powered conveyor facilitates the transport of limestone from quarries to processing plants, where it is further processed into cement. The system's ability to handle abrasive materials without significant wear and tear is particularly beneficial in this context, as it reduces equipment maintenance and extends the lifespan of the machinery.
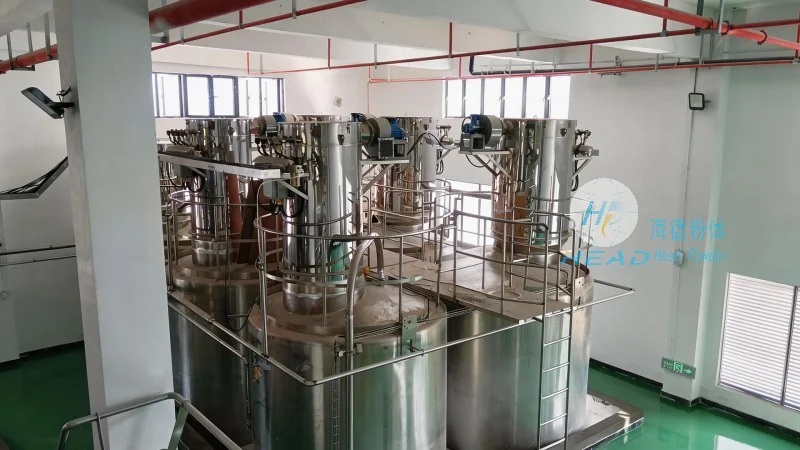
Furthermore, the chemical processing industry benefits from the versatility of these conveyors when handling various powders and granules. The controlled and dust-free operation of the system minimizes the risk of material contamination and ensures product quality. This is crucial in industries where purity and consistency are paramount, such as pharmaceuticals or food processing.
Conclusion
HeadPowder's air-powered conveyors for coal gangue, limestone, and similar bulk materials offer a reliable and efficient solution for industrial material handling. By leveraging the principles of pneumatic transport, these systems provide a cost-effective and low-maintenance option for moving large volumes of material over extended distances. The key features, including energy efficiency, versatility, and durability, make them an ideal choice for various industrial applications. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate and provide advanced solutions that meet the evolving needs of the industry.




