Sucrose powder conveying lines are critical equipment in modern food processing industries, designed to efficiently and safely transport granular sucrose powders. These systems integrate advanced mechanical design and control technologies to maintain the quality and stability of the powder during transport while meeting the demands of various production scenarios. By ensuring seamless and reliable movement of sucrose from storage to processing or packaging areas, these lines play a vital role in optimizing production workflows.
Principles of Sucrose Powder Conveying Lines
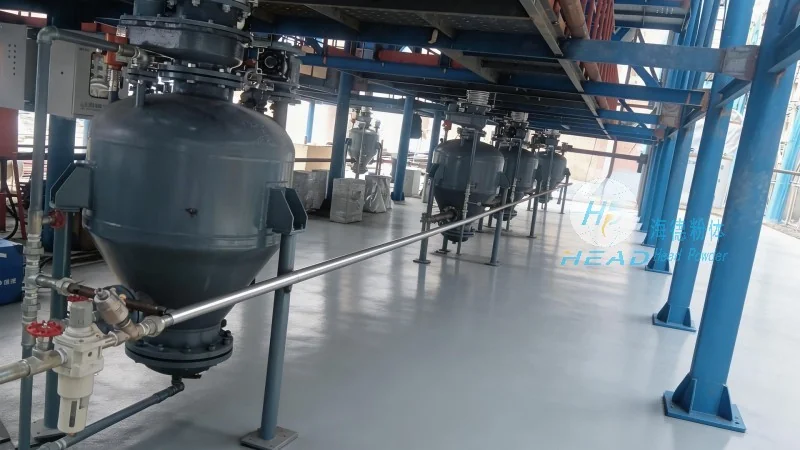
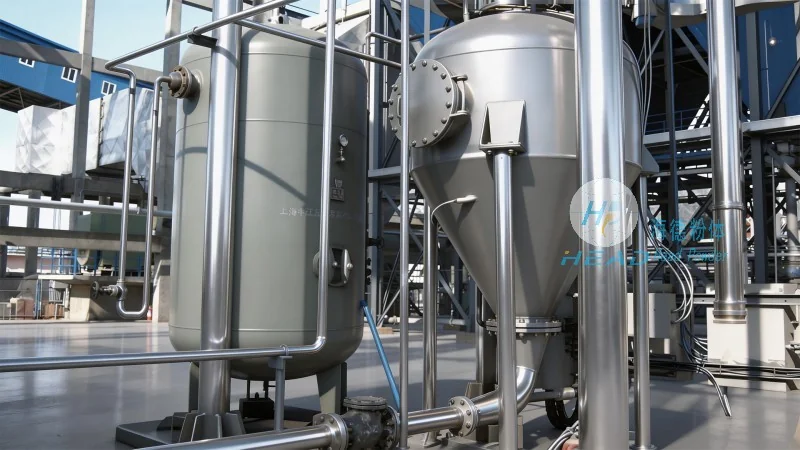
The core principles of sucrose powder conveying lines are rooted in fluid dynamics and particle transport technology. The system typically comprises several key components: a hopper for collecting and storing sucrose powder, conveying pipes to transport the powder to the target location, a driving device (such as a screw conveyor, pneumatic conveyor, or vibratory conveyor) to provide the necessary force for movement, and a control system to monitor and regulate parameters like speed and pressure. The hopper ensures a consistent supply of powder, while the conveying pipes maintain the integrity of the material. The driving device, whether mechanical or pneumatic, facilitates the movement of sucrose particles through the system. The control system plays a crucial role in maintaining operational stability, preventing issues like blockages or uneven flow. For instance, screw conveyors use rotating helical blades to push the powder along the pipe, whereas pneumatic conveyors utilize compressed air to blow the powder through the system. These technologies work in concert to achieve continuous, leak-free transport of sucrose powder, ensuring minimal degradation or contamination.
Key Working Scene Characteristics
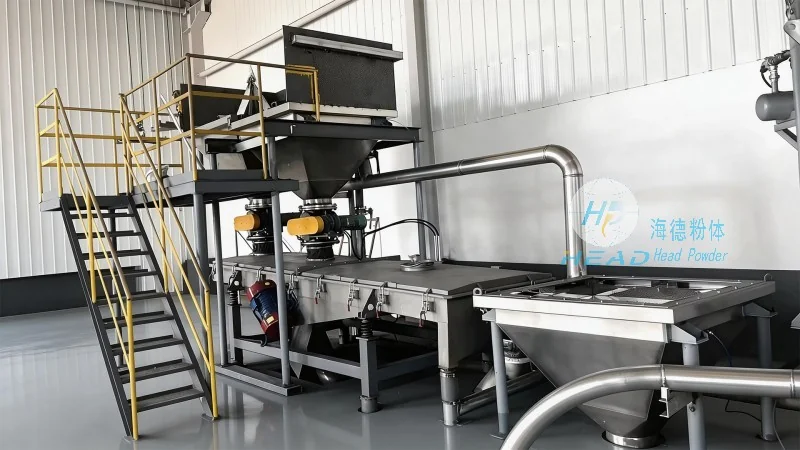
The working scene characteristics of sucrose powder conveying lines are diverse and adaptable, tailored to the specific needs of food processing environments. Common applications include sugar factories, candy manufacturing plants, and beverage production facilities. In these settings, the conveying lines must handle high-purity sucrose powders, ensuring that the material remains free from clumping or contamination during transport. For example, in a sugar factory, the line may transport raw sucrose from storage silos to the processing line, while in a candy factory, it delivers refined sucrose to mixing equipment or packaging lines. Additionally, the working scenarios often involve environmental considerations such as temperature control and humidity management to preserve the physical and chemical properties of the sucrose. The systems are typically modular, allowing for customization based on production scale and process requirements, ensuring flexibility and efficiency across different operational contexts.
About Shandong HeadPowder Engineering Co., Ltd.
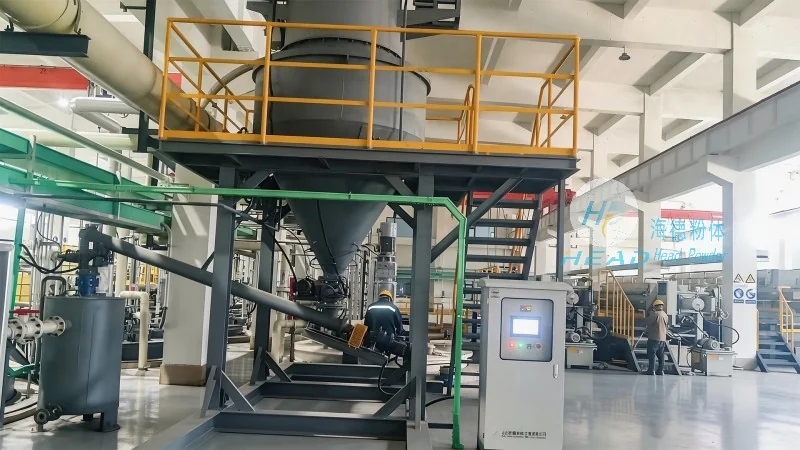
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a professional company based in Shandong, China, specializing in the research, development, manufacturing, and service of powder conveying equipment. Since its establishment, the company has focused on innovation and optimization of sucrose powder conveying systems and other food processing machinery. With extensive industry experience and advanced technical capabilities, headpowder has built a strong reputation for delivering high-quality, reliable solutions. The company’s headquarters is located in Shandong, China, and it is committed to providing efficient and dependable sucrose powder conveying solutions to help food processing enterprises enhance their production efficiency and product quality.




