Intelligent weighing powder conveying machines represent a sophisticated technological solution designed to enhance the efficiency and precision of powder handling processes across various industrial sectors. These systems integrate advanced weighing technology with automated material transport mechanisms, enabling real-time monitoring and control of powder flow, which is crucial for applications where accuracy and consistency are paramount.
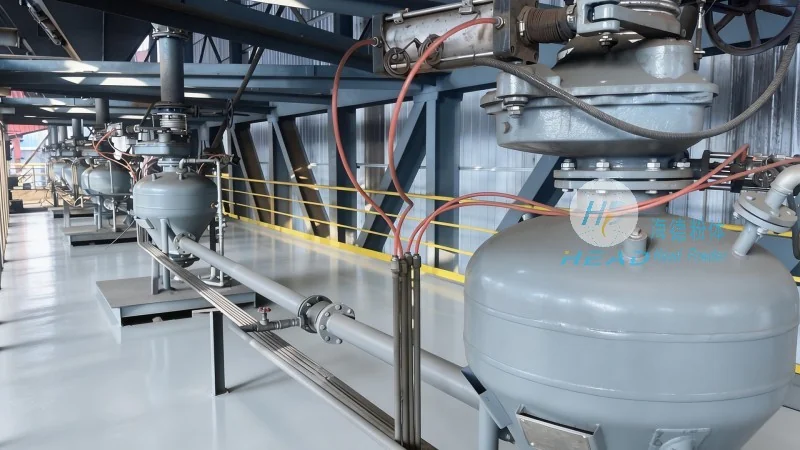
Core Principles of Intelligent Weighing Powder Conveying Systems
The fundamental principle of these machines lies in the integration of high-precision load cells and digital control systems. The load cells are strategically positioned to measure the weight of the powder as it is conveyed, providing immediate feedback to the control unit. This data is processed in real-time, allowing the system to adjust the conveying speed or flow rate to maintain a consistent weight output. The control system typically operates on a closed-loop feedback mechanism, ensuring that deviations from the set weight are corrected dynamically, thereby minimizing material waste and improving overall process reliability.
A key component in the operation of intelligent weighing powder conveying machines is the use of variable frequency drives (VFDs) for motor control. VFDs allow for precise adjustment of the conveyor speed, which directly impacts the powder flow rate. By coupling this with the weight measurement data, the system can achieve a high degree of control over the material being transported. Additionally, many modern systems incorporate sensors such as level detectors or flow meters to provide supplementary data, enhancing the overall monitoring capabilities and ensuring comprehensive process visibility.
Working Scene Characteristics and Application Environments
The working scene characteristics of intelligent weighing powder conveying machines are tailored to meet the diverse demands of industrial applications. These systems are commonly employed in sectors like chemical manufacturing, pharmaceutical production, food processing, and cement production, where the handling of bulk powders requires strict adherence to quality and safety standards. The design of these machines is optimized for environments that may involve dusty or potentially hazardous conditions, with features such as dust-proof enclosures and explosion-proof components to ensure operational safety.
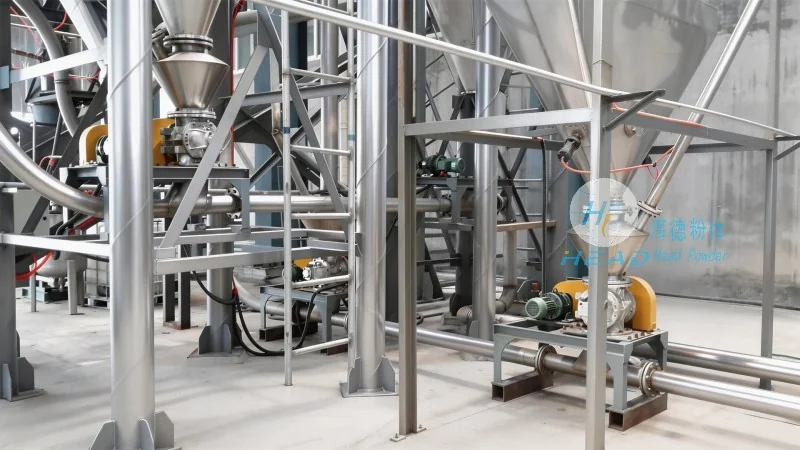
In chemical and pharmaceutical industries, for instance, the precision of weighing is critical to maintaining the correct formulation of products. The intelligent conveying systems help in achieving consistent dosing, which is essential for product quality and regulatory compliance. Similarly, in food processing, where hygiene and contamination control are paramount, these machines are equipped with stainless steel construction and easy-to-clean surfaces, ensuring that the handling of powders meets stringent sanitary standards.
The working scene also includes scenarios where space constraints are a factor. Compact designs and modular configurations allow for installation in existing production lines without significant modifications. Furthermore, the systems are designed to be scalable, enabling businesses to expand their operations by adding additional conveying lines or upgrading to higher capacity models as needed. This flexibility makes intelligent weighing powder conveying machines suitable for both small-scale and large-scale production environments.
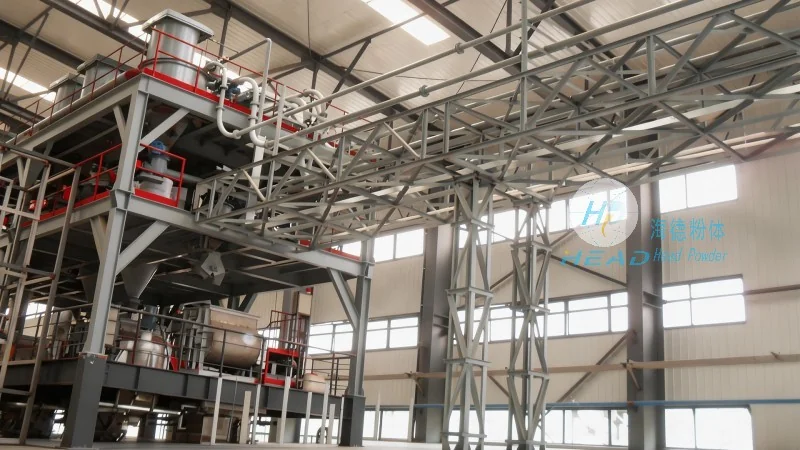
Company Background and Technical Expertise
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and production of advanced powder handling equipment. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted provider of intelligent weighing powder conveying systems. HeadPowder's engineering team leverages years of industry experience to develop products that address the specific challenges faced by clients in various sectors.
HeadPowder's facilities are located in Shandong, China, where the company operates state-of-the-art manufacturing and testing centers. This infrastructure enables the company to ensure the quality and reliability of its products through rigorous testing and quality control processes. The company's commitment to technological advancement is reflected in its continuous investment in research and development, which has led to the integration of cutting-edge features such as IoT connectivity, remote monitoring, and data analytics into its conveying systems.
By combining advanced technology with practical application expertise, HeadPowder aims to deliver solutions that not only meet but exceed the expectations of its clients. The company's products are designed to enhance operational efficiency, reduce downtime, and improve overall productivity, contributing to the long-term success of its customers' businesses. With a strong presence in the domestic and international markets, HeadPowder continues to be a key player in the powder handling equipment industry.




