The intelligent tonne bag loading station powder conveying machine is a specialized piece of equipment designed for efficient handling and transportation of bulk powders from tonne bags. As a key component in industrial material processing, this system integrates advanced automation and control technologies to ensure precise and reliable powder transfer. The machine is engineered to meet the demands of various industrial applications, providing a solution that enhances productivity and operational safety.
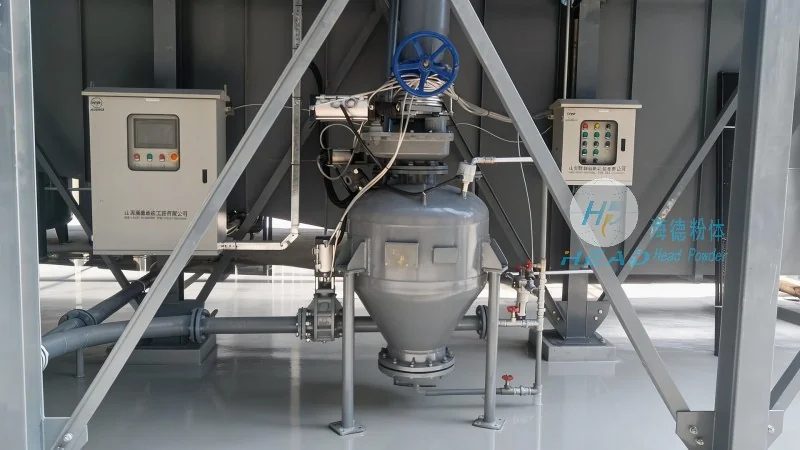
Key Features and Technical Specifications
HeadPowder, a leading manufacturer in the field, has developed this intelligent system with a focus on durability, efficiency, and user-friendly operation. The equipment typically includes a hopper for receiving powder from tonne bags, a feeding mechanism to control the flow rate, and a conveying system such as screw conveyors or pneumatic pipelines. The machine is equipped with sensors and control panels that allow for real-time monitoring and adjustment of the conveying process. This ensures consistent material handling and minimizes the risk of material loss or contamination.
Working Principle of the Powder Conveying Machine
The core principle of the intelligent tonne bag loading station powder conveying machine involves the sequential steps of bag opening, material discharge, and subsequent transport. The process begins with the placement of a tonne bag onto the loading platform. The machine then uses an automated system to open the bag and allow the powder to flow into the hopper. The feeding mechanism, often a variable-speed screw or a rotary valve, regulates the flow of powder from the hopper into the conveying system. The conveying system then transports the powder to the desired destination, such as a silo, storage tank, or processing unit. The entire operation is controlled by a programmable logic controller (PLC) that coordinates the actions of all components, ensuring smooth and continuous operation.
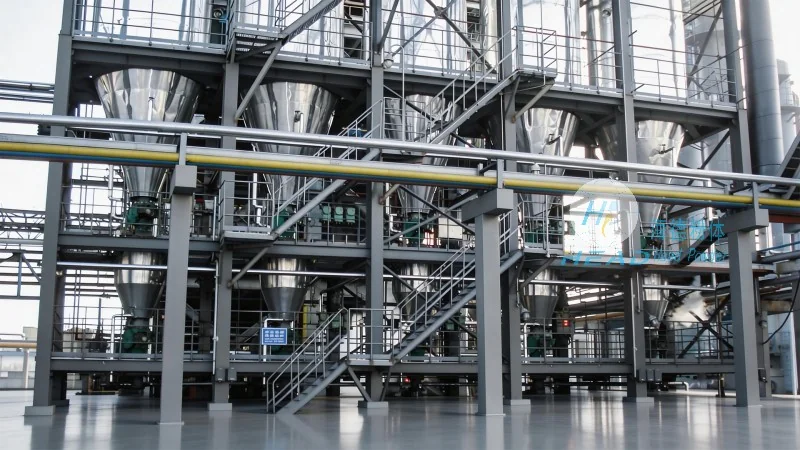
Working Scene Characteristics and Applications
The intelligent tonne bag loading station powder conveying machine is widely used in various industrial sectors, including chemical, pharmaceutical, food, and mining industries. Its design allows for the handling of a wide range of powders, from fine to coarse particles, with different moisture contents and flow properties. The machine is particularly suitable for applications where large quantities of bulk materials need to be transferred efficiently and safely. In chemical plants, for example, it is used to transport raw materials to reactors, while in food processing facilities, it handles ingredients like flour and sugar. The system's ability to maintain a clean and controlled environment is crucial in industries where product purity and hygiene are paramount.
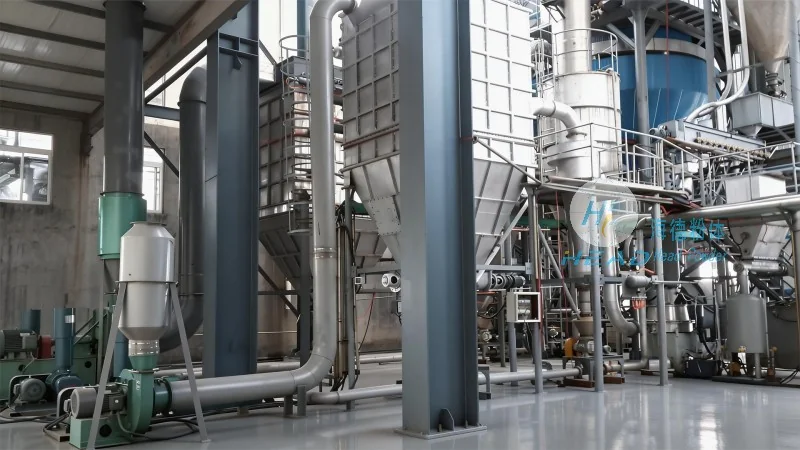
Advantages of the Intelligent System
Compared to traditional manual or semi-automatic systems, the intelligent tonne bag loading station powder conveying machine offers several advantages. Firstly, it significantly reduces labor costs and human error, as the entire process is automated. Secondly, it enhances operational efficiency by ensuring consistent flow rates and minimizing downtime. Thirdly, the system improves safety by eliminating the need for manual handling of heavy tonne bags and reducing the risk of dust exposure. Additionally, the machine can be integrated with other industrial systems, such as inventory management software, to provide a comprehensive solution for material handling. The durability and low maintenance requirements of the equipment also contribute to long-term cost savings for the end-user.
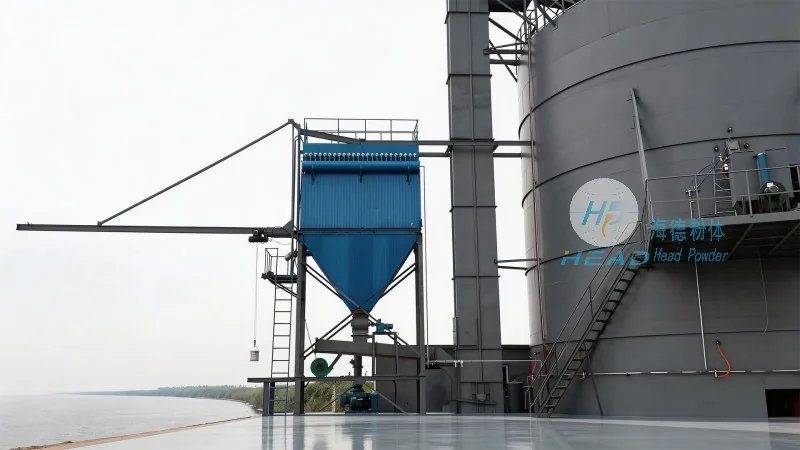
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a subsidiary of Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of bulk material handling equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's products are designed to meet the specific needs of different industries, offering customized solutions that enhance operational performance. The company's headquarters is located in Shandong, China, where it has a team of experienced engineers and technicians dedicated to research and development. HeadPowder adheres to international standards and continuously invests in advanced technologies to improve its product line and provide superior customer service.
Conclusion
The intelligent tonne bag loading station powder conveying machine represents a significant advancement in bulk material handling technology. By combining automation, precision control, and robust design, this system offers an efficient and reliable solution for industries that require the safe and effective transfer of powders. With its wide range of applications and numerous benefits, the machine is an essential component for modern industrial operations. HeadPowder's expertise in this field ensures that customers receive high-quality equipment that meets their specific requirements and contributes to their overall success.




