HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design and manufacturing of advanced cotton seed powder conveying systems. These systems are engineered to efficiently transport cotton seed powders, ensuring optimal performance in various industrial applications. This article explores the fundamental principles behind these systems and highlights the key characteristics that define their operational effectiveness in real-world scenarios.
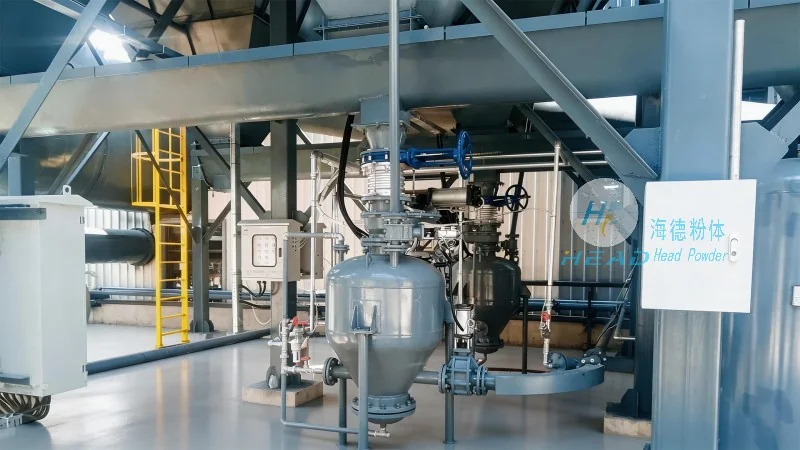
Understanding the Core Principles of Cotton Seed Powder Conveying Systems
The cotton seed powder conveying system operates on the principle of mechanical transport, utilizing a combination of components such as hoppers, conveyors, and control mechanisms to move bulk powders. The system is designed to handle the unique properties of cotton seed powders, including their fine particle size and potential for static electricity. By integrating features like vibration feeders and air seals, the equipment ensures consistent flow and prevents material degradation during transit. The control system, often equipped with sensors and automation, monitors parameters like flow rate and pressure, allowing for real-time adjustments to maintain optimal performance.
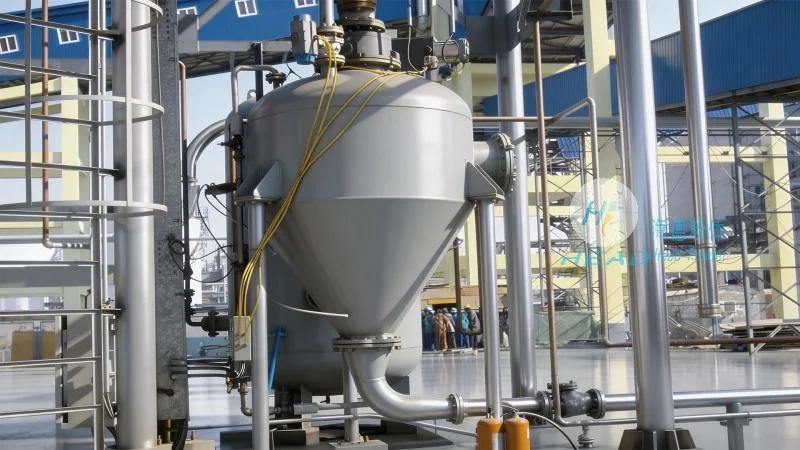
Key Working Scene Characteristics of Cotton Seed Powder Conveying Systems
The operational characteristics of cotton seed powder conveying systems are tailored to meet the demands of specific industrial environments. In cotton seed processing facilities, these systems are commonly used in stages such as raw material handling, storage, and transfer to processing units. The systems are designed to operate in environments with varying temperatures and humidity levels, ensuring reliability even under challenging conditions. One notable characteristic is their ability to handle high volumes of material with minimal downtime, which is crucial for maintaining production efficiency in large-scale operations. Additionally, the systems are constructed with materials that resist corrosion and wear, extending their service life and reducing maintenance costs.
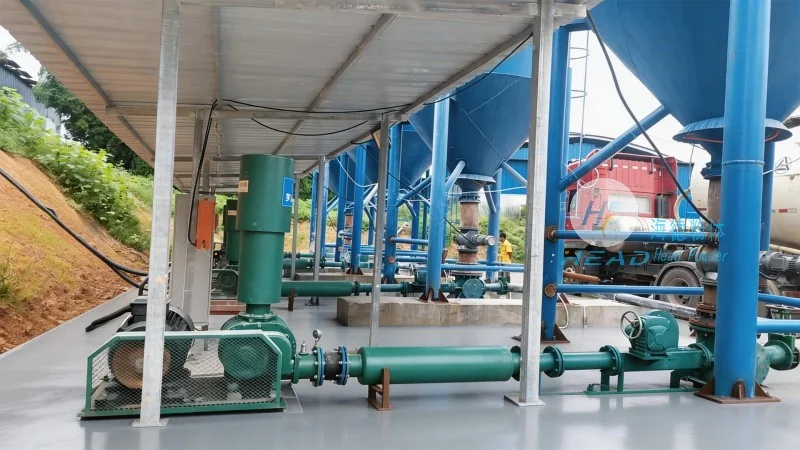
Application Scenarios and Operational Advantages
In industrial settings, cotton seed powder conveying systems are deployed in diverse scenarios, from small-scale processing plants to large-scale agricultural processing facilities. The systems are particularly effective in environments where precise control over material flow is essential, such as in the preparation of feed or oil extraction processes. The advantages of these systems include improved safety through reduced manual handling of powders, enhanced product quality by minimizing contamination, and increased operational efficiency through automated control. Furthermore, the modular design of the systems allows for easy integration with existing production lines, making them a versatile solution for various industrial needs.
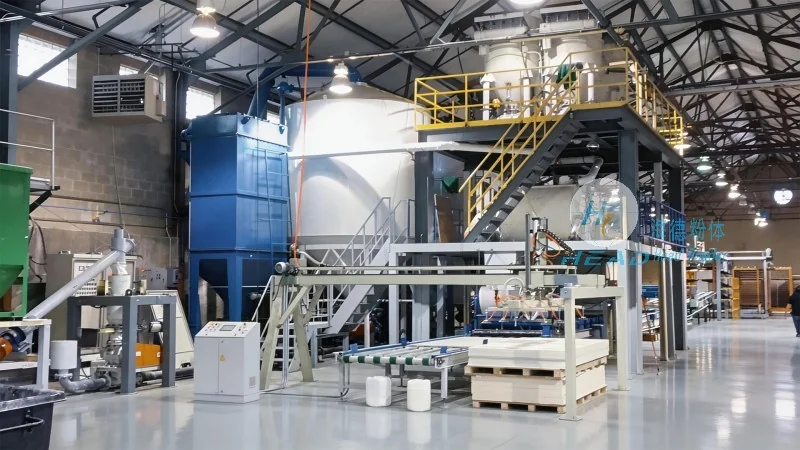
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable manufacturer specializing in the development of advanced powder handling equipment. With years of experience in the industry, the company has established itself as a trusted partner for businesses seeking reliable and efficient solutions for their material transport needs. HeadPowder's commitment to innovation and quality ensures that their products meet the highest standards of performance and durability, catering to the diverse requirements of global markets.




