Working Principle and Features of Fertilizer Material Handling System Equipment
Release time:2026-09-17 23:01:22
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Efficient and reliable fertilizer material handling systems are crucial for modern agricultural operations. These systems ensure the safe and efficient transport of bulk fertilizers from storage to application points, enhancing productivity and minimizing operational risks. Understanding the working principles and key features of such equipment is essential for selecting the right solution for specific agricultural needs.
Working Principle of Fertilizer Material Handling Systems
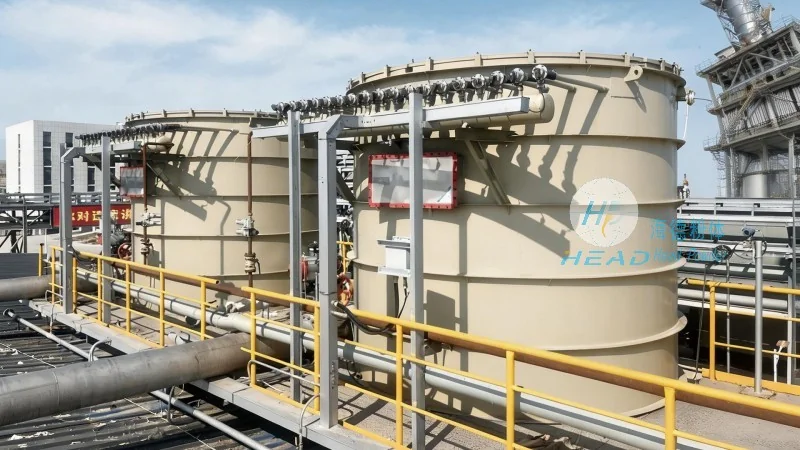
The core working principle of fertilizer material handling systems revolves around the use of specialized machinery to move bulk materials. These systems typically include components like feeders, conveyors, and storage silos. The process begins with the storage of raw fertilizer in silos, where it is then fed into a conveyor system. The conveyor, often equipped with augers or belt mechanisms, transports the fertilizer to the desired location. For vertical transport, elevators or bucket elevators are used to lift the material to higher levels. The system ensures consistent flow and minimal material degradation, maintaining the quality of the fertilizer throughout the handling process.
Key Features of Fertilizer Material Handling Equipment
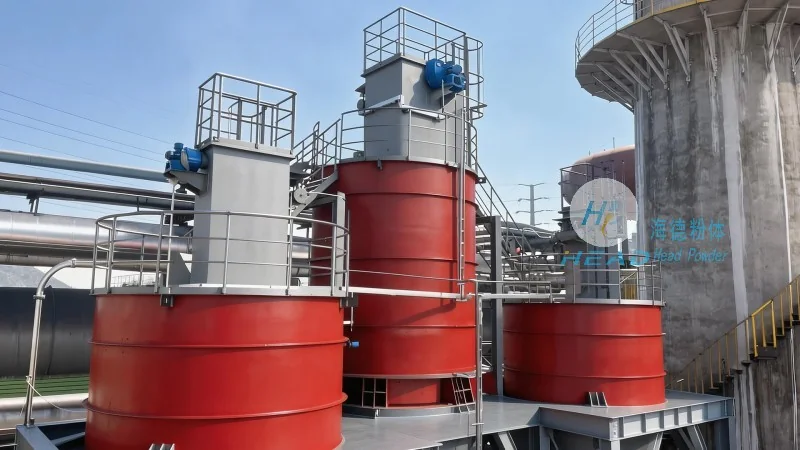
Modern fertilizer material handling systems are designed with several key features that enhance performance and reliability. One of the primary features is the ability to handle various types of fertilizers, including granular, powdered, and liquid forms. The equipment is constructed with durable materials, such as stainless steel or corrosion-resistant alloys, to withstand the chemical properties of fertilizers and prevent contamination. Another important feature is the integration of advanced control systems, which allow for precise control of flow rates and operational parameters. This ensures optimal performance and reduces the risk of overloading or underflow. Additionally, the systems are equipped with safety features, such as overload protection and emergency stop mechanisms, to protect both the equipment and personnel. The design also emphasizes energy efficiency, with variable speed drives and optimized conveyor designs reducing power consumption while maintaining high throughput.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
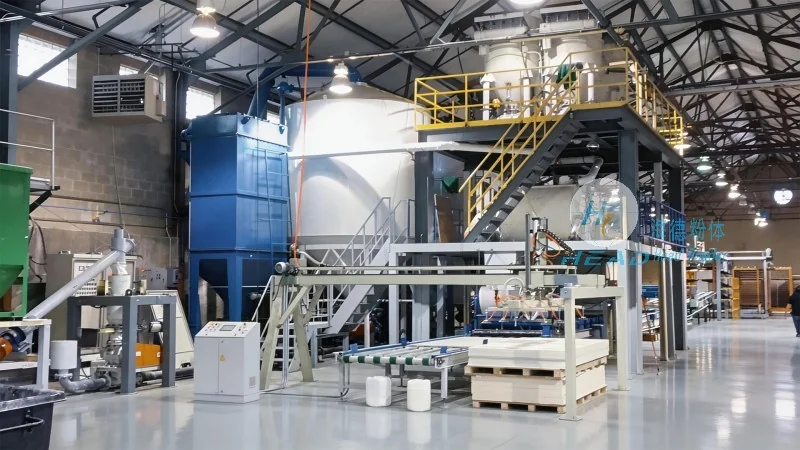
HeadPowder, a leading manufacturer in the field of fertilizer handling technology, specializes in providing high-quality material handling solutions. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for agricultural operations worldwide. HeadPowder's products are designed to meet the diverse needs of the fertilizer industry, offering reliable and efficient equipment that enhances operational efficiency and reduces costs. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced production equipment and skilled engineering teams. HeadPowder's dedication to quality and customer service has earned it a reputation for excellence in the fertilizer handling sector.




