Denitration fly ash powder conveying system equipment is a specialized device designed for the efficient transportation of denitration fly ash, a byproduct from flue gas desulfurization and denitrification processes in thermal power plants and industrial facilities. This equipment plays a crucial role in the entire waste treatment and resource utilization chain, ensuring that fly ash is transported safely and effectively from the denitration unit to storage or further processing areas. The system integrates advanced engineering principles and robust construction to meet the demanding requirements of industrial applications.
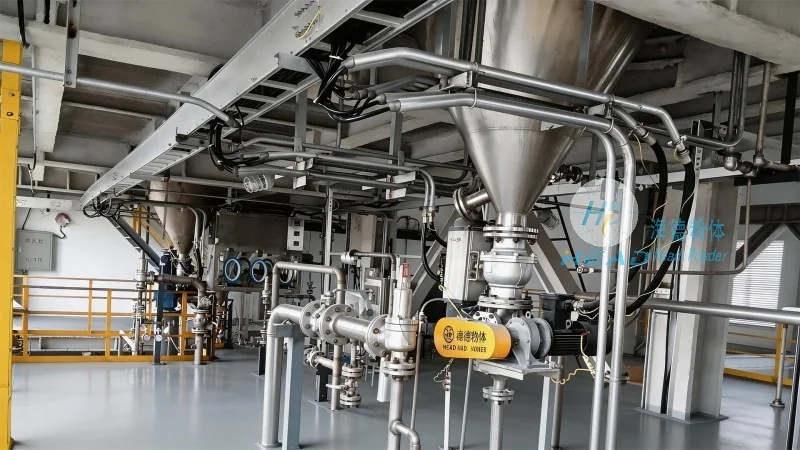
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the manufacturer of this denitration fly ash powder conveying system, is a leading enterprise based in Shandong, China. With a strong commitment to technological innovation and quality control, the company specializes in providing comprehensive solutions for powder handling and conveying systems. HeadPowder's team of experienced engineers and technicians leverages years of industry expertise to develop equipment that meets international standards while addressing the unique challenges of each client's operational environment. The company's headquarters and main production facilities are located in Shandong, China, where state-of-the-art manufacturing processes and rigorous quality assurance protocols are implemented to ensure the reliability and durability of all products.
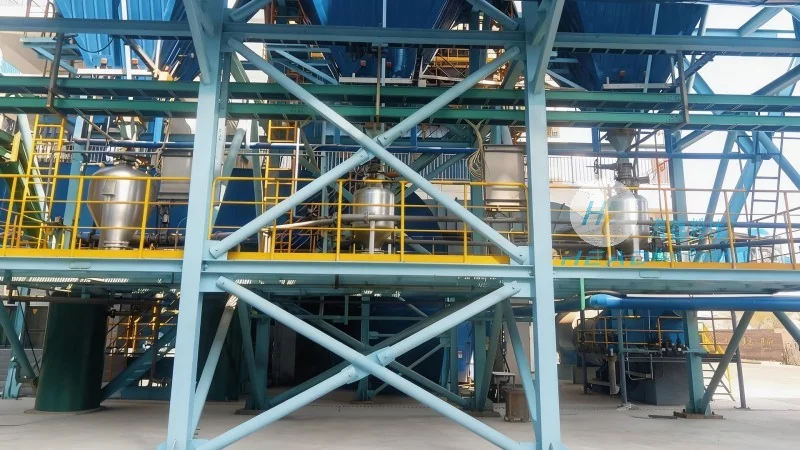
Principle of Denitration Fly Ash Powder Conveying System
The denitration fly ash powder conveying system operates based on the principle of pneumatic or mechanical conveying, depending on the specific design and application requirements. Pneumatic conveying systems utilize compressed air to transport the fly ash particles through a network of pipes, while mechanical systems employ screw conveyors, belt conveyors, or bucket elevators to move the material. The choice of conveying method is determined by factors such as the ash's moisture content, particle size distribution, and the distance and elevation changes between the source and destination points. In pneumatic systems, the fly ash is typically mixed with air in a hopper or feeder, and the mixture is then propelled through the pipeline by high-pressure air. The system includes components like air compressors, dust collectors, and control valves to regulate the flow and ensure efficient operation. Mechanical systems, on the other hand, rely on the physical movement of the ash within the conveyor's housing, often using augers or belts to transport the material. Both types of systems are designed to minimize material degradation, prevent blockages, and maintain a consistent flow rate, which is critical for maintaining the efficiency of downstream processes.
Working Scene Characteristics of the Conveying System
The denitration fly ash powder conveying system is widely used in various industrial working scenes, particularly in thermal power plants, cement factories, and industrial waste treatment facilities. In thermal power plants, the system is typically installed in the fly ash handling area, where it connects the denitration unit to the ash storage silos or the ash utilization facilities. The working scene in this environment involves handling large volumes of fly ash, often with high moisture content and varying particle sizes. The system must be capable of handling these conditions without clogging or losing efficiency. In cement factories, the system is used to transport fly ash as a raw material for cement production, where it is mixed with other components to improve the cement's properties. The working scene here requires the system to maintain a stable flow rate and ensure the consistent quality of the fly ash feed. Additionally, the system is used in industrial waste treatment facilities where the fly ash is processed for resource recovery, such as in the production of building materials or as a soil amendment. The working scene in these facilities involves handling fly ash with different characteristics, such as higher or lower moisture content, and requires the system to be adaptable to these variations. The key characteristics of the working scene include the need for high reliability, low maintenance, and the ability to operate continuously for extended periods without interruption. The system is designed to withstand the harsh conditions of industrial environments, including high temperatures, dust, and corrosive substances, ensuring long-term performance and minimal downtime.
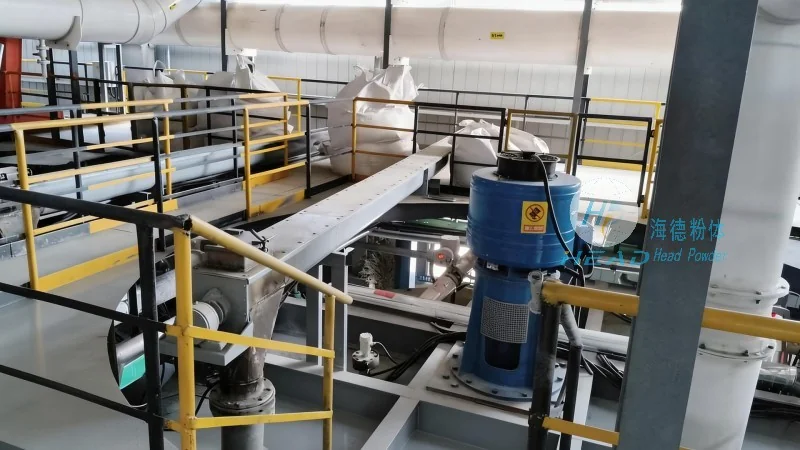
Advantages and Applications in Different Industrial Environments
The denitration fly ash powder conveying system offers several advantages that make it suitable for a wide range of industrial applications. One of the primary advantages is its ability to handle large volumes of fly ash efficiently, reducing the need for manual handling and improving workplace safety. The system also minimizes the environmental impact by preventing dust emissions and ensuring that the fly ash is transported in a controlled manner. Another advantage is the flexibility of the system, which can be customized to meet the specific requirements of different industrial settings. For example, the system can be designed with different conveying capacities, pressure levels, and control systems to suit the needs of thermal power plants, cement factories, or waste treatment facilities. The system's reliability and durability are also significant advantages, as it is built to withstand the demanding conditions of industrial operations and require minimal maintenance. In terms of applications, the system is used in various industries where fly ash is a byproduct, including power generation, cement manufacturing, and industrial waste management. The system's ability to transport fly ash over long distances and at high speeds makes it an essential component in the overall waste management and resource utilization strategy of these industries. Additionally, the system's integration with other equipment, such as ash storage silos and utilization facilities, allows for a seamless flow of materials, improving the overall efficiency of the production process.




