Denitrizer material handling systems are essential infrastructure in industrial facilities that employ selective catalytic reduction (SCR) technology to reduce nitrogen oxide (NOx) emissions. These systems are responsible for the storage, transport, and precise dosing of denitrifier agents, such as urea or aqueous ammonia, to the injection points within the exhaust stream. The effectiveness of these systems directly influences the efficiency and reliability of the denitrification process, making them a critical component in modern industrial operations. As environmental regulations tighten and the demand for cleaner exhaust increases, the design and operation of denitrizer material handling systems have become increasingly important for facility owners and operators.
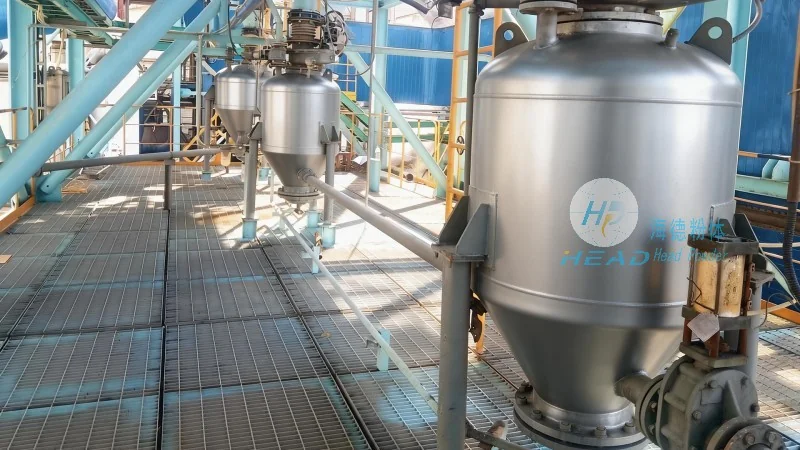
Principle of Denitrizer Material Handling Systems
The fundamental principle of denitrizer material handling systems is to ensure the accurate and consistent delivery of the denitrifier agent to the points of application. The system typically comprises several interconnected components, including storage tanks, pumps, dosing units, and conveying equipment. The storage tanks are designed to hold the liquid denitrifier, which is then pumped through a network of pipes to the injection points. The pumps are responsible for maintaining the required pressure and flow rate, while the dosing units regulate the concentration and flow rate of the agent, ensuring that the correct amount is delivered. The conveying equipment, which may include pneumatic or mechanical systems, transports the agent from the storage area to the injection points, maintaining consistent pressure and flow. The entire system operates under strict control, often integrated with the plant's control system, to enable real-time monitoring and adjustment of the system's parameters. This integration allows for dynamic response to changes in the exhaust stream, ensuring optimal denitrification performance.
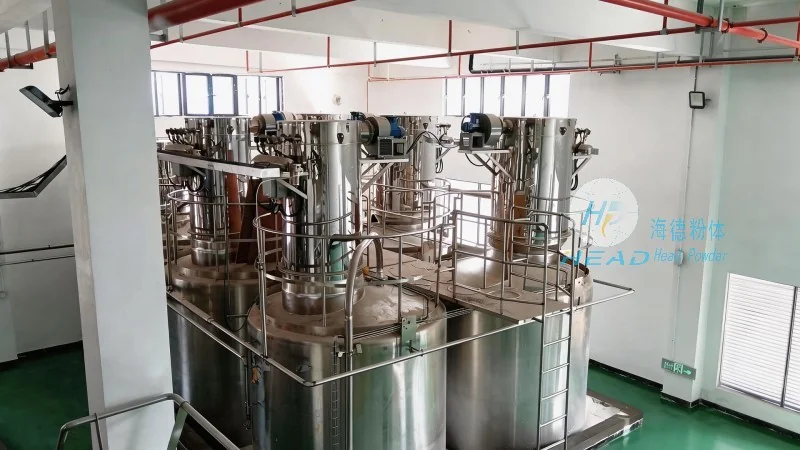
Working Scene Characteristics of Denitrizer Material Handling Systems
The working scene characteristics of denitrizer material handling systems vary significantly based on the specific industrial application and plant layout. In large-scale power plants, for instance, these systems are designed to handle high volumes of denitrifier, with capacities ranging from tens to hundreds of cubic meters. The systems are engineered to operate continuously, with redundancy features such as backup pumps and storage tanks to prevent downtime in case of equipment failure or maintenance. The conveying equipment in such systems often includes large-diameter pipes and robust pumps to handle the high flow rates and pressures. In contrast, in smaller industrial facilities, the systems may be more compact, with lower flow rates and simpler control mechanisms. The working environment in power plants, for example, involves high temperatures and pressures, requiring the system components to be made from corrosion-resistant materials like stainless steel. In petrochemical plants, the systems must also be able to handle the presence of corrosive gases and chemicals, adding another layer of complexity to their design. Additionally, the systems are often located in remote or hazardous areas, necessitating robust safety features and easy access for maintenance personnel.
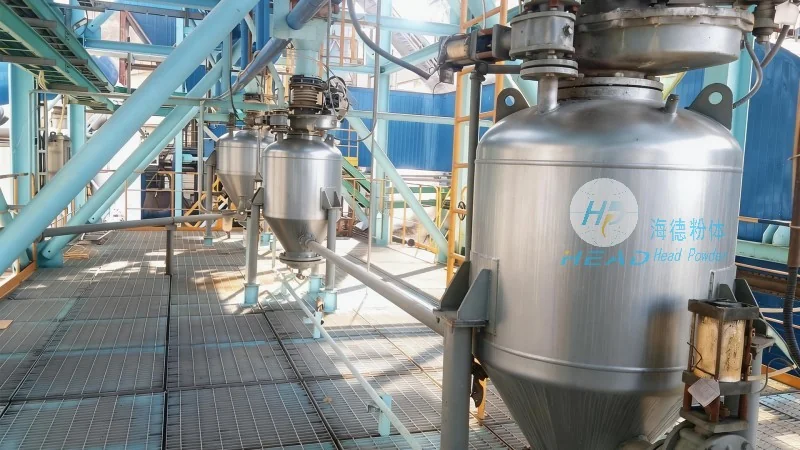
Key Features and Advantages of Denitrizer Material Handling Systems from Shandong HeadPowder Engineering Co., Ltd.
Denitrizer material handling systems manufactured by Shandong HeadPowder Engineering Co., Ltd. are characterized by their advanced technology, high reliability, and adherence to international standards. The company specializes in designing and manufacturing systems tailored to the specific needs of industrial facilities, ensuring optimal performance and compliance with environmental regulations. One of the key features of their systems is the use of high-quality, corrosion-resistant materials, such as stainless steel and special alloys, which are resistant to the harsh chemicals and temperatures encountered in industrial environments. The pumps and dosing units are equipped with advanced control technology, including digital control panels and sensors, allowing for precise and consistent delivery of the denitrifier agent. The conveying equipment is optimized for low maintenance and high efficiency, with features like self-cleaning mechanisms and energy-efficient motors. Furthermore, the systems are designed with safety in mind, incorporating features such as pressure relief valves, leak detection systems, and emergency shutdown capabilities. These features ensure that the system operates safely and reliably, minimizing the risk of accidents and downtime.




