Calcium nitrite is a critical chemical compound widely used in various industrial applications, including flame retardants, water treatment, and construction materials. The efficient handling and transportation of calcium nitrite are essential for maintaining production efficiency and ensuring product quality. This article explores the principle and working scene characteristics of a specialized material handling system designed for calcium nitrite, highlighting its operational mechanisms and practical applications.
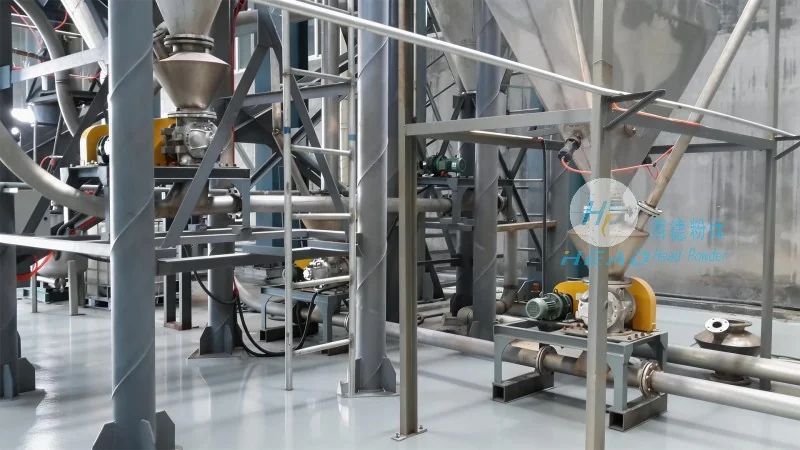
System Principle: How the Calcium Nitrite Material Handling System Operates
The calcium nitrite material handling system is engineered to handle the unique properties of calcium nitrite, such as its hygroscopic nature and potential reactivity under certain conditions. The system typically incorporates advanced pneumatic or mechanical conveying technologies to ensure safe and efficient transport. Key components include dust collection systems, temperature control mechanisms, and specialized valves to prevent material degradation or contamination. The design prioritizes minimal material exposure to air and moisture, which are critical factors in preserving the chemical integrity of calcium nitrite. By integrating these elements, the system achieves consistent and reliable material flow, reducing downtime and operational risks.
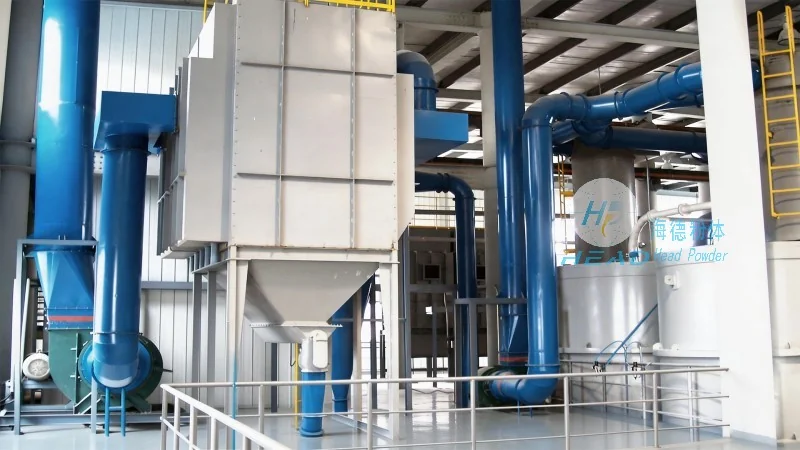
Working Scene Characteristics: Practical Applications and Operational Environments
The working scene characteristics of the calcium nitrite material handling system are tailored to diverse industrial settings. In manufacturing facilities, the system is often integrated into production lines for continuous material supply to reactors or processing units. It is also used in storage facilities to transfer calcium nitrite from bulk storage silos to packaging or blending equipment. The system's adaptability allows it to operate in both indoor and outdoor environments, though indoor installations are more common to control environmental factors like humidity and temperature. The design accommodates varying material flow rates, from low to high throughput, making it suitable for different production scales. Additionally, the system is equipped with safety features, such as emergency shut-off valves and pressure relief systems, to mitigate risks associated with material handling in industrial settings.
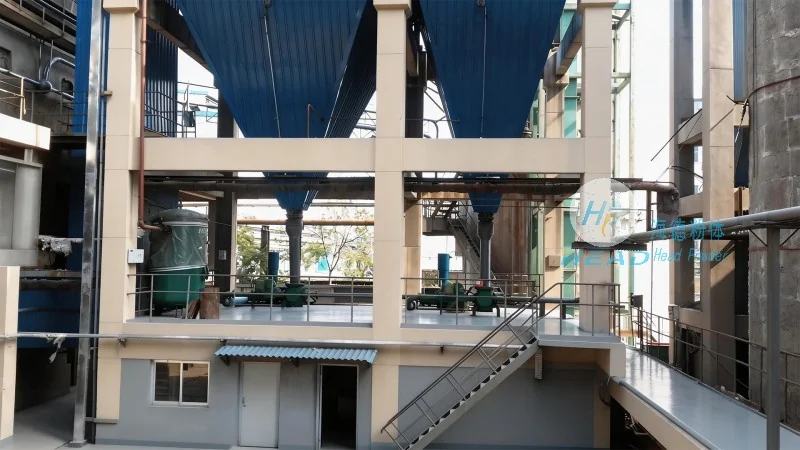
Advantages in Practical Applications: Efficiency and Reliability
One of the primary advantages of the calcium nitrite material handling system is its ability to maintain the chemical stability of the material during transport. The system's enclosed design minimizes exposure to air and moisture, which can cause degradation or changes in the material's properties. This is particularly important for calcium nitrite, as it can react with certain substances or degrade over time if not handled properly. The system also enhances operational efficiency by reducing manual handling and minimizing material loss. Automated control systems allow for precise flow regulation, ensuring consistent delivery to downstream processes. Furthermore, the system's durability and low maintenance requirements contribute to long-term cost savings for industrial users. By addressing the specific challenges of calcium nitrite handling, the system provides a reliable solution for industries that rely on this chemical compound.
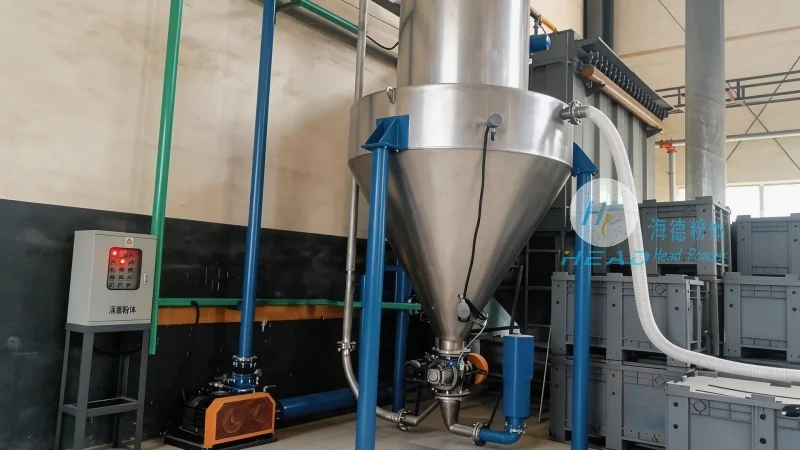
About HeadPowder: Expertise in Material Handling Solutions
HeadPowder, a leading provider of engineering solutions, specializes in designing and manufacturing material handling systems tailored to the needs of various industries. With a focus on innovation and quality, HeadPowder has developed advanced technologies for handling challenging materials like calcium nitrite. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-performance solutions. HeadPowder's commitment to customer satisfaction and technical excellence has established it as a trusted partner for businesses seeking reliable material handling systems. The company's team of engineers and technicians works closely with clients to understand their specific requirements and provide customized solutions that meet their operational needs.




