Principle and Working Scene Characteristics of Wet Sodium Nitrate Material Handling Systems
Release time:2026-09-19 11:01:30
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Wet sodium nitrate, a critical chemical compound widely used in fertilizer production, mining, and industrial applications, requires specialized handling systems to ensure safe and efficient transportation. The material handling system for wet sodium nitrate is designed to manage the unique properties of this compound, including its moisture content and potential reactivity. This system integrates advanced engineering solutions to address the challenges associated with transporting such materials, ensuring compliance with safety standards and operational efficiency.
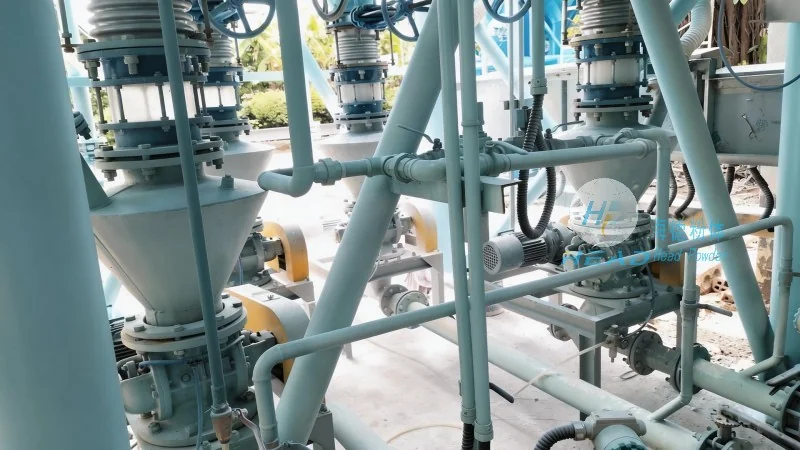
Principle of Operation for the Material Handling System
The core principle of the wet sodium nitrate material handling system is to maintain the material's integrity while facilitating smooth transport. The system typically employs a combination of conveyor technologies, such as belt conveyors or screw conveyors, tailored to handle the moisture content and bulk density of wet sodium nitrate. Key components include feeding mechanisms, which evenly distribute the material into the conveyor, and control systems that regulate the flow rate to prevent overloading or material degradation. The design also incorporates moisture management features, such as drainage or drying sections, to minimize the risk of slippage or clogging in the conveying equipment. Additionally, the system may include safety features like overfill sensors and emergency stop buttons to mitigate potential hazards associated with the material's handling.
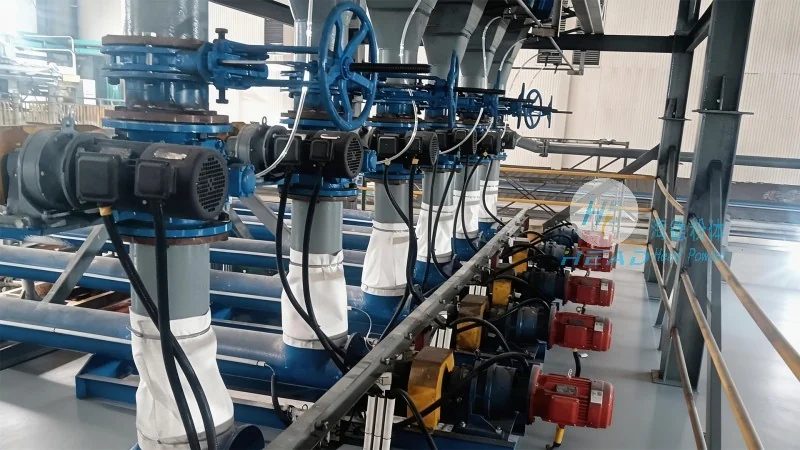
Working Scene Characteristics and Application Scenarios
The working scene characteristics of the wet sodium nitrate material handling system are shaped by the diverse industrial environments where it is deployed. In fertilizer manufacturing plants, for instance, the system is integrated into the production line to transport wet sodium nitrate from processing units to storage or packaging areas. The system must handle high volumes of material while maintaining consistent moisture levels to ensure the quality of the final fertilizer product. In mining operations, the material handling system may be used to transport ore containing sodium nitrate, where the system's robust design is essential to withstand harsh conditions and potential abrasion from the ore. The system's adaptability to different working environments is a critical factor, as it must be scalable to accommodate varying production rates and material characteristics. Furthermore, the system's integration with other industrial processes, such as mixing or drying, allows for a seamless workflow, enhancing overall operational efficiency.
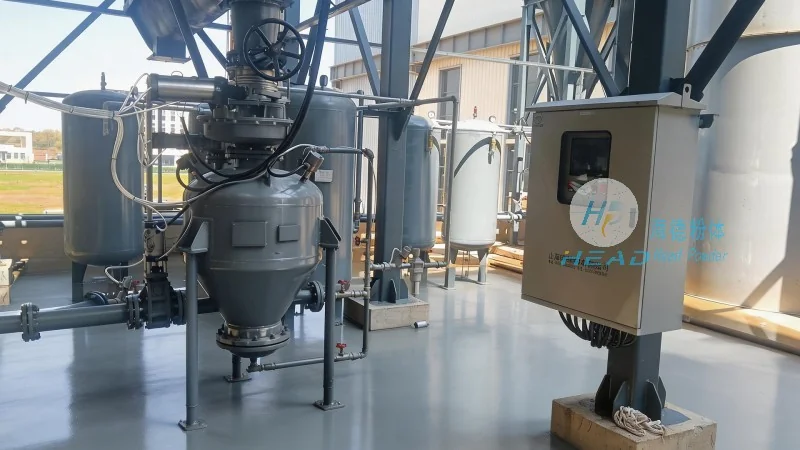
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling systems for various industrial applications. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner in the chemical and mining industries. The company's expertise in handling challenging materials like wet sodium nitrate has enabled it to develop systems that meet the highest safety and performance standards. HeadPowder's commitment to quality and reliability is reflected in its comprehensive product line, which includes customized solutions tailored to the specific needs of each client. The company's team of experienced engineers and technicians ensures that every system is designed to optimize operational efficiency while minimizing downtime and maintenance costs.




