HeadPowder, a leading provider in the field of powder handling technology, specializes in advanced pneumatic conveying systems designed for the efficient transport of nanometer calcium carbonate powders. This article explores the fundamental principles underlying such systems and highlights the key characteristics of their operational environments.
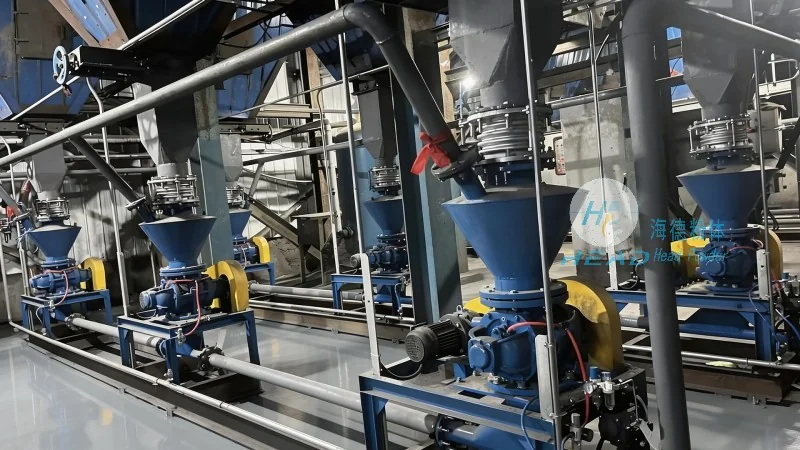
About HeadPowder Engineering Co., Ltd.
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted partner in the industrial sector, focusing on delivering innovative solutions for powder processing and material handling. With a strong commitment to quality and technological advancement, HeadPowder offers a range of products and services tailored to meet the diverse needs of its clients.
Understanding Pneumatic Conveying Systems for Nanometer Calcium Carbonate
Nanometer calcium carbonate is a fine powder with unique properties that require specialized handling methods to ensure optimal performance and safety. Pneumatic conveying systems utilize air or other gases to transport these powders from one location to another, eliminating the need for mechanical components like belts or buckets that might cause contamination or damage to the product. The core principle of these systems involves creating a pressure differential to move the powder through a pipeline, often using a combination of positive and negative pressure zones to achieve efficient and reliable transport.
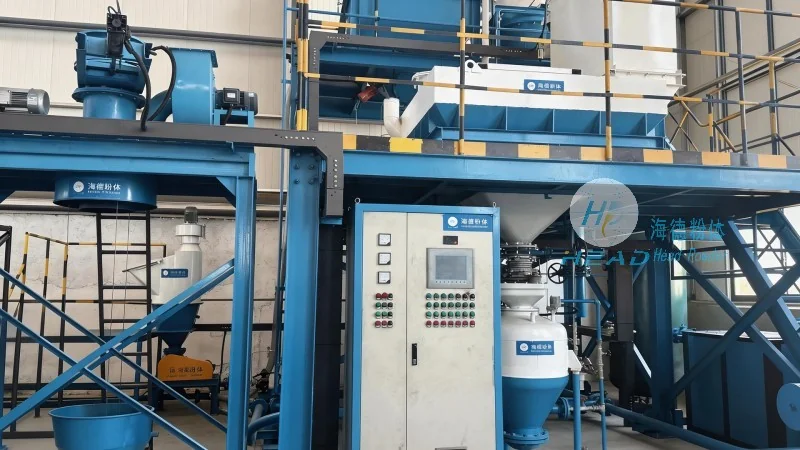
Key Working Scene Characteristics
The operational environment of a nanometer calcium carbonate pneumatic conveying system is characterized by several critical factors that influence its design and performance. Firstly, the system must be capable of handling the high fineness and low bulk density of the powder, which can lead to issues such as caking or agglomeration if not properly managed. Advanced systems incorporate features like in-line mixing, temperature control, and moisture management to maintain the powder's quality throughout the conveying process.
Secondly, the system's design must consider the potential for dust generation and the need for effective dust control measures. Pneumatic conveying systems typically include filtration and collection systems to ensure compliance with environmental regulations and to protect personnel from exposure to fine particles. Additionally, the system's scalability and adaptability are crucial, as industrial applications may require varying capacities and configurations to accommodate different production volumes and process requirements.
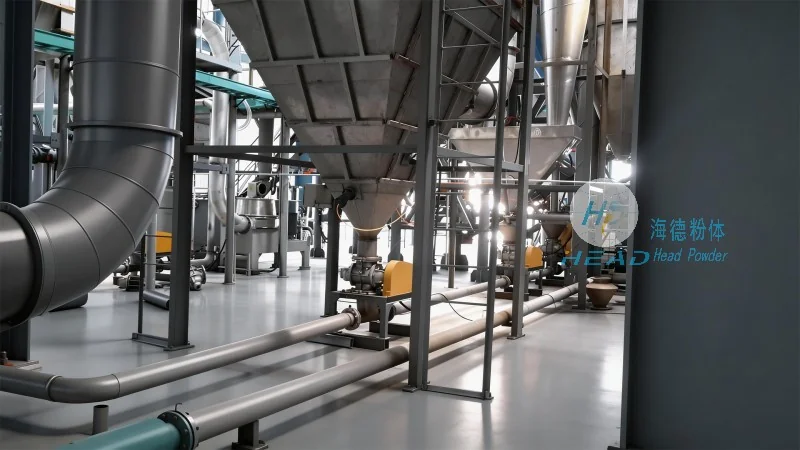
Practical Applications and System Integration
The working scene characteristics of these systems are directly linked to their practical applications in various industries. For instance, in the paper and plastic manufacturing sectors, nanometer calcium carbonate is commonly used as a filler or reinforcement material. The pneumatic conveying system must be integrated seamlessly with existing production lines, ensuring smooth material flow and minimal downtime. This integration often involves customizing the system's components, such as the hopper design, pipeline layout, and control mechanisms, to align with the specific requirements of the end-user.
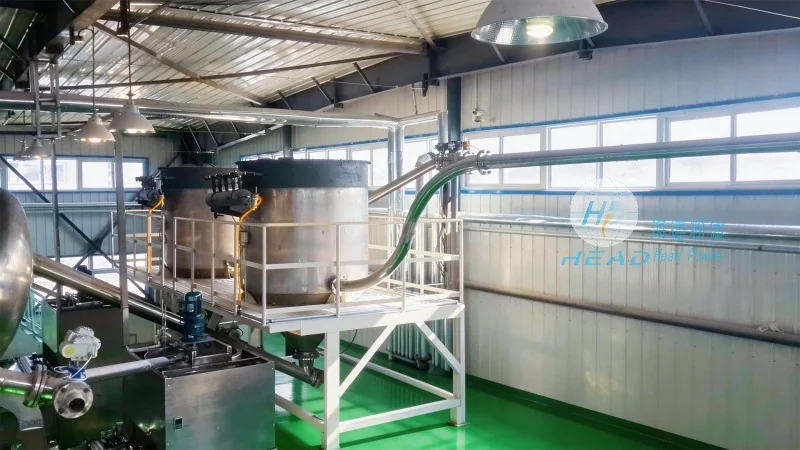
Furthermore, the system's reliability and maintenance requirements are key considerations in operational environments. High-quality materials and robust construction are essential to withstand the abrasive nature of the powder and the continuous operational demands. Regular maintenance, including filter cleaning and component inspection, is necessary to ensure the system operates efficiently and prolong its service life. The working scene also includes considerations for energy efficiency, as pneumatic conveying systems can consume significant amounts of air, and optimizing air usage is a critical aspect of system design.
Conclusion
In summary, the pneumatic conveying system for nanometer calcium carbonate is a sophisticated piece of equipment that combines principles of fluid dynamics and material science to achieve efficient and safe powder transport. The working scene characteristics, including the powder's properties, environmental regulations, and industrial integration requirements, play a vital role in determining the system's design and performance. HeadPowder Engineering Co., Ltd., with its expertise and commitment to innovation, continues to provide tailored solutions that meet the evolving needs of the industry, ensuring the reliable and efficient handling of nanometer calcium carbonate powders in various operational settings.




