HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced powder handling systems. The company's core product, the tonne bag unloading powder conveying line, is engineered to efficiently manage bulk powder transfer from large bags to processing equipment. This system is a critical component for industries that rely on consistent and reliable powder handling, such as food processing, chemical manufacturing, and pharmaceutical production.
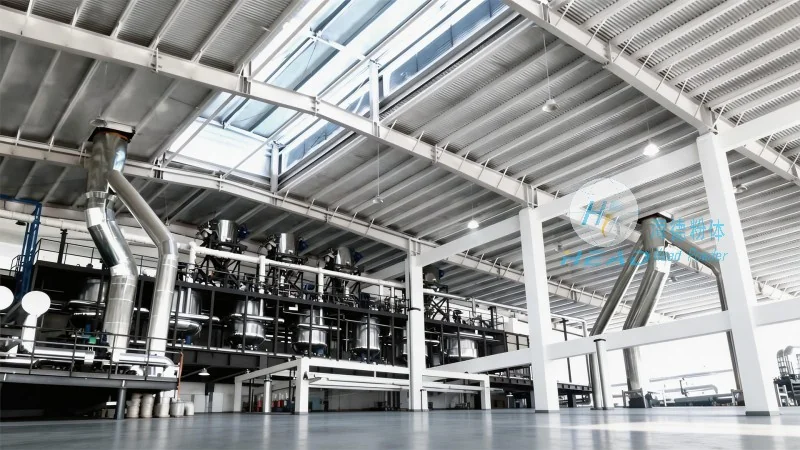
Overview of the Tonne Bag Unloading Powder Conveying Line
The tonne bag unloading powder conveying line is a comprehensive solution that integrates multiple functional units to streamline the entire powder handling process. At its core, the system is designed to handle large capacity bags, typically with a capacity of 1 tonne (or 1000 kg), and transfer the contained powder to downstream equipment like mixers, reactors, or storage silos. The system's modular design allows for customization based on specific application requirements, ensuring optimal performance and efficiency.
Key Components and Their Functions
The tonne bag unloading powder conveying line typically consists of several key components, each playing a crucial role in the overall operation. The primary components include the bag opening mechanism, the powder suction or discharge system, the conveyor system (such as a screw conveyor or pneumatic conveyor), and the control panel. Each component is engineered to work in harmony to ensure smooth and continuous operation.
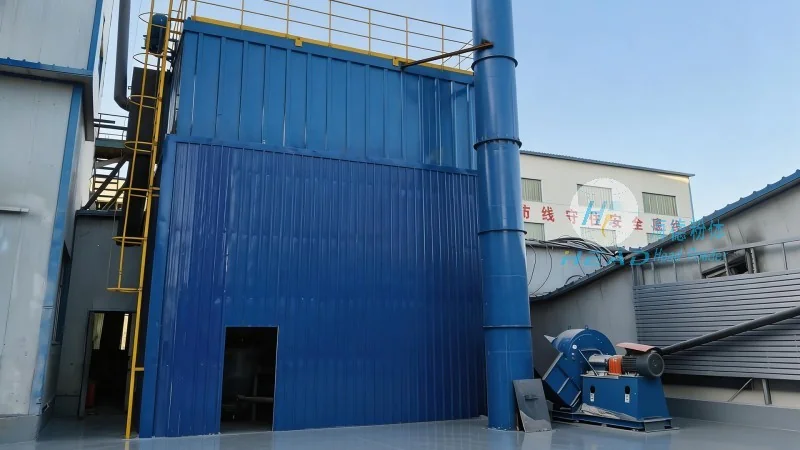
Operation Process of the Tonne Bag Unloading Powder Conveying Line
The operation of the tonne bag unloading powder conveying line follows a systematic sequence to ensure efficient and safe powder transfer. The process begins with the placement of a tonne bag onto the bag stand or lifting frame. The bag opening mechanism, which may include a valve or a cutting device, is then activated to open the bag and allow the powder to be released. Simultaneously, the powder suction or discharge system is engaged, creating a controlled airflow or pressure differential to draw the powder from the bag and direct it into the conveyor system.
The conveyor system, which can be either a screw conveyor or a pneumatic conveyor, then transports the powder to the next stage of processing. In a screw conveyor, the rotating screw pushes the powder forward, while in a pneumatic conveyor, the powder is carried by air flow through a pipeline. The control panel monitors and regulates the entire process, ensuring that the flow rate, pressure, and other parameters are maintained within optimal ranges. The system may also include a dust collection system to capture any airborne particles and prevent contamination or environmental issues.
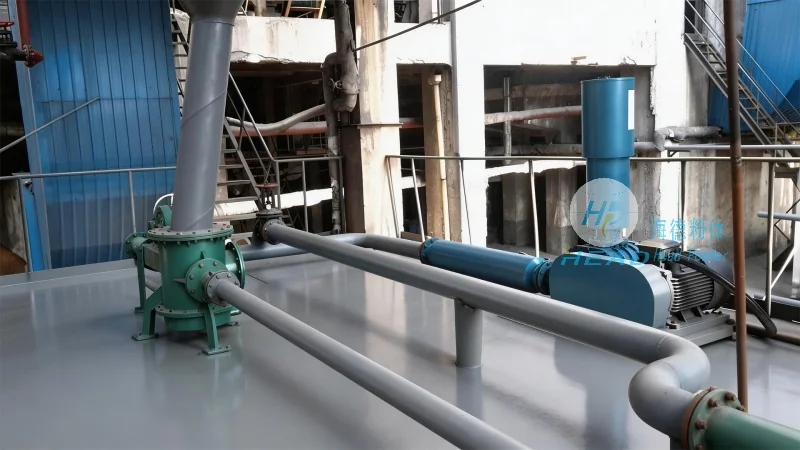
Working Principle of the Tonne Bag Unloading Powder Conveying Line
The working principle of the tonne bag unloading powder conveying line is based on the principles of fluid dynamics and mechanical engineering. The system utilizes a combination of mechanical and pneumatic forces to transfer the powder from the bag to the conveyor. The bag opening mechanism ensures that the powder is released in a controlled manner, preventing spillage or blockages. The suction or discharge system creates a pressure difference that draws the powder into the conveyor, while the conveyor itself moves the powder along the designated path. The control panel provides real-time monitoring and adjustment of the system's parameters, ensuring that the operation is efficient and safe.
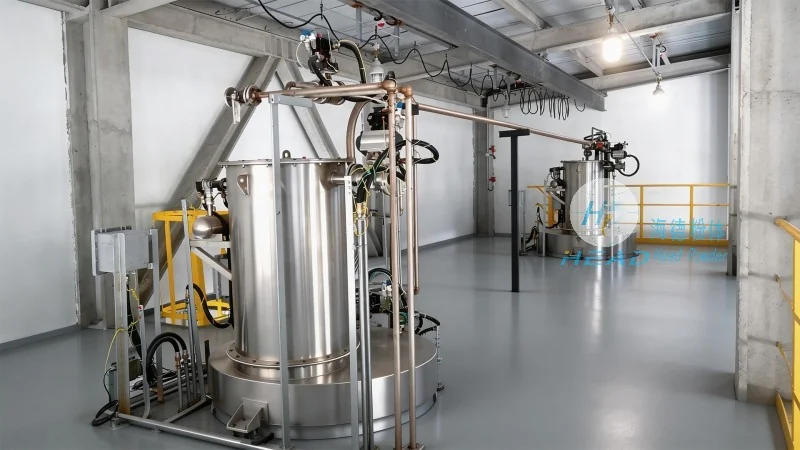
Advantages and Applications
The tonne bag unloading powder conveying line offers several advantages over traditional manual handling methods. It significantly reduces labor costs and improves operational efficiency by automating the entire powder transfer process. The system also minimizes the risk of powder contamination and exposure to personnel, enhancing workplace safety. Additionally, the modular design allows for easy integration with existing processing equipment, making it a versatile solution for various industrial applications.
HeadPowder's tonne bag unloading powder conveying line is widely used in industries that require high-volume powder handling, such as food processing, where it is used to transfer ingredients like flour, sugar, and spices. In the chemical industry, it is used to handle raw materials like powders and granules. In the pharmaceutical industry, it is used to transfer active ingredients and excipients with high precision and minimal contamination. The system's ability to handle a wide range of powder types, from fine powders to coarse granules, makes it a versatile solution for various applications.




