Dry stone powder pneumatic conveying is a technology widely used in the industrial sector for the efficient transport of dry, non-clumping materials such as stone powders. This method leverages air as the primary medium to move bulk materials from one location to another, offering advantages like reduced equipment wear, lower maintenance costs, and the ability to handle materials in a dust-free environment. The system's design is tailored to ensure reliable and continuous material transfer, making it suitable for various applications in construction, mining, and chemical processing industries.
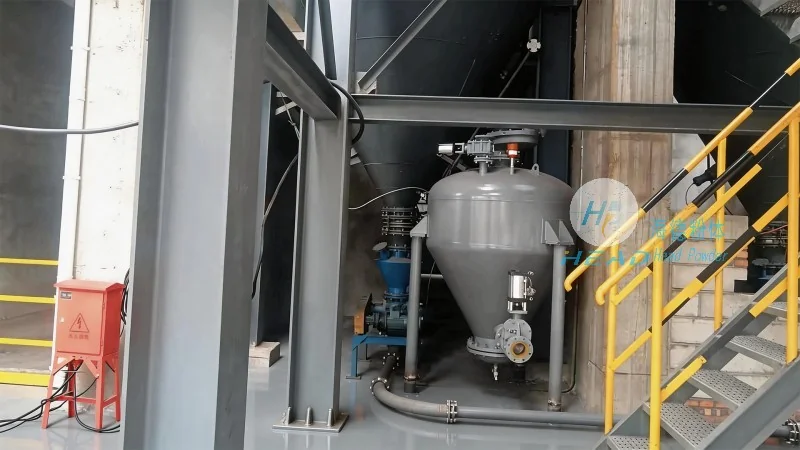
Key Components and Structural Design of Pneumatic Conveying Systems
The core components of a dry stone powder pneumatic conveying system include the material hopper, air compressor, conveying pipeline, and discharge unit. The material hopper is designed to store the dry stone powder, equipped with a feeding mechanism that controls the flow of material into the system. The air compressor generates the necessary air pressure to propel the material through the pipeline. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, is configured in a loop or straight line depending on the application requirements. The discharge unit, often a rotary valve or a dust collector, collects the material at the destination point, ensuring a clean and efficient transfer process.
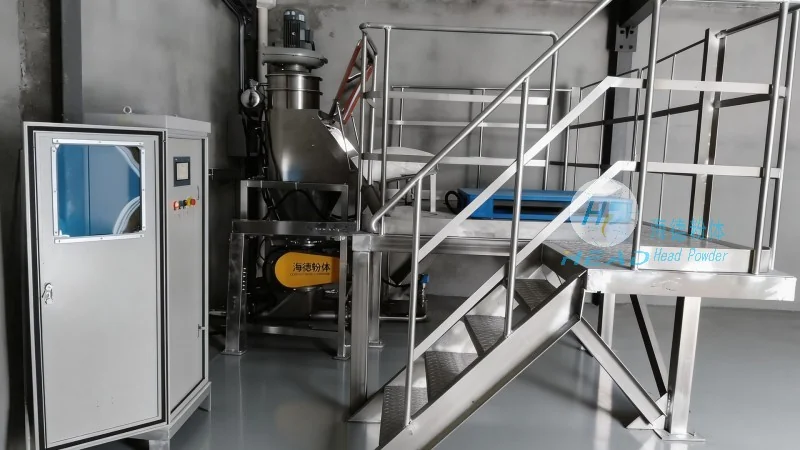
Working Principle of Pneumatic Conveying for Dry Stone Powders
The operation of a dry stone powder pneumatic conveying system involves several stages. Initially, the dry stone powder is fed from the hopper into the conveying pipeline under the pressure of the compressed air. The air, moving at high velocity, creates a flow that entrains the powder particles, forming a slurry-like mixture. This mixture travels through the pipeline to the discharge point. At the destination, the air is separated from the powder, often through a cyclone or filter system, and the powder is collected. The air is then either recirculated or vented, depending on the system design. This process ensures that the material is transported without the need for mechanical conveyors, reducing the risk of contamination and material degradation.
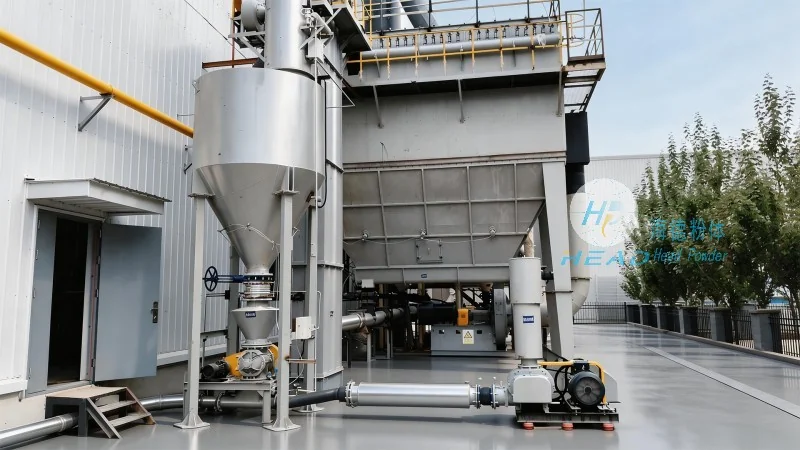
Advantages of Using Pneumatic Conveying for Dry Stone Powders
Compared to traditional mechanical conveying methods, dry stone powder pneumatic conveying offers several benefits. Firstly, it minimizes material degradation and contamination, as the material is handled in an enclosed system. Secondly, it reduces labor costs and maintenance requirements, as there are fewer moving parts compared to belt or screw conveyors. Thirdly, the system can handle materials with varying particle sizes and moisture content, making it versatile for different applications. Additionally, the ability to transport materials over long distances without intermediate storage points enhances operational efficiency. These advantages make pneumatic conveying an ideal solution for industries dealing with dry stone powders, ensuring reliable and cost-effective material transport.
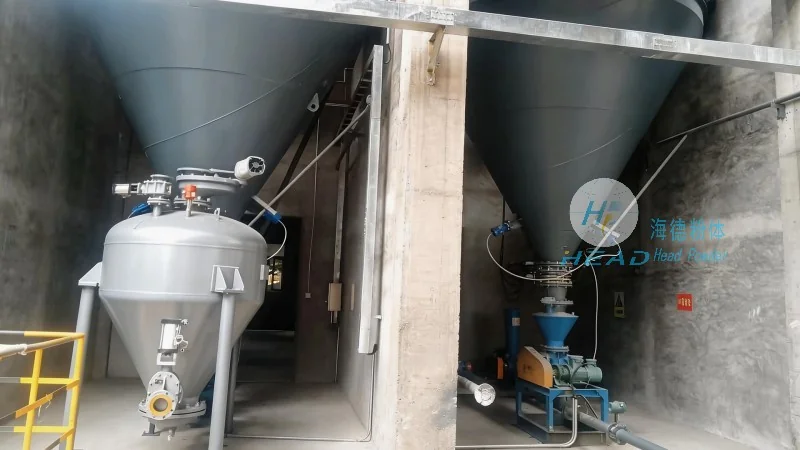
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying systems for industrial applications. With a focus on innovation and quality, the company specializes in designing and manufacturing customized solutions tailored to the specific needs of clients in the construction, mining, and chemical sectors. HeadPowder's products are known for their durability, efficiency, and compliance with industry standards. The company's headquarters is located in Shandong, China, where it leverages advanced technology and experienced engineering teams to develop cutting-edge pneumatic conveying systems. By providing reliable and efficient solutions, headpowder helps industries optimize their material handling processes, reducing costs and improving overall operational performance.




