Coal ash, as a byproduct of coal combustion in thermal power plants, poses significant challenges in handling and transportation due to its fine powder characteristics and potential environmental impacts. Efficient and reliable equipment for coal ash powder conveying is crucial for industrial operations, ensuring safe and effective material transport while minimizing dust emissions and operational risks. This article provides an overview of coal ash powder conveying equipment, focusing on its structural design and operational principles, with an emphasis on the technology and solutions offered by Shandong HeadPowder Engineering Co., Ltd.
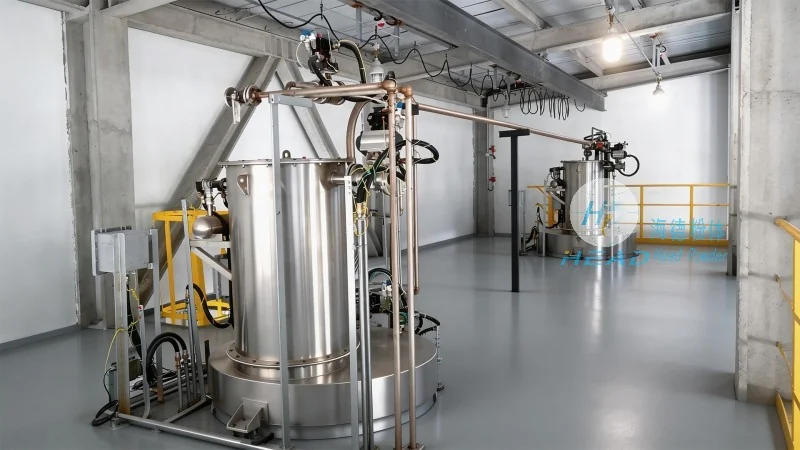
Overview of Coal Ash Powder Conveying Equipment
Coal ash powder conveying equipment is specifically designed to handle the transportation of coal ash, a fine particulate material that requires specialized handling due to its dustiness and potential health hazards. The primary goal of such equipment is to transport coal ash from the source (e.g., ash hoppers, storage silos) to disposal or utilization sites, such as landfills, recycling facilities, or power plant reutilization processes. The equipment must address challenges like dust control, material flow stability, and operational efficiency, making it a critical component in the overall coal ash management system.
Key Components and Structural Design of Coal Ash Powder Conveying Equipment
The structural design of coal ash powder conveying equipment typically includes several key components that work in tandem to ensure reliable operation. These components are engineered to handle the unique properties of coal ash, including its fine particle size, moisture content, and potential agglomeration. The main structural elements include:
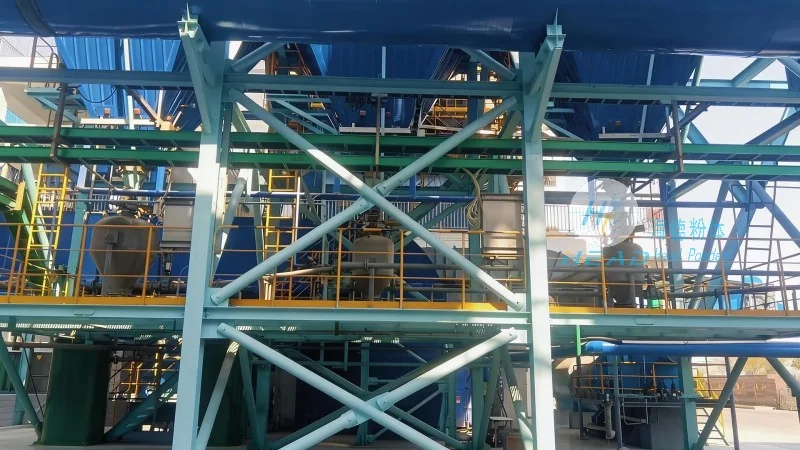
- Feeding System: This component is responsible for introducing coal ash into the conveying system. It may include hoppers, feeders, or rotary valves that control the flow rate and prevent blockages. The design of the feeding system is critical to ensure a consistent and controlled feed of coal ash, which is essential for stable conveying.
- Conveying Pipe: The conveying pipe is the main channel through which coal ash is transported. It is usually made of materials resistant to corrosion and abrasion, such as stainless steel or special alloys, to withstand the abrasive nature of coal ash particles. The pipe is often equipped with internal liners or coatings to extend its service life and reduce wear. The pipe layout may vary depending on the application, including horizontal, vertical, or inclined configurations, with bends and elbows designed to minimize pressure losses and maintain material flow.
- Pneumatic Conveying System: Many coal ash powder conveying systems utilize pneumatic conveying, where air is used to transport the material. This system typically includes a blower or compressor to generate the necessary air pressure, a filter system to capture dust and prevent environmental contamination, and a receiver or discharge hopper at the destination. The pneumatic system is effective for long-distance or high-rise conveying, as it can handle both dilute and dense phase flows, depending on the application requirements.
- Control and Monitoring System: A sophisticated control and monitoring system is integrated into the equipment to ensure safe and efficient operation. This system may include sensors for flow rate, pressure, temperature, and dust levels, as well as control panels for adjusting parameters such as air pressure, feed rate, and system speed. The control system also includes safety features, such as emergency shut-off valves and dust suppression mechanisms, to prevent accidents and environmental pollution.
Working Principle of Coal Ash Powder Conveying Equipment
The working principle of coal ash powder conveying equipment involves the coordinated operation of its components to transport coal ash from the source to the destination. The process typically begins with the feeding system introducing coal ash into the conveying pipe. In a pneumatic conveying system, the blower generates air pressure, which is introduced into the pipe, creating a flow that carries the coal ash particles along with it. The air and material mixture travels through the pipe, with bends and elbows designed to maintain the flow direction and minimize pressure losses. At the destination, the air and material mixture is separated, with the air being filtered and the coal ash being discharged into the receiver or disposal site.
The control system plays a crucial role in regulating the operation of the conveying equipment. It monitors various parameters, such as flow rate and pressure, and adjusts the air pressure or feed rate as needed to maintain stable operation. The system also includes safety features to prevent overpressure or blockages, ensuring that the equipment operates within safe limits. Additionally, the dust suppression system is activated during operation to minimize dust emissions and protect the environment and personnel.
Applications and Benefits of Coal Ash Powder Conveying Equipment
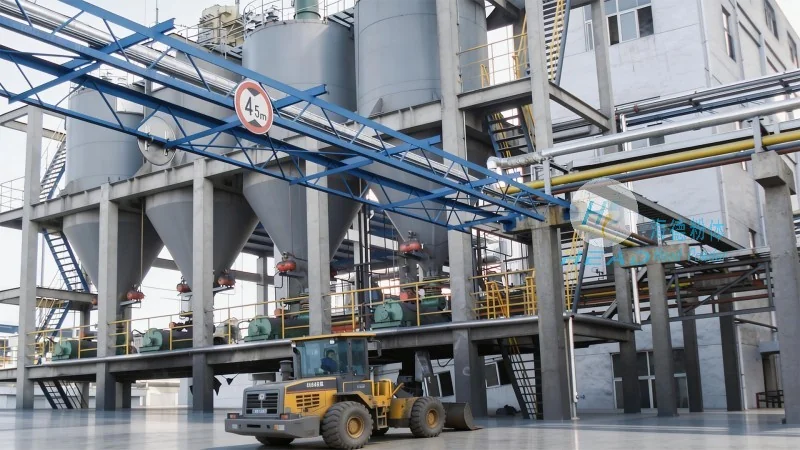
Coal ash powder conveying equipment is widely used in various industrial applications, particularly in thermal power plants, where coal ash is a byproduct of coal combustion. The equipment is also used in other industries, such as cement production, where coal ash is utilized as a raw material. The benefits of using specialized coal ash powder conveying equipment include:
- Efficient Material Transport: The equipment ensures efficient and reliable transportation of coal ash, reducing the time and cost associated with manual handling or traditional methods.
- Dust Control: The integrated dust suppression system minimizes dust emissions, protecting the environment and personnel from health hazards.
- Operational Safety: The control and safety features of the equipment prevent accidents and ensure safe operation, reducing the risk of injuries or environmental incidents.
- Reduced Maintenance: The robust design and materials used in the equipment reduce the need for frequent maintenance, lowering operational costs.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of coal ash powder conveying equipment and related industrial solutions. With its headquarters in Shandong, China, the company specializes in designing, manufacturing, and installing advanced coal ash handling systems tailored to the specific needs of its clients. HeadPowder's equipment is engineered to meet the highest standards of efficiency, reliability, and safety, ensuring that clients can manage their coal ash waste effectively and comply with environmental regulations.




