

Analysis of Powder Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer and supplier specializing in the design, development, and installation of advanced powder handling solutions. With a focus on innovation and quality, the company serves a wide range of industries, including chemical, food, pharmaceutical, and more. HeadPowder is headquartered in Shandong, China, providing local support and expertise to clients worldwide.
Introduction to Pneumatic Conveying Systems for Powders
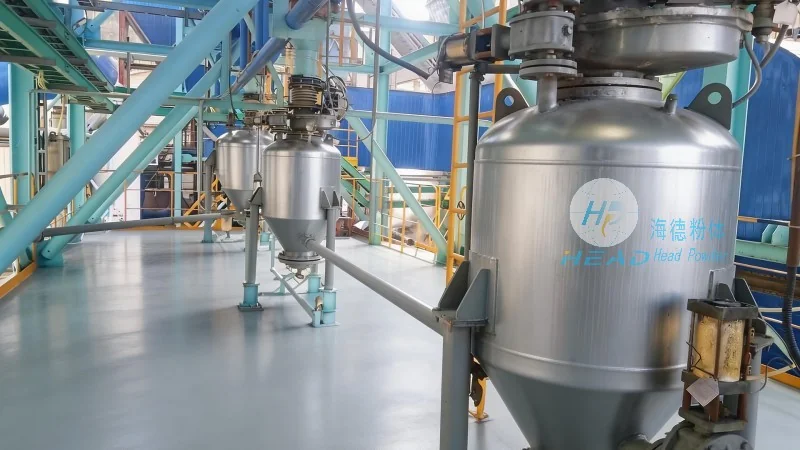
Pneumatic conveying systems are essential for the efficient and safe transportation of bulk powders over short to medium distances. These systems utilize compressed air or other gases to move powders through a network of pipes, offering a flexible and reliable alternative to traditional methods like conveyor belts or trucks. The core principle involves creating a pressure differential that propels the powder particles through the system, ensuring minimal product degradation and contamination.
Key Components and Their Functions in a Powder Pneumatic Conveying System
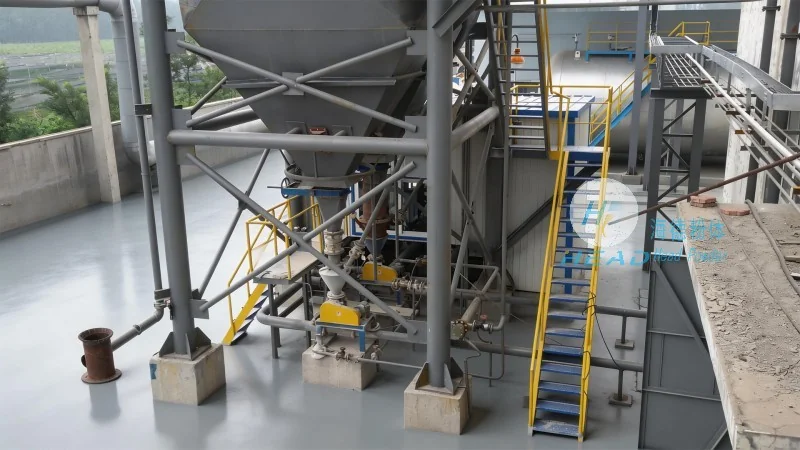
The effectiveness of a pneumatic conveying system for powders depends on several critical components, each playing a vital role in the overall operation. The primary components include the feed hopper, which holds the powder and regulates the flow into the system; the air supply unit, typically a compressor that generates the necessary pressure; the conveying line, which consists of pipes designed to withstand the pressure and material flow; and the separator, which separates the powder from the air at the end of the line. Additionally, air filters and dust collectors are often integrated to ensure environmental compliance and maintain system efficiency.
Advantages of Using Pneumatic Conveying Systems for Powder Handling
Compared to other powder handling methods, pneumatic conveying systems offer numerous advantages that make them a preferred choice for many industries. One of the most significant benefits is the ability to handle a wide variety of powders, from fine to coarse, without the need for additional equipment. The systems are also highly flexible, allowing for changes in layout or expansion without major modifications. Furthermore, they provide a closed-loop operation, reducing the risk of dust exposure and contamination, which is crucial in industries like food and pharmaceuticals. Maintenance requirements are generally lower than traditional systems, as the components are designed for durability and ease of repair.
Applications in Different Industries
Pneumatic conveying systems for powders are widely used across various sectors due to their adaptability and efficiency. In the chemical industry, they are used to transport raw materials and finished products, ensuring a smooth production process. The food industry benefits from these systems by maintaining hygiene standards and preventing cross-contamination during the handling of ingredients like flour, sugar, and spices. In the pharmaceutical sector, the closed-loop design and minimal human contact make pneumatic conveying ideal for transporting active pharmaceutical ingredients (APIs) and other sensitive materials. Additionally, the systems are employed in the agricultural industry for handling fertilizers and seeds, as well as in the mining industry for transporting ore powders.
Customization and Scalability of Pneumatic Conveying Solutions
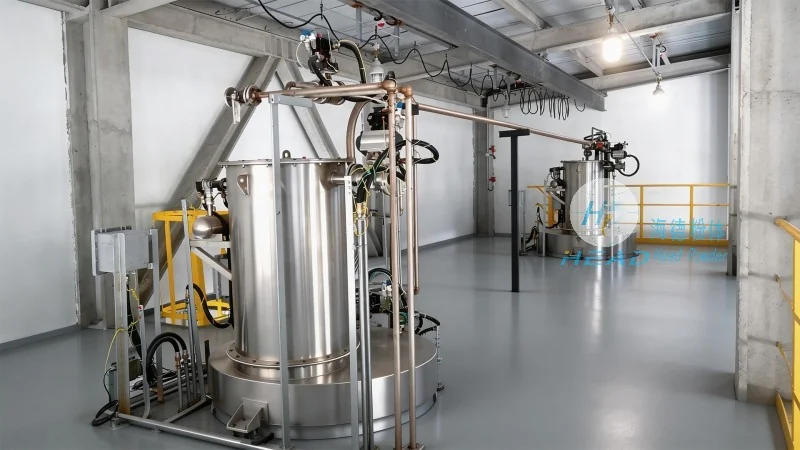
HeadPowder understands that each client has unique requirements, which is why they offer customized pneumatic conveying solutions tailored to specific needs. Whether it's a small-scale system for a laboratory or a large-scale system for an industrial plant, the company provides comprehensive design and engineering services. The systems can be scaled up or down based on the volume of powder to be transported, and can be integrated with existing facilities or new installations. This flexibility ensures that clients receive a solution that meets their exact specifications and operational goals.
Conclusion: The Role of Pneumatic Conveying Systems in Modern Powder Handling
In conclusion, pneumatic conveying systems for powders are a critical technology in modern industrial operations. They offer a reliable, efficient, and safe method for transporting bulk powders, reducing downtime and operational costs. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can implement advanced powder handling solutions that enhance productivity and meet industry standards. As the demand for efficient and sustainable powder handling increases, the role of pneumatic conveying systems will continue to grow, making them an essential component of industrial infrastructure.