

Introduction to Coal Ash Conveying Systems: Advantages of Coal Ash Pneumatic Conveying
Coal ash, a byproduct of coal combustion in power plants, presents significant challenges for transportation and disposal. Traditional methods such as trucking or belt conveyors often encounter issues like dust pollution, material degradation, and operational inefficiencies. To address these challenges, advanced coal ash conveying systems have emerged, with pneumatic conveying being a leading solution. This article provides an overview of coal ash conveying systems, focusing on the advantages and features of pneumatic conveying technology, while highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. as a key player in this field.
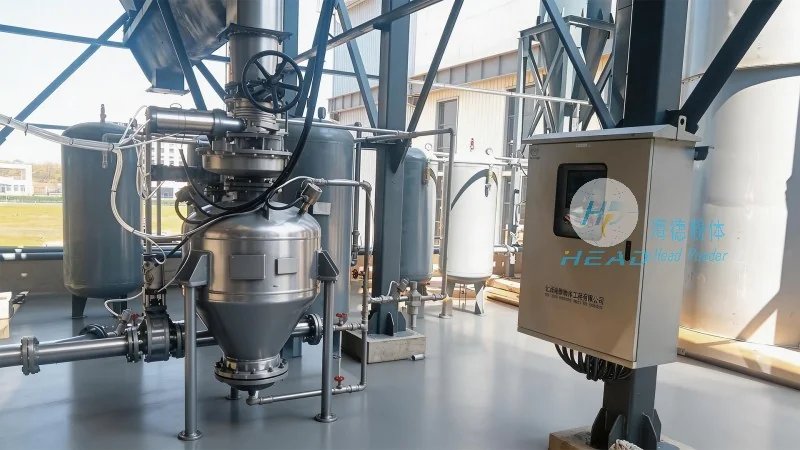
HeadPowder: Your Expert in Coal Ash Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in Shandong, China, specializing in the design, manufacturing, and implementation of coal ash handling systems. With years of experience in the power industry, HeadPowder has developed a comprehensive range of solutions tailored to the unique needs of coal ash transportation. The company's commitment to innovation and quality ensures that clients receive reliable and efficient systems that meet industry standards and environmental regulations.
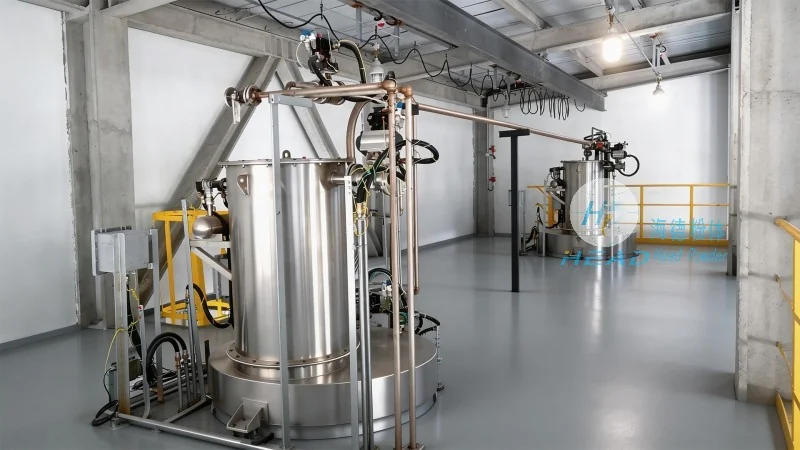
Key Features of Pneumatic Conveying for Coal Ash
Pneumatic conveying, also known as air conveying, utilizes air pressure to transport bulk materials like coal ash through a pipeline. This technology offers several advantages over traditional methods. First, it provides a dust-free environment, reducing the risk of respiratory issues and environmental contamination. Second, it enables the transportation of materials over long distances without the need for intermediate storage or transfer points. Third, the system is highly flexible, allowing integration of multiple sources and destinations within a single network. Additionally, pneumatic conveying systems can handle a wide range of ash compositions, including fly ash and bottom ash, with minimal degradation of the material.
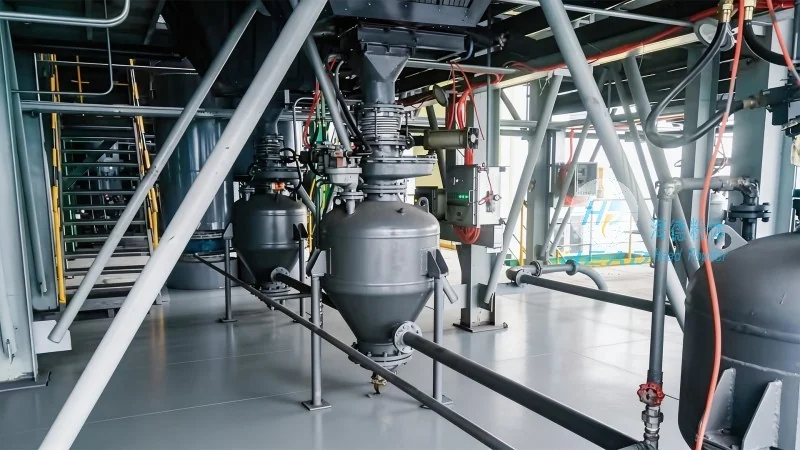
Advantages of Pneumatic Conveying in Coal Ash Transport
The adoption of pneumatic conveying for coal ash transport brings numerous benefits. One primary advantage is reduced operational costs. By eliminating the need for heavy machinery and labor-intensive manual handling, companies achieve significant savings in both time and resources. Furthermore, the system enhances safety by minimizing human exposure to dust and hazardous materials. Environmental benefits are substantial, as the enclosed pipeline system prevents ash from being released into the atmosphere, thereby reducing air pollution and complying with stringent environmental regulations. Another key advantage is improved material quality, as the conveying process preserves the physical and chemical properties of the coal ash, crucial for its subsequent use in construction materials or other industrial applications.
Technical Specifications and Application Scenarios
HeadPowder's coal ash pneumatic conveying systems are designed with precision, incorporating advanced components such as high-efficiency blowers, flexible hoses, and robust pipeline networks. The systems are available in various configurations, including positive and negative pressure modes, to suit different operational requirements. For instance, positive pressure systems are ideal for short-distance transport, while negative pressure systems are suitable for longer distances or when the ash needs to be transported from multiple sources to a central disposal or utilization site. The company's engineers work closely with clients to assess specific site conditions, ash characteristics, and operational goals to design customized solutions that optimize performance and cost-effectiveness.
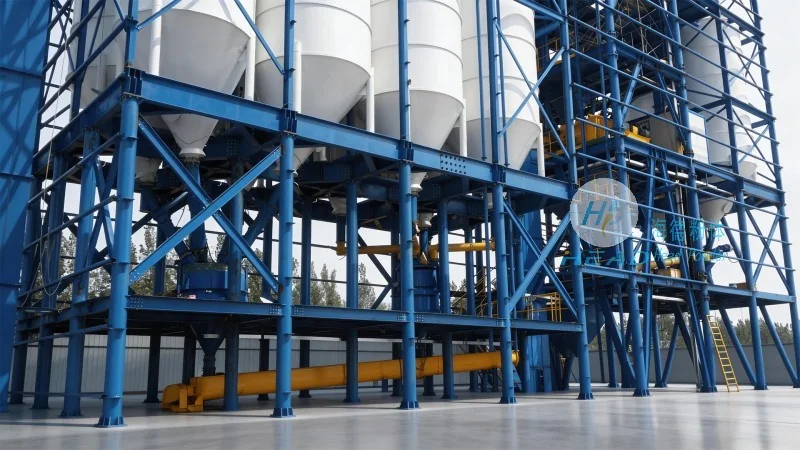
Conclusion
In conclusion, coal ash conveying systems, particularly those utilizing pneumatic conveying technology, represent a modern and efficient approach to handling coal ash. The advantages of this method, including dust control, cost reduction, and environmental compliance, make it a preferred choice for power plants and industrial facilities. Shandong HeadPowder Engineering Co., Ltd. stands out as a trusted partner in providing these advanced systems, leveraging its expertise and innovative solutions to meet the evolving needs of the industry. By investing in such systems, companies can enhance operational efficiency, ensure environmental responsibility, and contribute to sustainable development in the power sector.