

[Magnesium Sulfate Heptahydrate Pneumatic Conveying System: The Intelligent and Efficient New Era fo
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced material handling solutions. The company, commonly known as headpowder, leverages its extensive industry experience to deliver high-performance systems tailored to the unique needs of various industrial applications.
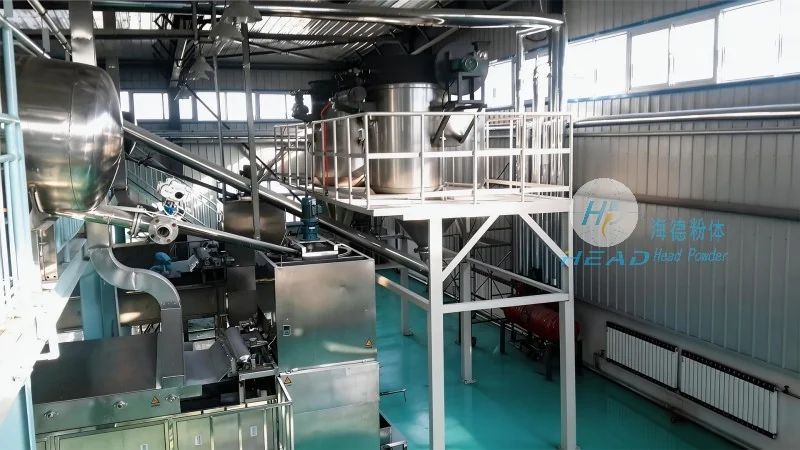
Introducing the Magnesium Sulfate Heptahydrate Pneumatic Conveying System
The Magnesium Sulfate Heptahydrate Pneumatic Conveying System represents a cutting-edge solution for the efficient and reliable transportation of magnesium sulfate heptahydrate. This system is engineered to address the challenges associated with handling bulk materials, ensuring minimal product loss, reduced labor costs, and enhanced operational safety. By integrating advanced pneumatic conveying technology with intelligent control systems, the system optimizes the entire material handling process from source to destination.
Key Features and Advantages of the System
At the core of the Magnesium Sulfate Heptahydrate Pneumatic Conveying System are several key features that set it apart from traditional conveying methods. Firstly, the system employs a closed-loop pneumatic design, which significantly minimizes dust generation and environmental contamination. This is particularly crucial for handling magnesium sulfate heptahydrate, a material that requires strict adherence to hygiene and safety standards. Secondly, the intelligent control module allows for real-time monitoring and adjustment of conveying parameters, ensuring consistent material flow and preventing system overloads or blockages.
Another notable advantage is the system's adaptability to different operational conditions. Whether dealing with varying material moisture levels or fluctuating production volumes, the system can be configured to maintain optimal performance. The use of high-quality materials in the construction of the conveying lines and components ensures durability and long-term reliability, reducing maintenance requirements and overall operational costs. Additionally, the system's modular design facilitates easy integration with existing production lines, minimizing downtime during installation and commissioning.
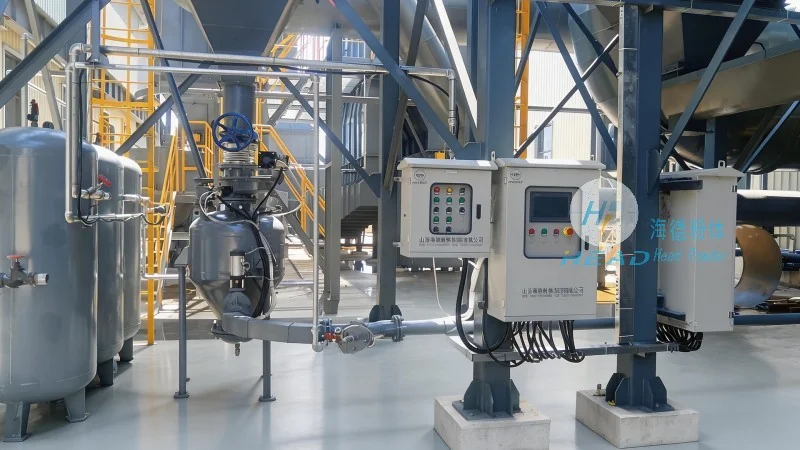
Enhanced Efficiency and Cost Savings
By implementing the Magnesium Sulfate Heptahydrate Pneumatic Conveying System, industries can achieve substantial improvements in operational efficiency and cost savings. Traditional methods of transporting bulk materials, such as bucket elevators or belt conveyors, often suffer from high maintenance costs and frequent breakdowns. In contrast, pneumatic conveying systems offer a more seamless and continuous material flow, reducing the need for manual intervention and associated labor expenses. The system's ability to handle materials at high speeds and over longer distances without the need for intermediate storage points further enhances overall productivity.
Furthermore, the intelligent control system enables predictive maintenance, allowing for proactive identification and resolution of potential issues before they lead to system failures. This not only minimizes unexpected downtime but also extends the lifespan of the equipment. The reduced product loss due to the system's enclosed design also contributes to significant cost savings, as less material is wasted during transportation. Overall, the Magnesium Sulfate Heptahydrate Pneumatic Conveying System provides a comprehensive solution that aligns with modern industrial demands for efficiency, sustainability, and cost-effectiveness.
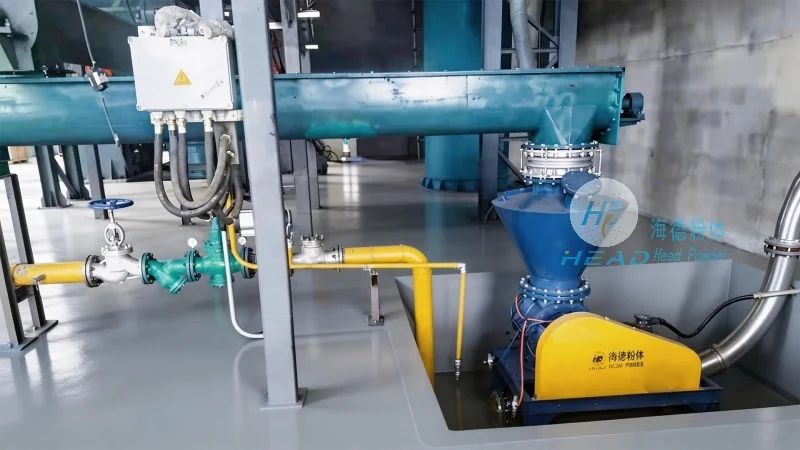
Application and Industry Impact
The Magnesium Sulfate Heptahydrate Pneumatic Conveying System is particularly well-suited for industries that rely on the consistent and reliable supply of magnesium sulfate heptahydrate, such as pharmaceuticals, agriculture, and chemical manufacturing. In these sectors, the material's purity and quality are paramount, and the system's ability to maintain these standards throughout the conveying process is critical. The system's design ensures that the material remains free from contamination, preserving its chemical integrity and meeting stringent regulatory requirements.
For agricultural applications, the system facilitates the efficient distribution of magnesium sulfate heptahydrate as a fertilizer or soil amendment, improving crop yields and soil health. In the pharmaceutical industry, the system's hygienic design and minimal product exposure make it ideal for handling active pharmaceutical ingredients (APIs) and other sensitive materials. The chemical manufacturing sector benefits from the system's ability to handle bulk quantities of magnesium sulfate heptahydrate, supporting large-scale production processes with minimal interruptions.
Conclusion and Future Outlook
Shandong HeadPowder Engineering Co., Ltd. continues to innovate and advance its material handling solutions, with the Magnesium Sulfate Heptahydrate Pneumatic Conveying System being a prime example of its commitment to excellence. By combining advanced technology with practical engineering, the company provides industries with a reliable and efficient solution for transporting magnesium sulfate heptahydrate. As the demand for high-quality material handling systems grows, the system's intelligent and efficient design positions it as a leading choice for businesses seeking to optimize their operations and enhance their competitive edge. With its proven performance and adaptability, the Magnesium Sulfate Heptahydrate Pneumatic Conveying System is set to play a vital role in the future of industrial material handling.