Understanding the various types, key features, and practical application ranges of corn kernel pneumatic conveying systems is crucial for industries dealing with bulk material handling. This article explores the different configurations, technical advantages, and operational contexts where these systems are effectively utilized, providing insights into their role in enhancing efficiency and reliability in material transport.
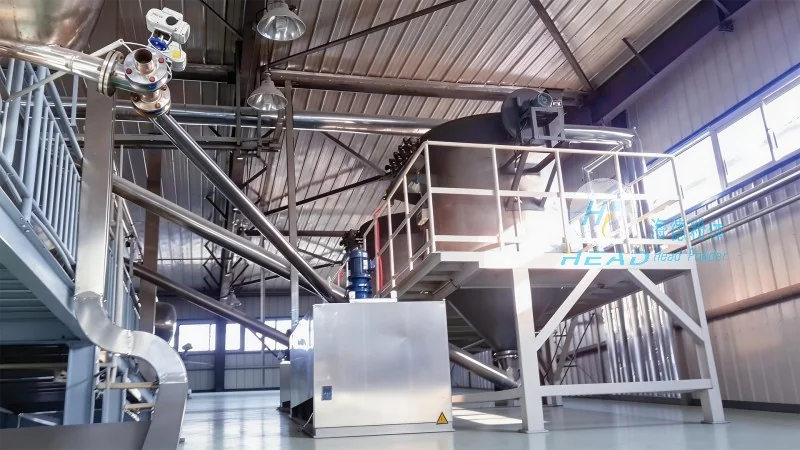
Overview of Corn Kernel Pneumatic Conveying Systems
Corn kernel pneumatic conveying systems are engineered to transport bulk solid materials, such as corn kernels, through a pressurized or vacuumed air stream. These systems are widely adopted in agricultural processing, food manufacturing, and related industries due to their ability to handle large volumes of material with minimal mechanical contact. The core components typically include a hopper for material storage, a conveyor line (often a flexible or rigid tube), a fan or blower to generate the air flow, and a receiver or discharge point for the material. The design of these systems can vary significantly based on the specific requirements of the application, including the size of the corn kernels, the distance to be conveyed, and the desired throughput.
Different Types of Pneumatic Conveying Systems for Corn Kernels
There are primarily two main categories of pneumatic conveying systems used for corn kernels: pressure systems and vacuum systems. Each type has distinct characteristics and is suited to different operational scenarios.
Pressure systems operate by forcing air and material through a closed pipeline under positive pressure. These systems are generally more suitable for conveying materials over longer distances or against gravity. They typically feature a positive displacement blower or a centrifugal fan that generates the necessary pressure. The material is introduced into the system at the inlet, where it is mixed with the air stream and propelled forward. Pressure systems are often preferred for applications requiring high throughput and the ability to handle abrasive or sticky materials like corn kernels.
Vacuum systems, on the other hand, create a negative pressure environment that draws material from the source into the pipeline. These systems are ideal for short-distance conveying or when the material needs to be collected from multiple points. They utilize a vacuum pump to create the suction force, and the material is drawn into the system through a hopper or collection point. Vacuum systems are commonly used in applications where the material is to be transported from a lower elevation to a higher one or when the material is sensitive to pressure changes.
Key Features and Technical Advantages of Corn Kernel Pneumatic Conveying
Several key features distinguish effective corn kernel pneumatic conveying systems, contributing to their efficiency and reliability in industrial settings.
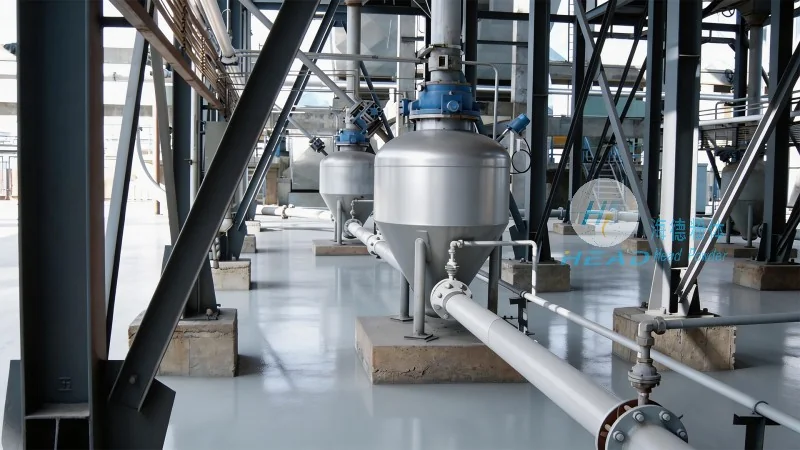
Firstly, the system's ability to handle varying particle sizes and densities is a critical feature. Corn kernels can vary in size and density, and a well-designed pneumatic conveying system must accommodate these variations without causing blockages or excessive wear on components. Advanced systems often incorporate adjustable air flow rates and material feed mechanisms to maintain consistent performance under different operating conditions.
Secondly, the system's energy efficiency is a significant advantage. Modern pneumatic conveying systems utilize high-efficiency fans and blowers that minimize energy consumption while maintaining the required air pressure and flow rates. This not only reduces operational costs but also aligns with sustainability goals in industrial operations.
Thirdly, the system's ability to prevent material degradation is an important technical feature. Corn kernels are susceptible to moisture and temperature changes, which can affect their quality and usability. Pneumatic conveying systems can be designed with insulated pipelines and controlled air temperatures to minimize exposure to environmental factors, preserving the integrity of the material during transport.
Additionally, the system's flexibility in terms of layout and integration with existing infrastructure is a valuable feature. Pneumatic conveying systems can be configured in various shapes and sizes to fit within existing plant layouts, and they can be easily integrated with other processing equipment, such as cleaning, drying, or packaging machinery. This adaptability makes them a versatile solution for diverse industrial applications.
Application Ranges of Corn Kernel Pneumatic Conveying Systems
The application ranges of corn kernel pneumatic conveying systems are broad and cover various stages of corn processing and handling. These systems are commonly used in the following contexts:
In agricultural processing facilities, pneumatic conveying systems are used to transport corn kernels from storage silos to processing lines, such as grinding, milling, or flaking operations. The ability to handle large volumes of material quickly and efficiently supports high production rates in these facilities. The systems are also used to move processed corn products, such as cornmeal or corn flour, between different processing stages or to storage silos for distribution.
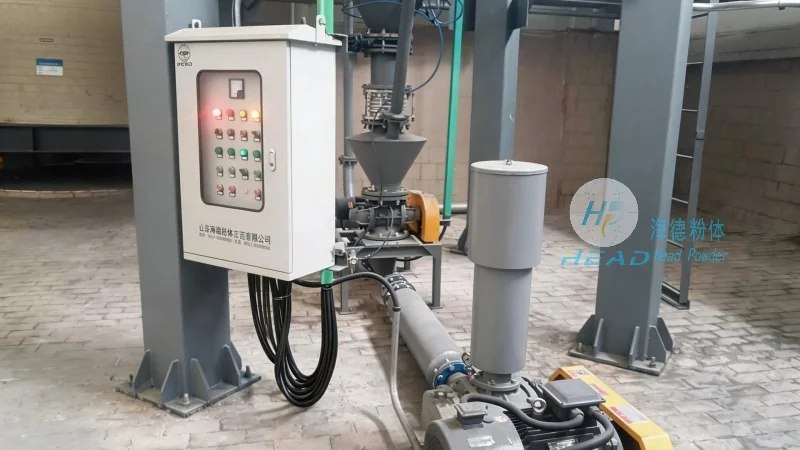
In food manufacturing plants, pneumatic conveying systems are employed to transport corn kernels and other ingredients to mixing and blending equipment. This ensures a consistent and uniform mixture of ingredients, which is essential for producing high-quality food products. The systems are also used to convey finished products, such as corn-based snacks or cereals, from production lines to packaging areas.
In grain storage and handling operations, pneumatic conveying systems are used to move corn kernels from storage bins to processing facilities or to transport them between different storage locations. This facilitates efficient inventory management and ensures that the material is moved in a controlled manner, reducing the risk of spoilage or damage.
In addition, pneumatic conveying systems are used in research and development facilities to transport and test different types of corn kernels under various conditions. This allows researchers to study the properties of corn kernels and develop new processing techniques or products.
Conclusion and Company Introduction
Corn kernel pneumatic conveying systems offer a reliable and efficient solution for handling bulk corn kernels in various industrial applications. The different types of systems—pressure and vacuum—provide flexibility to meet diverse operational requirements, while key features such as adjustable air flow, energy efficiency, and material protection enhance their performance and sustainability. The application ranges of these systems span from agricultural processing to food manufacturing and storage, supporting the entire lifecycle of corn handling.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying systems, specializes in designing and supplying customized solutions for corn kernel and other bulk material handling needs. With a focus on innovation and quality, HeadPowder provides systems that meet the specific requirements of its clients, ensuring optimal performance and reliability. The company's headquarters is located in Shandong, China, where it leverages advanced technology and expertise to deliver cutting-edge solutions for the agricultural and food processing industries.




