

What is a Dust Removal Coke Powder Material Pneumatic Conveying Equipment? What is its Design Princi
For industrial facilities dealing with coke powder, an efficient and reliable material handling solution is crucial. The dust removal coke powder pneumatic conveying equipment, developed by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated method to transport these fine materials while ensuring environmental compliance and operational efficiency. This equipment is designed to handle the unique challenges associated with coke powder, such as its fine particle size, potential dust generation, and the need for dust control during transport.
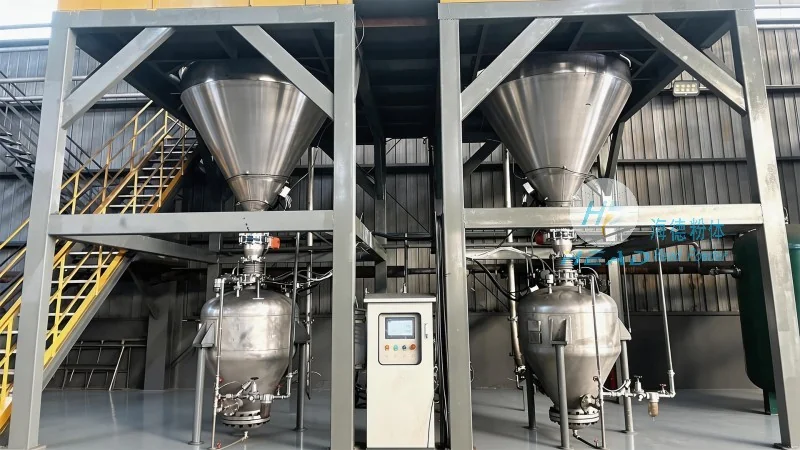
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer in the field of material handling equipment, specializing in pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring advanced solutions for powder and bulk material transport. HeadPowder's expertise lies in designing equipment that meets the specific demands of clients, ensuring durability, performance, and compliance with industry standards. The company's headquarters is located in Shandong, China, where it operates its research and development, manufacturing, and customer support facilities.
What is Dust Removal Coke Powder Pneumatic Conveying Equipment?
Dust removal coke powder pneumatic conveying equipment is a system that uses air pressure to transport coke powder from one location to another. Unlike traditional mechanical conveyors, this equipment relies on the principle of pneumatic transport, where the material is suspended in a stream of air and moved through a pipeline. The system is equipped with dust removal mechanisms to capture and filter the fine particles, preventing environmental contamination and ensuring a clean operation. This equipment is particularly suitable for applications where coke powder needs to be transported over long distances or through complex layouts, while maintaining low dust emissions.
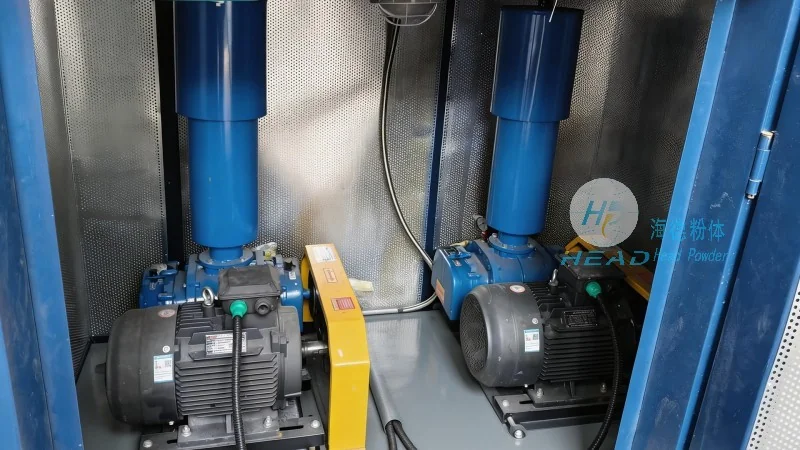
Key Components and Their Functions
The dust removal coke powder pneumatic conveying equipment consists of several key components, each playing a vital role in the overall operation. The main components include the material feed hopper, the air compressor, the conveying pipeline, the dust filter system, and the control panel. The material feed hopper is responsible for storing and feeding the coke powder into the system, ensuring a consistent flow of material. The air compressor generates the necessary air pressure to move the material through the pipeline. The conveying pipeline is designed to withstand the pressure and material flow, with appropriate fittings and valves to control the direction and speed of transport. The dust filter system is a critical component that captures the fine particles, preventing them from being released into the environment. The control panel allows operators to monitor and adjust the system parameters, ensuring optimal performance and safety.
Design Principle of the Equipment
The design principle of the dust removal coke powder pneumatic conveying equipment is based on the fundamental laws of fluid dynamics and material transport. The system operates on the principle of pneumatic conveying, where the material is suspended in a stream of air and transported through the pipeline. The key design considerations include the air velocity, which must be sufficient to keep the material suspended but not so high as to cause excessive pressure drop or wear on the equipment. The pipeline diameter and length are also critical factors, as they affect the pressure drop and the overall efficiency of the system. The dust removal system is designed to capture the fine particles, using filters and cyclones to separate the material from the air. The system is also equipped with safety features, such as pressure relief valves and emergency shut-off mechanisms, to prevent accidents and ensure safe operation.
Advantages of Using Dust Removal Coke Powder Pneumatic Conveying Equipment
There are several advantages to using dust removal coke powder pneumatic conveying equipment in industrial applications. First, the equipment is highly efficient in transporting coke powder, with minimal material loss and low energy consumption. Second, the dust removal system ensures that the operation is environmentally friendly, with low emissions of fine particles. Third, the equipment is flexible and can be adapted to various applications, including long-distance transport and complex layouts. Fourth, the system is relatively low maintenance, with easy access to components for inspection and replacement. Finally, the equipment is designed to meet the specific needs of clients, ensuring that it operates optimally in their particular environment.
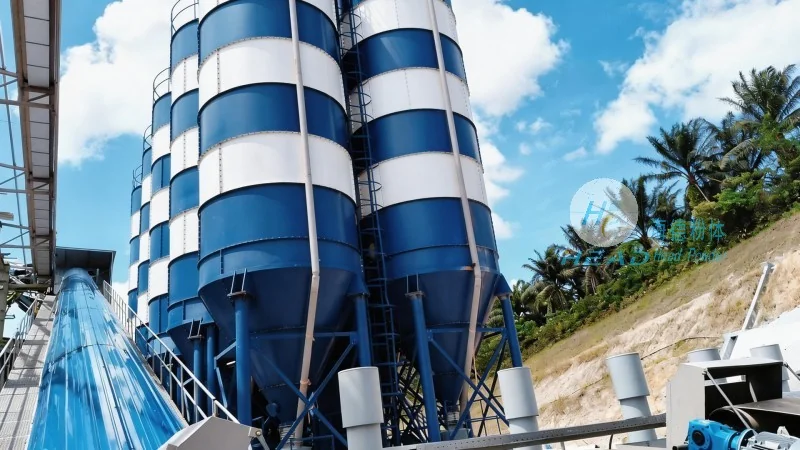
Applications and Industries
The dust removal coke powder pneumatic conveying equipment is widely used in various industries that handle coke powder, including steel manufacturing, power generation, and chemical processing. In steel plants, the equipment is used to transport coke from storage silos to the blast furnace, ensuring a continuous supply of raw material. In power plants, the equipment is used to transport coke to the boiler, where it is burned to generate electricity. In chemical plants, the equipment is used to transport coke powder to various processing units, such as reactors and mixers. The equipment is also used in other industries, such as food processing and pharmaceuticals, where fine powders need to be transported in a clean and efficient manner.
Conclusion
Dust removal coke powder pneumatic conveying equipment is an essential component for industrial facilities dealing with coke powder. The equipment, developed by Shandong HeadPowder Engineering Co., Ltd., offers a reliable and efficient solution for transporting these fine materials while ensuring environmental compliance and operational efficiency. With its advanced design and dust removal capabilities, the equipment is suitable for various applications and industries, making it a valuable asset for any facility requiring bulk material handling. By choosing this equipment, clients can improve their operational efficiency, reduce costs, and ensure a safe and clean working environment.