Shandong HeadPowder Engineering Co., Ltd., often referred to as HeadPowder, is a leading provider of specialized pneumatic conveying systems tailored for the fine chemicals industry. The company, based in Shandong, China, focuses on delivering high-quality solutions that address the unique challenges of handling delicate, sensitive, and often hazardous materials. These systems are engineered to maintain product integrity, ensure operational efficiency, and comply with stringent industry standards, making them essential for modern chemical processing facilities.
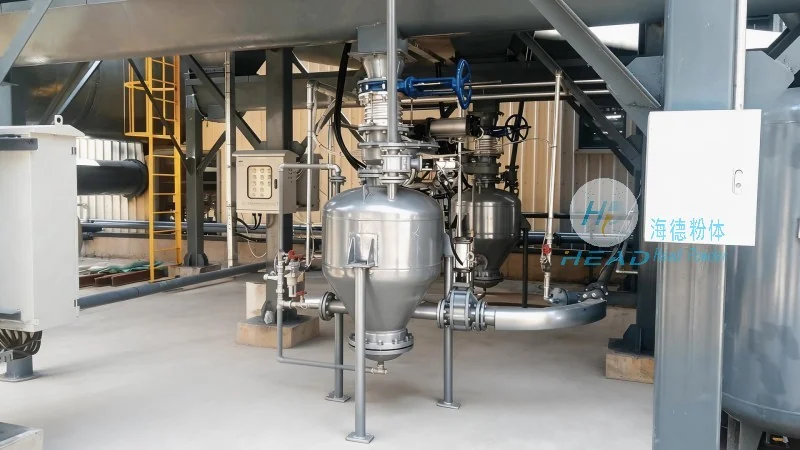
Working Principle of Pneumatic Conveying Systems
The fundamental operation of a pneumatic conveying system revolves around the use of air pressure or vacuum to transport bulk materials through a pipeline. In positive pressure systems, compressed air is introduced into the pipeline, creating a flow that lifts and carries the material particles. The process begins with a material feed hopper, which holds the bulk material. A rotary airlock valve, positioned at the hopper outlet, controls the material flow into the pipeline, preventing air from escaping back into the hopper. As the air travels through the pipeline at a controlled velocity, it transports the material to the receiving hopper or silo at the destination. The receiving hopper collects the material, and the air is then filtered and discharged. Negative pressure systems, on the other hand, utilize suction to draw material from the source into the pipeline. This method is particularly advantageous for applications requiring material to be moved from a higher elevation to a lower one or when handling dusty or hazardous materials, as it reduces the risk of dust dispersion and exposure.
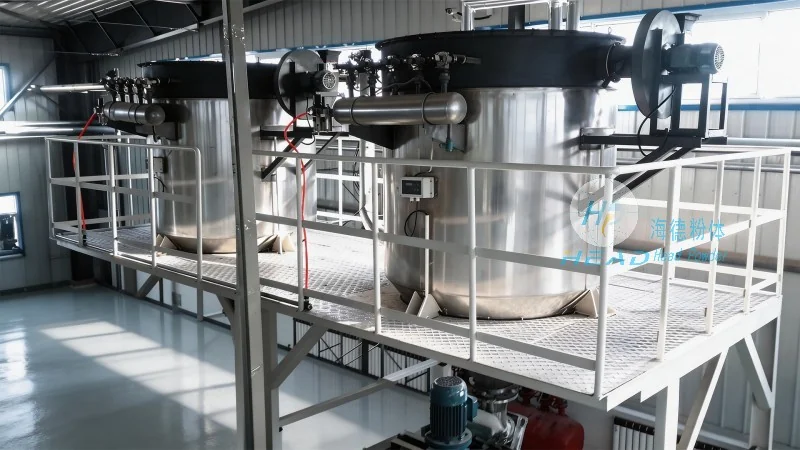
Key Features of Fine Chemicals Pneumatic Conveying Systems
Systems designed for fine chemicals incorporate several critical features that distinguish them from standard bulk handling equipment. Firstly, the construction materials are chosen for their chemical inertness and non-reactivity, such as stainless steel or specialized alloys, to prevent contamination of the processed chemicals. The components are also designed with smooth, non-porous surfaces to minimize material buildup and reduce the risk of clogging, which is crucial for fine powders that can adhere to surfaces. Advanced control mechanisms, including variable frequency drives (VFDs) for air flow regulation and pressure sensors for real-time monitoring, enable precise control over the conveying rate. This ensures consistent material flow, preventing overloading or underloading of the pipeline and maintaining system stability. Additionally, integrated dust collection and filtration systems capture and neutralize airborne particles, maintaining a clean and safe working environment. Safety interlocks and emergency shut-off valves are also standard features, providing protection against accidents and ensuring equipment and personnel safety.
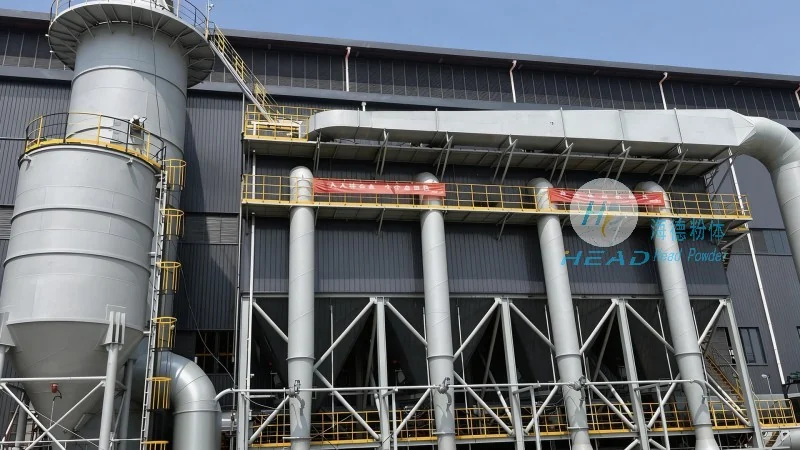
Advantages and Practical Applications
The implementation of pneumatic conveying systems in the fine chemicals industry offers significant advantages, including enhanced product quality, operational efficiency, and safety. Unlike mechanical conveyors, which can cause particle attrition and size reduction, pneumatic systems minimize physical stress on the material, preserving its integrity and ensuring that the final product meets the required specifications. This is particularly important for sensitive materials, such as pharmaceuticals, food additives, and specialty chemicals, where particle size and purity are critical. The enclosed and hygienic design of these systems facilitates compliance with regulatory standards like GMP (Good Manufacturing Practice), reducing the risk of contamination and ensuring product safety. Furthermore, the flexibility of pneumatic systems allows for easy integration with existing production lines and scalability as production needs change. They can handle a wide range of material types, from fine powders to granules, making them suitable for various applications, including material transfer between reactors, storage silos, and packaging lines. By optimizing material flow and reducing downtime, these systems contribute to increased productivity and cost savings for manufacturers in the fine chemicals sector.




