For industrial applications involving the handling of rice husk ash, efficient and reliable material transport is crucial. The pneumatic conveying system, specifically designed for rice husk ash, offers a sophisticated solution that addresses the unique challenges associated with this material. This article explores the working principle and key features of such a system, highlighting its advantages and practical applications.
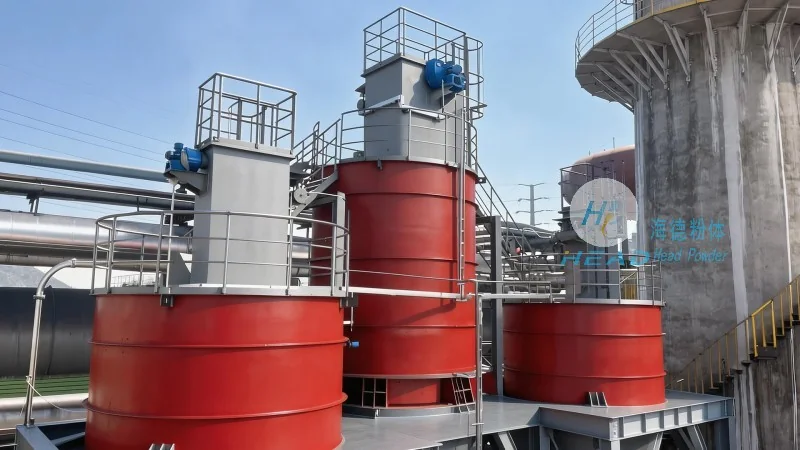
Introduction to the Rice Husk Ash Pneumatic Conveying System
The system is engineered by Shandong HeadPowder Engineering Co., Ltd., a leading company based in China, specializing in advanced material handling solutions. The company's expertise in pneumatic conveying technology ensures that the system is tailored to meet the specific demands of rice husk ash, which is known for its light weight, abrasive properties, and potential for dust generation. By leveraging the company's technical prowess, the system provides a seamless and efficient method for transporting this material from source to destination.
Working Principle of the Pneumatic Conveying System
The core mechanism of the rice husk ash pneumatic conveying system revolves around the use of air to transport the material. The system operates by creating a pressure differential, either through suction or pressure, to move the rice husk ash particles through a pipeline. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. As air is introduced, it creates a flow that carries the ash particles along the pipeline. The system utilizes various components, including a blower or compressor, a hopper, a feeder, and a receiver, to ensure smooth and continuous transport. The air velocity is carefully controlled to maintain the material in a suspended state, preventing blockages and ensuring consistent flow rates. The system's design allows for the efficient transport of rice husk ash over varying distances, making it suitable for both short and long-range applications.
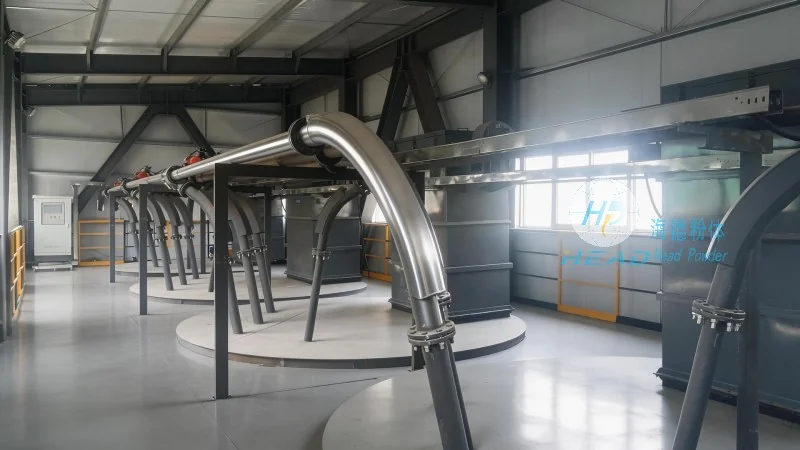
Key Features and Advantages of the System
The rice husk ash pneumatic conveying system by Shandong HeadPowder Engineering Co., Ltd. is characterized by several key features that enhance its performance and reliability. One of the primary advantages is its ability to handle the abrasive nature of rice husk ash without causing significant wear to the system components. The system incorporates durable materials, such as high-quality stainless steel or specialized coatings, to withstand the abrasive effects of the material over extended periods. Additionally, the system is designed to minimize dust generation, which is a critical concern in industrial settings. By using efficient filtration and sealing mechanisms, the system reduces the risk of dust contamination and ensures a cleaner working environment. Another notable feature is the system's flexibility, allowing for easy integration with existing industrial processes. The modular design enables customization to fit specific operational requirements, including varying material flow rates and pipeline configurations. The system also offers energy efficiency, with optimized air usage that reduces operational costs while maintaining high transport efficiency. Furthermore, the system is equipped with advanced monitoring and control systems, providing real-time data on flow rates, pressure, and material levels. This allows for proactive maintenance and ensures optimal performance at all times.
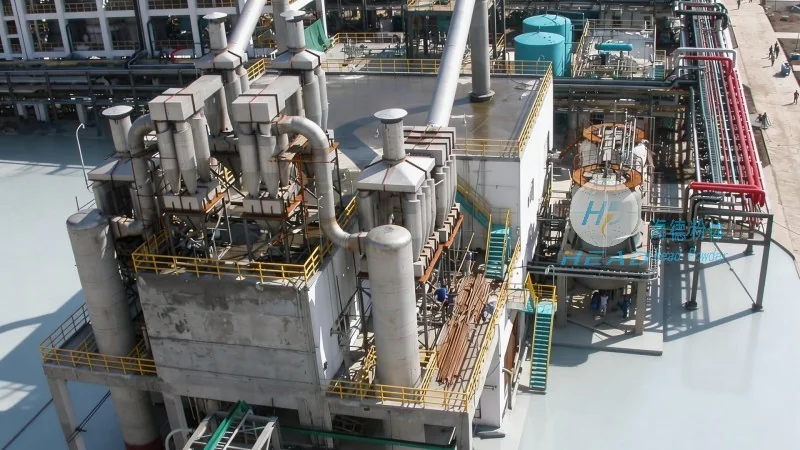
Applications and Industrial Use Cases
The rice husk ash pneumatic conveying system finds extensive application in various industrial sectors where rice husk ash is a byproduct or raw material. In the power generation industry, for instance, rice husk ash is often used as a fuel or additive in boilers. The system efficiently transports the ash from the combustion chamber to storage or processing facilities, ensuring a continuous supply for energy production. In the construction industry, rice husk ash is utilized as a raw material in the production of cement and concrete. The system facilitates the transport of ash from storage to mixing plants, contributing to the efficient manufacturing of building materials. Additionally, the system is employed in agricultural applications, where rice husk ash is used as a soil amendment or fertilizer. The ability to transport the material over long distances makes it suitable for large-scale agricultural operations. The system's adaptability also makes it suitable for research and development facilities, where precise handling of rice husk ash is required for experimental purposes.
Conclusion and Company Overview
In conclusion, the rice husk ash pneumatic conveying system by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and reliable solution for the efficient handling of rice husk ash. The system's working principle, based on pneumatic transport, ensures smooth and continuous material movement, while its key features, such as durability, dust control, and flexibility, address the unique challenges associated with this material. The company's expertise in engineering and manufacturing ensures that the system meets the highest standards of performance and reliability. As a leading provider of material handling solutions, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide tailored systems that enhance operational efficiency and reduce costs for its clients. The system's application in various industries highlights its versatility and importance in modern industrial processes.




