Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in bulk material handling solutions. Our white powder bulk material conveyors are designed to efficiently transport various white powders, including but not limited to industrial chemicals, food additives, and pharmaceutical powders. This article will explore the working principle and key features of these conveyors, providing insights into their functionality and advantages.
Introduction to White Powder Bulk Material Conveyors
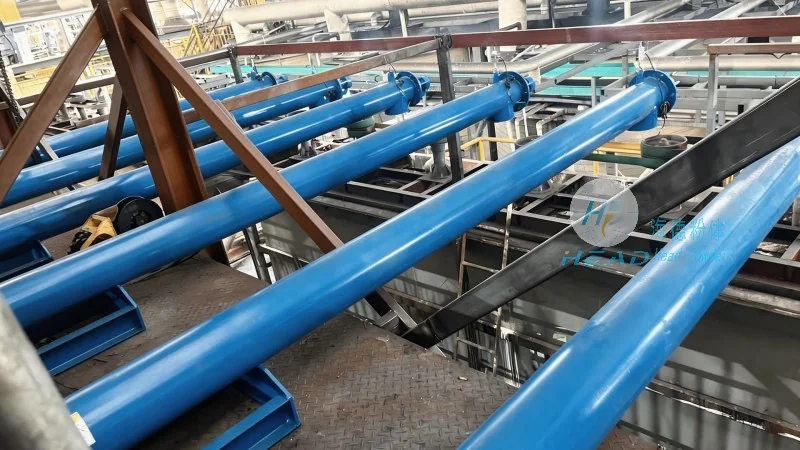
White powder bulk material conveyors are essential equipment in industries that rely on the transportation of fine powders. These systems are engineered to handle materials with specific characteristics, such as low bulk density, high dustiness, and sensitivity to moisture. The design of these conveyors addresses the unique challenges associated with white powders, ensuring reliable and efficient material movement from source to destination.
Working Principle of White Powder Bulk Material Conveyors
The working principle of white powder bulk material conveyors typically involves a combination of mechanical components working in tandem to move the powder. The primary mechanism often includes a screw or auger that rotates within a closed tube, creating a positive pressure that propels the material forward. As the screw rotates, it pushes the powder along the conveyor's path, maintaining a consistent flow rate. The system may also incorporate a hopper at the inlet to store the material and a discharge outlet at the end for delivery. Some models utilize a vacuum or pressure system to enhance the conveying process, especially for materials that are light or have poor flow characteristics. The control system, often integrated with sensors, monitors the flow rate and adjusts the motor speed as needed to maintain optimal performance. This dynamic adjustment ensures that the conveyor operates efficiently under varying load conditions, preventing clogging or overloading.
Key Features of White Powder Bulk Material Conveyors
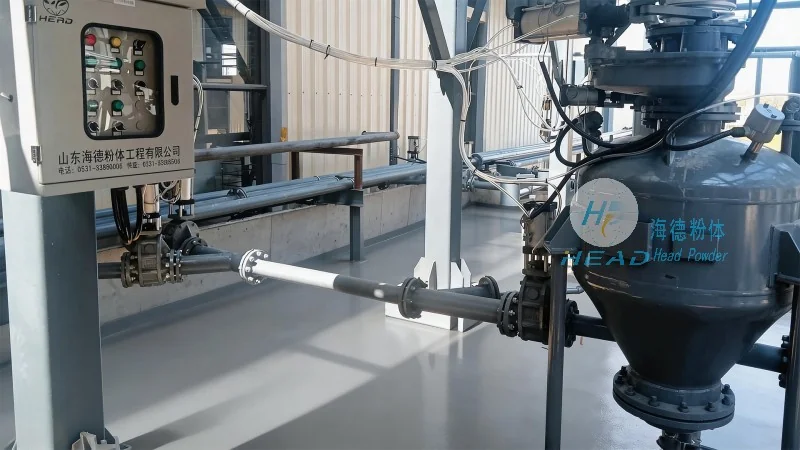
White powder bulk material conveyors from Shandong HeadPowder Engineering Co., Ltd. are equipped with several key features that enhance their performance and reliability. One of the most notable features is the use of high-quality, food-grade or industrial-grade materials for the conveyor components, ensuring compatibility with a wide range of white powders. The design incorporates smooth, non-stick surfaces to minimize material buildup and reduce the risk of contamination. Additionally, the conveyors are equipped with dust collection systems to maintain a clean working environment and comply with industrial safety standards. The modular construction allows for easy maintenance and replacement of parts, reducing downtime and operational costs. Advanced control systems with real-time monitoring capabilities provide operators with insights into the conveyor's performance, enabling proactive maintenance and troubleshooting. The conveyors are also designed for easy integration into existing production lines, with adjustable inlet and outlet configurations to accommodate different processing requirements. This flexibility makes them suitable for various applications, from small-scale laboratory use to large-scale industrial production.
Advantages of Using White Powder Bulk Material Conveyors
Implementing white powder bulk material conveyors offers several advantages for businesses in need of efficient powder handling solutions. The primary advantage is the significant reduction in labor costs associated with manual handling of powders. By automating the conveying process, companies can minimize the risk of human error and improve overall operational efficiency. The conveyors also help maintain consistent material quality by preventing contamination and ensuring uniform flow rates. This consistency is crucial in industries where material purity directly impacts product quality, such as pharmaceuticals and food processing. Furthermore, the energy-efficient design of these conveyors reduces operational costs over time, making them a cost-effective investment for long-term use. The compact design of many models allows for space-saving installation, which is particularly beneficial in facilities with limited floor space. The durability of the components, combined with regular maintenance, ensures a long service life, providing a reliable solution for bulk material transportation.
Applications and Industries
White powder bulk material conveyors are widely used across various industries due to their versatility and effectiveness. In the chemical industry, they are used to transport white powders like calcium carbonate, titanium dioxide, and other industrial chemicals. The food and beverage industry utilizes these conveyors for handling food additives, such as sugar, starch, and flavorings. The pharmaceutical sector relies on them to transport active pharmaceutical ingredients (APIs) and excipients, ensuring strict adherence to hygiene and safety standards. Additionally, the cosmetics industry uses white powder conveyors for transporting ingredients like talc, silica, and other fine powders used in skincare and beauty products. These applications highlight the importance of reliable and efficient powder handling in maintaining product quality and meeting industry regulations.
Maintenance and Operational Tips
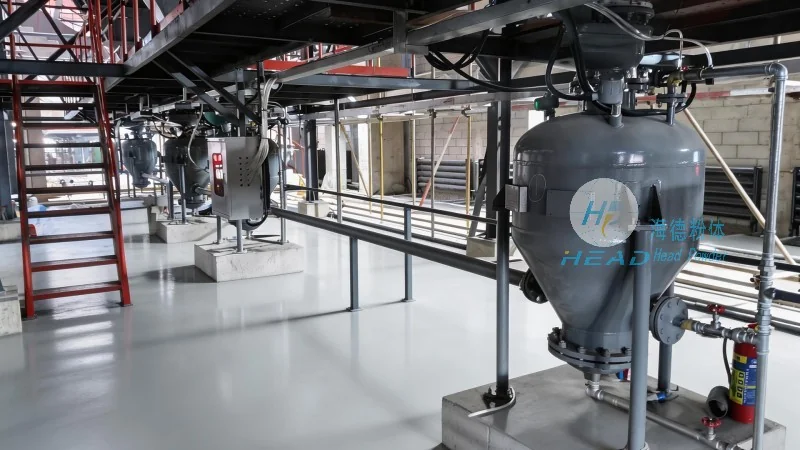
Proper maintenance is essential to ensure the longevity and optimal performance of white powder bulk material conveyors. Regular inspection of the screw and auger components is crucial to detect any signs of wear or damage. Cleaning the conveyor system after each use, especially for materials prone to clogging, helps prevent material buildup and maintains smooth operation. The dust collection system should be checked regularly to ensure it is functioning correctly and capturing all airborne particles. Lubrication of moving parts, as recommended by the manufacturer, is vital to reduce friction and extend the life of the components. Operators should also monitor the motor temperature and sound during operation, as abnormal conditions may indicate a problem that requires immediate attention. Following the manufacturer's guidelines for maintenance and operational procedures ensures that the conveyor operates at its best, minimizing downtime and maximizing productivity.
Conclusion
White powder bulk material conveyors from Shandong HeadPowder Engineering Co., Ltd. represent a reliable and efficient solution for transporting white powders in various industrial applications. Their working principle, based on mechanical propulsion and advanced control systems, ensures consistent and reliable material movement. The key features, including high-quality materials, dust collection systems, and modular design, enhance performance and ease of maintenance. The advantages of using these conveyors, such as reduced labor costs, improved product quality, and energy efficiency, make them a valuable investment for businesses in need of effective powder handling solutions. By understanding the working principle and features of these conveyors, companies can make informed decisions about integrating them into their production processes, ultimately improving operational efficiency and product quality.




