Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of specialized equipment for handling and conveying bulk materials, including advanced systems for moisture - containing ammonium nitrate powder. This article provides an in - depth look at the working principle and key features of such conveyors, highlighting their importance in industrial applications where efficient and safe material transport is critical.
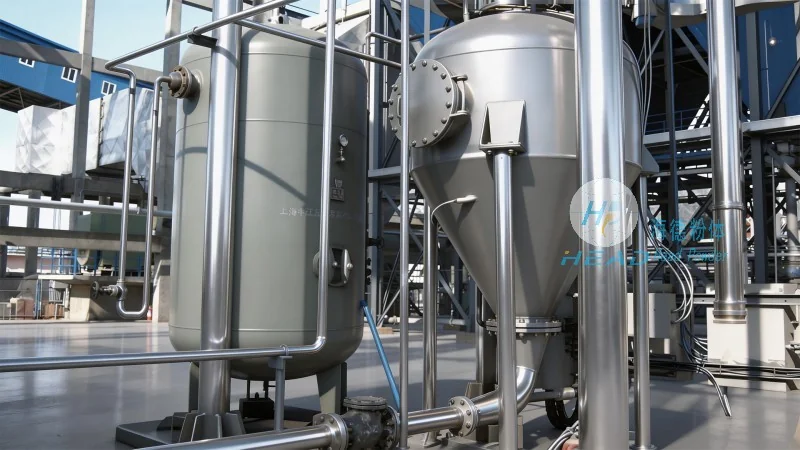
Company Introduction
HeadPowder, as a professional manufacturer based in Shandong, China, has established itself as a leading provider of engineering solutions for bulk material handling. With a strong focus on innovation and customer - oriented design, the company develops equipment tailored to meet the specific needs of various industries, ensuring reliability, efficiency, and safety in material processing operations.
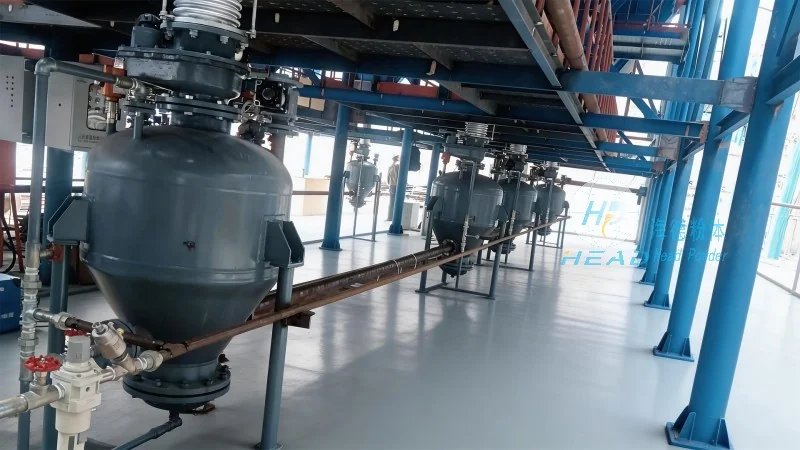
Working Principle of Moisture - Containing Ammonium Nitrate Powder Conveyors
The working principle of a moisture - containing ammonium nitrate powder conveyor is centered on the efficient transport of granular materials that have a certain moisture content. These conveyors typically employ a combination of mechanical components to move the material from the loading point to the discharge point. The system usually starts with a hopper or feeding mechanism that receives the ammonium nitrate powder with moisture. The material is then fed into a conveyor section, which may consist of a screw conveyor, belt conveyor, or pneumatic system, depending on the specific design and the characteristics of the material. The screw conveyor, for instance, uses rotating screws to push the material forward, while the belt conveyor relies on a moving belt to transport the powder. In the case of moisture - containing ammonium nitrate, the conveyor design must account for the material's tendency to stick or clump, which can affect the flow and transport efficiency. Therefore, the conveyor may incorporate features such as variable speed drives, cleaning mechanisms, or special materials for the conveyor components to ensure smooth operation and prevent blockages. The discharge mechanism at the end of the conveyor then delivers the material to the next processing stage or storage area. Overall, the working principle aims to maintain a consistent flow rate, minimize material degradation, and ensure safe handling of the ammonium nitrate, which is a critical chemical in many industrial processes.
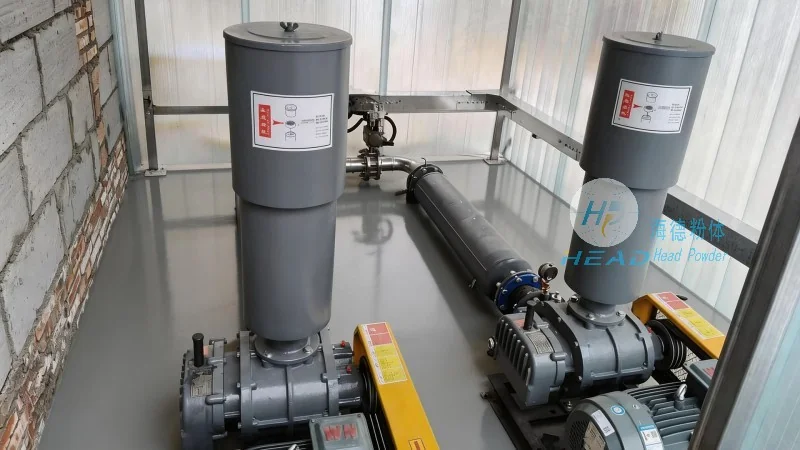
Key Features of the Conveyors
The key features of moisture - containing ammonium nitrate powder conveyors are designed to address the unique challenges associated with handling this material. One of the primary features is the ability to handle materials with a certain moisture content without causing excessive wear or damage to the equipment. The conveyor components, such as the screws, belts, or pipes, are often made from materials that are resistant to corrosion and abrasion, such as stainless steel or special alloys, to withstand the chemical properties of ammonium nitrate. Another important feature is the control system, which allows for precise regulation of the conveyor speed and flow rate. This is crucial for maintaining a stable operation and preventing overloading or underloading of the system. The system may also include sensors and monitoring devices to detect any abnormalities, such as blockages or changes in material flow, and trigger appropriate responses to ensure safety and efficiency. Additionally, the design of the conveyor may include features to minimize dust generation and improve environmental safety, as ammonium nitrate is a fine powder that can create dust hazards. The conveyors are also designed to be easy to clean and maintain, with removable parts that can be replaced or cleaned to prevent contamination and ensure long - term performance. Overall, these features make the conveyors suitable for various industrial applications, including fertilizer production, chemical processing, and material handling in agricultural and industrial settings.
Applications and Benefits
Moisture - containing ammonium nitrate powder conveyors are widely used in industries where the efficient and safe transport of ammonium nitrate is essential. In the fertilizer industry, for example, these conveyors are used to move ammonium nitrate from storage to processing units, ensuring a continuous supply of raw material for the production of fertilizers. In chemical processing plants, the conveyors are used to transport ammonium nitrate to reactors or other processing equipment, where it is used as a key ingredient in the production of various chemicals. The benefits of using these conveyors include improved efficiency in material handling, reduced downtime due to equipment failures, and enhanced safety by minimizing the risk of dust explosions or material blockages. Additionally, the advanced design of the conveyors helps to maintain the quality of the ammonium nitrate, preventing moisture loss or degradation during transport. This is particularly important for ammonium nitrate, as its quality can be affected by exposure to moisture or air, which can lead to changes in its physical properties and performance. By using specialized conveyors, industries can ensure that the ammonium nitrate is transported in optimal conditions, maintaining its quality and effectiveness for the intended applications.
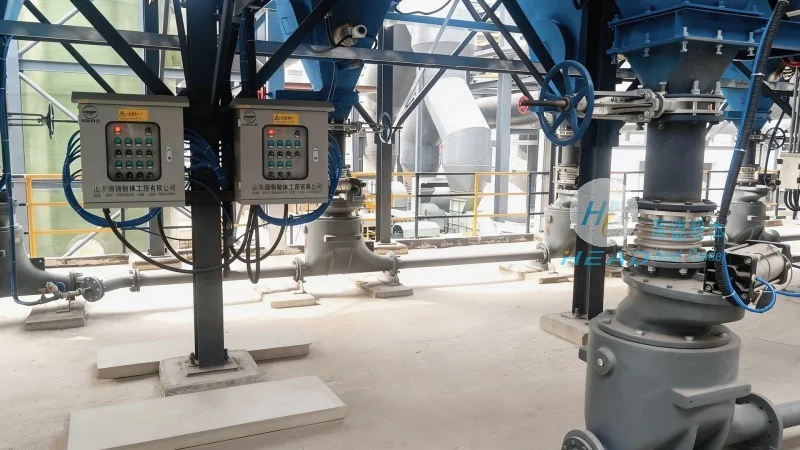
Conclusion
Moisture - containing ammonium nitrate powder conveyors are critical equipment in industries that rely on the efficient handling of this important chemical. The working principle and key features of these conveyors are designed to address the unique challenges of handling materials with moisture content, ensuring reliable and safe transport. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. provides high - quality conveyors that meet the specific needs of various industries, contributing to improved efficiency and safety in material processing operations. With a focus on innovation and customer satisfaction, HeadPowder continues to develop advanced solutions for bulk material handling, helping businesses achieve their operational goals while maintaining the highest standards of safety and performance.




