Wheat starch material handling systems are critical components in the processing industry, designed to efficiently transport and manage wheat starch, a key ingredient in various food and industrial applications. Understanding the working principle and features of such systems is essential for optimizing production efficiency and ensuring product quality. This article provides a detailed overview of the mechanisms and characteristics of wheat starch material handling equipment, highlighting how these systems contribute to seamless operations in starch processing facilities.
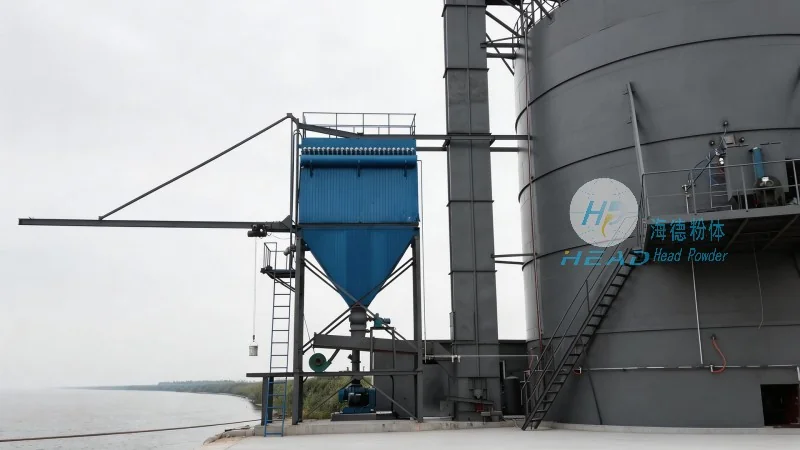
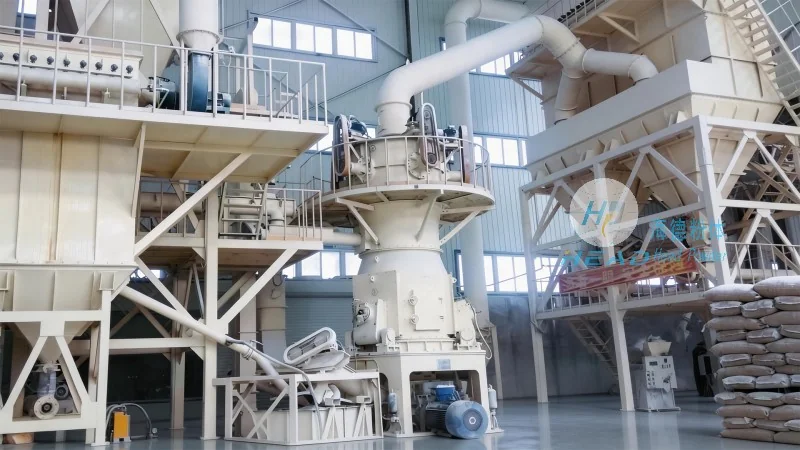
Working Principle of Wheat Starch Material Handling Systems
The working principle of wheat starch material handling systems typically involves several key steps, each designed to ensure the safe and efficient movement of raw materials and finished products. The process begins with the intake of wheat starch, which is often stored in bulk storage silos or hoppers. From there, the material is transferred through a series of conveyors, elevators, and pneumatic systems, depending on the specific requirements of the processing line. Conventional systems may use belt conveyors for horizontal transport, while vertical elevators or bucket elevators handle vertical movement. Pneumatic conveying systems, on the other hand, utilize air pressure to transport starch particles through pipelines, offering a dust-free and hygienic method for handling fine powders like wheat starch. The entire system is controlled by a centralized control panel, which monitors and adjusts the flow rate, pressure, and speed of each component to maintain optimal performance. This integrated approach ensures that the material is moved from storage to processing units, and eventually to packaging or further processing stages, with minimal human intervention and maximum efficiency.
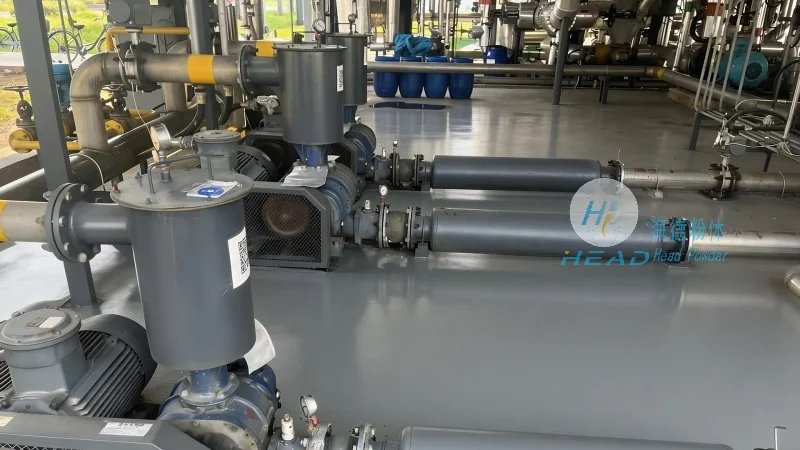
Key Features of Wheat Starch Material Handling Equipment
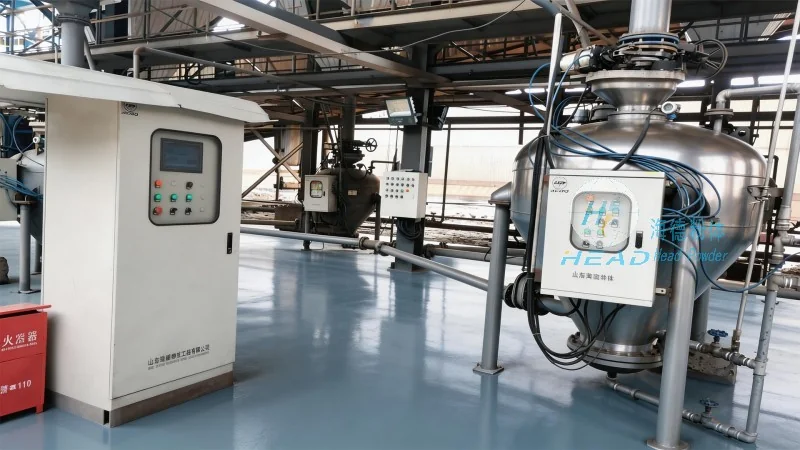
Wheat starch material handling systems are characterized by several key features that enhance their functionality and reliability. One of the primary features is the ability to handle fine, powdery materials without causing dust accumulation or blockages. This is achieved through the use of specialized equipment such as rotary valves, which regulate the flow of starch into conveyors, and dust collection systems that capture and filter airborne particles. Another important feature is the system's adaptability to varying production volumes. Modern material handling systems are equipped with variable speed drives and adjustable conveyor speeds, allowing operators to match the flow rate to the current production demand. This flexibility helps in reducing energy consumption and preventing overloading of downstream equipment. Additionally, the systems are designed with hygiene and safety in mind, featuring smooth, easy-to-clean surfaces and explosion-proof components, which are crucial in food processing environments. The use of stainless steel construction further enhances durability and resistance to corrosion, ensuring long-term performance. Furthermore, advanced control systems, including programmable logic controllers (PLCs) and human-machine interfaces (HMIs), provide real-time monitoring and diagnostic capabilities, enabling quick identification and resolution of any operational issues. These features collectively contribute to the high efficiency, reliability, and safety of wheat starch material handling systems.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of specialized material handling equipment for the food and starch processing industries. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient solutions for their material handling needs. HeadPowder's expertise lies in designing and manufacturing systems tailored to the specific requirements of wheat starch processing, ensuring that each component is optimized for performance and durability. The company's facilities are equipped with state-of-the-art technology and skilled engineering teams, enabling them to develop customized solutions that meet the unique challenges of each client. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including installation, training, and maintenance services. By leveraging its extensive experience and technical capabilities, HeadPowder continues to deliver high-quality material handling systems that enhance operational efficiency and product quality for its clients. HeadPowder's operations are based in Shandong, China, where the company maintains its manufacturing and research facilities, ensuring close proximity to its customers and the ability to provide timely support.




