For industrial operations that require efficient handling of bulk materials, pneumatic conveying systems offer a reliable solution. Specifically, the tonne bag unloading pneumatic conveying machine is a specialized equipment designed to streamline the process of transferring materials from large bags into processing or storage systems. This equipment is integral to industries where bulk materials are commonly packaged in tonne bags, such as chemical, food, and agricultural sectors.
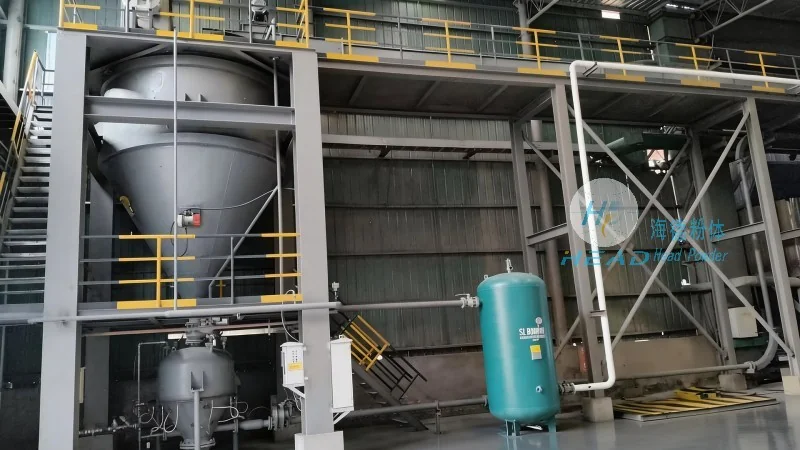
Principle of Tonne Bag Unloading Pneumatic Conveying
The core principle of this equipment is based on the use of compressed air to create a flow of material through a pipeline. When a tonne bag is placed at the inlet of the machine, the compressed air is introduced into the bag, causing the material to be dislodged and carried through the conveying line. The system typically consists of a hopper, a rotary valve, a conveying pipe, and a dust collector. The hopper collects the material from the bag, the rotary valve controls the flow of material into the conveying pipe, and the compressed air propels the material through the pipeline to the destination point. The dust collector ensures that any airborne particles are captured, maintaining a clean and safe working environment.
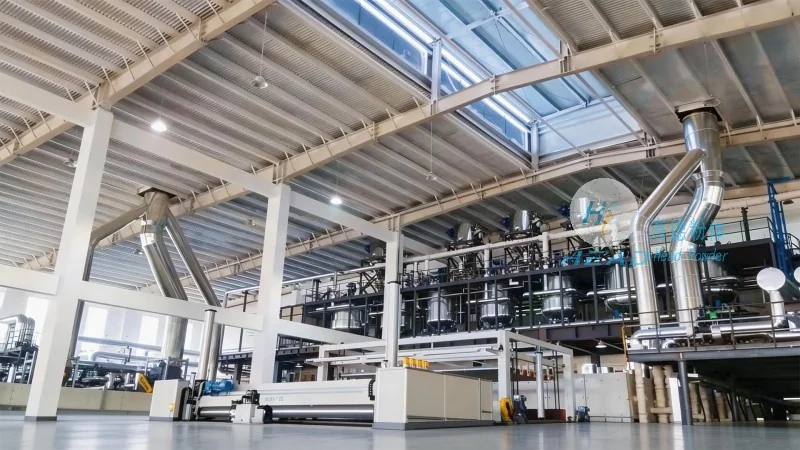
Working Scene Characteristics
The tonne bag unloading pneumatic conveying machine is particularly suited for applications where large volumes of bulk materials need to be handled with minimal manual intervention. In chemical plants, for example, this equipment is used to transfer raw materials like powders and granules from tonne bags into reactors or storage silos. The food industry also benefits from this technology, as it allows for the safe and hygienic transfer of food-grade powders and ingredients without cross-contamination. Agricultural facilities, such as grain processing plants, utilize this equipment to move bulk crops from bags into processing lines or storage bins. The key characteristics of these working scenes include high throughput, reduced labor costs, and improved safety compared to traditional manual unloading methods.
Advantages in Industrial Applications
One of the primary advantages of the tonne bag unloading pneumatic conveying machine is its ability to handle a wide range of materials, from fine powders to coarse granules. The system is also highly flexible, as it can be configured to accommodate different bag sizes and material types. Additionally, the equipment operates with minimal noise and vibration, making it suitable for use in sensitive environments. The use of compressed air as the conveying medium also eliminates the need for mechanical components that could cause wear and tear, reducing maintenance costs over time. Furthermore, the dust collection system ensures compliance with environmental regulations, making it an environmentally friendly solution for industrial material handling.
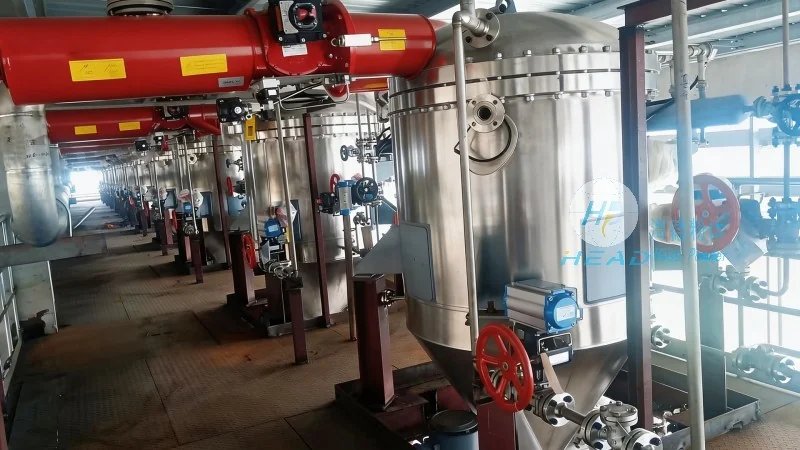
Company Overview and Expertise
HeadPowder, a leading manufacturer of material handling equipment, specializes in the design and production of tonne bag unloading pneumatic conveying machines. With years of experience in the industry, the company has developed a reputation for producing high-quality, reliable equipment that meets the needs of various industrial sectors. HeadPowder's products are engineered to provide efficient and safe material handling solutions, ensuring that clients can operate their facilities with minimal downtime and maximum productivity. The company's headquarters is located in Shandong, China, where it has a state-of-the-art manufacturing facility equipped with advanced technology and skilled workforce. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking to optimize their material handling processes.




