Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer based in Shandong, China. The company specializes in the design, development, and production of advanced powder conveying systems, particularly those tailored for handling bulk powder materials from tonne bags. This article delves into the fundamental principles of such systems and highlights the key characteristics of their operational scenarios.
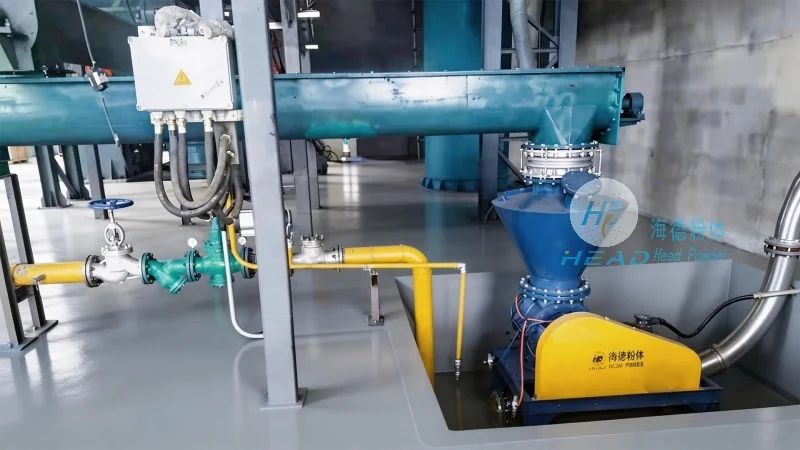
Overview of Tonne Bag Powder Conveying Systems
A tonne bag powder conveying system is a specialized piece of equipment engineered to efficiently transfer bulk powder from large, flexible containers known as tonne bags (also called super sacks or big bags) into processing lines, storage silos, or other destinations. These systems are critical in industries where large volumes of powder are handled, such as chemical manufacturing, food processing, pharmaceuticals, and mining. The primary goal of the system is to ensure a smooth, reliable, and safe transfer of powder, minimizing material loss and operational downtime.
Core Principles of the Conveying Process
The operation of a tonne bag powder conveying system is based on a combination of mechanical and pneumatic principles. The process typically begins with the opening of the tonne bag, which is usually done using a specialized bag opener or a mechanical clamp that cuts and spreads the bag's top. Once the bag is opened, the powder is drawn out through a hopper or a discharge valve. From there, the powder is conveyed to the next stage using either a pneumatic system (air pressure) or a mechanical system (such as a screw conveyor or a belt conveyor).
In pneumatic conveying systems, the powder is suspended in a stream of air and transported through pipes. This method is particularly effective for fine powders and can handle long distances and multiple transfers. The system includes components like a vacuum or pressure pump, a filter to remove dust, and a control panel to regulate the flow rate. Mechanical systems, on the other hand, rely on the physical movement of the powder through a conveyor mechanism, which is often more suitable for coarser materials or when air quality is a concern.
Key Working Scene Characteristics
The characteristics of tonne bag powder conveying systems are highly influenced by the specific operational environment and the nature of the powder being handled. Several key aspects define how these systems perform in different scenarios:
1. High Efficiency and Throughput: In industrial settings where large volumes of powder are processed daily, the system's ability to maintain high throughput is paramount. The design of the conveying mechanism, such as the speed of the screw or the air pressure in pneumatic systems, directly impacts the efficiency. For instance, in a chemical plant producing bulk fertilizers, the system must handle several tonne bags per hour without interruption to meet production targets.
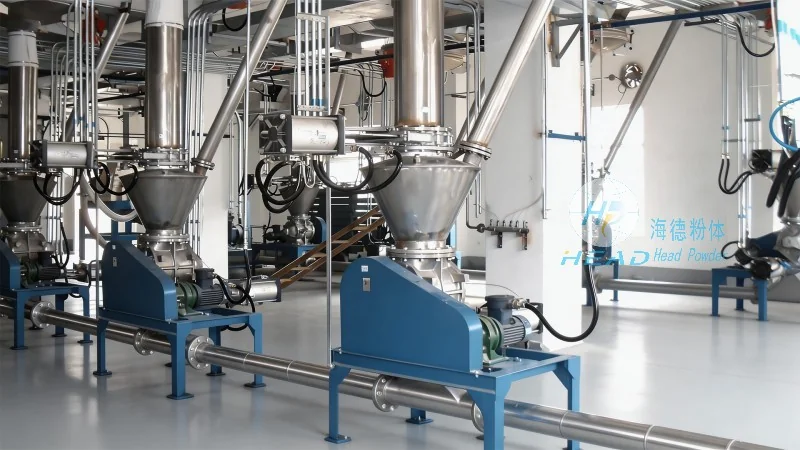
2. Material Handling Adaptability: Different industries require handling a wide range of powder types, from fine, dusty powders to coarse, abrasive materials. The tonne bag powder conveying system must be adaptable to these variations. This adaptability is achieved through adjustable components, such as variable speed drives, different hopper designs, and customizable filter systems. For example, in the food industry, where the powder might be sensitive to contamination, the system includes sanitary components to ensure hygiene.
3. Safety and Environmental Considerations: Handling powders can pose risks related to dust explosions and inhalation hazards. Modern tonne bag powder conveying systems incorporate safety features like explosion-proof designs, dust collection systems, and enclosed conveying paths to minimize these risks. Additionally, the system may include environmental controls, such as air filtration to comply with local regulations and protect the surrounding environment.
4. Space and Layout Flexibility: Industrial facilities often have limited space or complex layouts. The tonne bag powder conveying system is designed to be flexible in terms of installation and layout. It can be configured to fit into existing structures, with components like vertical or horizontal conveyors, and can be integrated with other processing equipment. This flexibility allows for efficient use of space and seamless integration into the production line.
Application Scenarios and Industry Examples
The versatility of tonne bag powder conveying systems makes them applicable across various industries. Here are some typical working scenarios where these systems are commonly used:
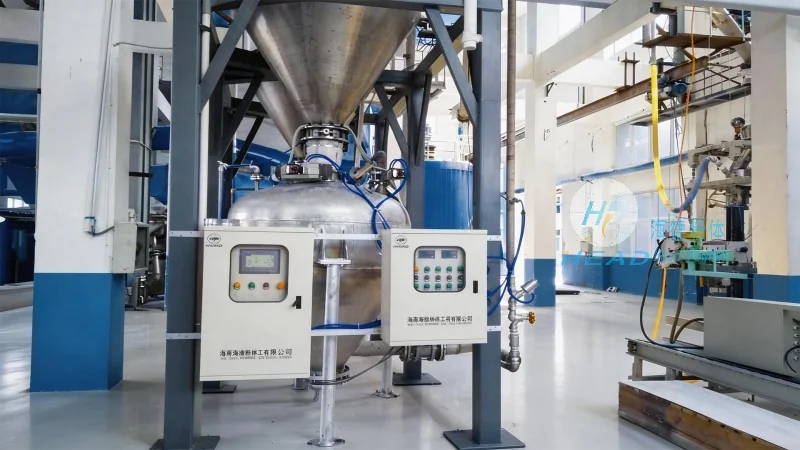
Chemical Manufacturing: In chemical plants, the system is used to transfer raw materials like powders for fertilizer production, pigments, or specialty chemicals. The high efficiency and reliability of the system ensure consistent quality in the final products. For example, a fertilizer plant might use a pneumatic conveying system to move large quantities of nitrogen or phosphorus powders from tonne bags to mixing tanks.
Food and Beverage Industry: The food industry requires systems that are hygienic and can handle food-grade powders, such as flour, sugar, or protein powders. The tonne bag powder conveying system in this sector is designed with stainless steel components, easy-to-clean surfaces, and sealed conveying paths to prevent contamination. A bakery might use such a system to transfer flour from tonne bags into storage silos or directly into mixing machines.
Pharmaceutical Sector: In pharmaceutical manufacturing, the system must meet stringent standards for purity and safety. The equipment is often equipped with sterile filtration, positive pressure systems, and automated controls to ensure that the powder is handled under controlled conditions. A pharmaceutical company producing active pharmaceutical ingredients (APIs) might use a mechanical conveying system to transfer raw powder from tonne bags into a high-purity processing line.
Mining and Minerals Processing: In mining operations, the system is used to handle bulk minerals and ores from tonne bags. The robust design of the equipment can withstand the abrasive nature of the materials and the harsh environmental conditions of mining sites. A mining company processing iron ore might use a large-scale pneumatic conveying system to transport the ore from storage bags to the crushing and grinding equipment.
Conclusion: The Importance of Advanced Powder Conveying Systems
As industries continue to demand higher efficiency and reliability in material handling, the tonne bag powder conveying system remains a critical component. The combination of mechanical and pneumatic principles, along with the adaptability to various powder types and operational environments, makes these systems indispensable. Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized solutions that meet the specific needs of different industries, ensuring that the powder transfer process is efficient, safe, and cost-effective.




