For industrial applications, the efficient and reliable transport of limestone powder is crucial for maintaining production efficiency and ensuring product quality. Limestone powder, a common raw material in various industries such as cement manufacturing, chemical processing, and environmental remediation, requires specialized handling systems to manage its fine, dusty nature. This article explores the operation process and working principles of limestone powder material handling, highlighting key components, operational steps, and the importance of proper system design for optimal performance.
Key Components of Limestone Powder Handling Systems
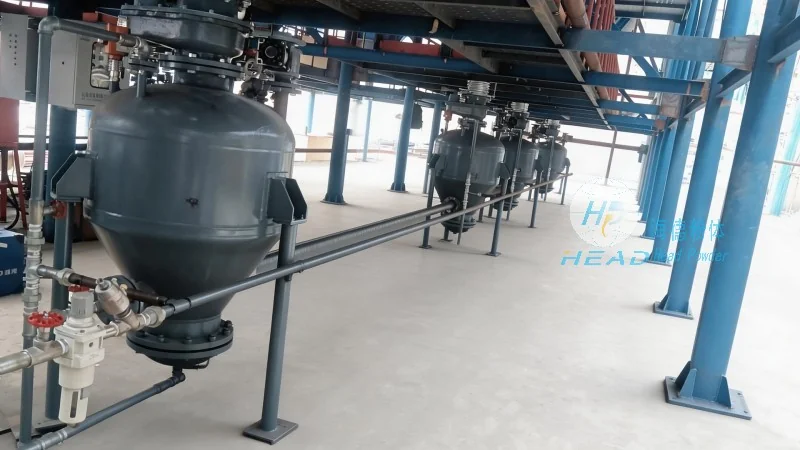
The limestone powder handling system typically consists of several critical components that work in tandem to ensure smooth material transport. These components include feeders, conveyors, dust collection systems, and storage silos. Feeders, such as rotary valves or screw conveyors, are used to regulate the flow of limestone powder from the storage silo to the conveyor system. Conveyors, often in the form of belt conveyors or pneumatic systems, transport the powder from one location to another. Dust collection systems are essential to maintain air quality and prevent dust accumulation, which can lead to health hazards and equipment damage. Storage silos provide a controlled environment for storing limestone powder, ensuring consistent material availability for processing.
Operation Process of Limestone Powder Material Handling
The operation process of limestone powder material handling involves several sequential steps that ensure the material is transported safely and efficiently. The process begins with the material being stored in a silo. The feeder then regulates the flow of limestone powder from the silo into the conveyor system. The conveyor transports the powder to the processing area or another storage location. During this process, dust collection systems continuously remove airborne particles to maintain a clean working environment. The entire system operates under controlled conditions, with sensors and controls monitoring flow rates, pressure, and other critical parameters to prevent overloading or system failures.
Working Principles of Limestone Powder Handling Systems
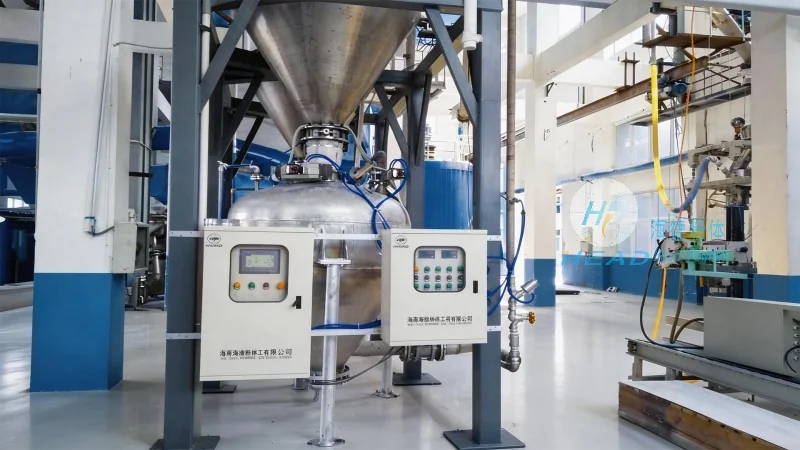
The working principles of limestone powder handling systems are based on the physical properties of the material and the design of the equipment used. Limestone powder is a fine, dry material that can be easily suspended in air, making it susceptible to dust generation. Therefore, the system design prioritizes containment and control of dust. The feeders are designed to minimize material spillage and ensure a consistent flow rate. The conveyors are selected based on the material's characteristics, such as particle size and moisture content, to prevent blockages or wear. Pneumatic systems, which use air pressure to transport the powder, are often preferred for fine powders due to their ability to handle high volumes and maintain low dust levels. The dust collection systems, typically using bag filters or cartridge filters, capture the fine particles and return them to the system or dispose of them safely.
Importance of Proper System Design and Maintenance
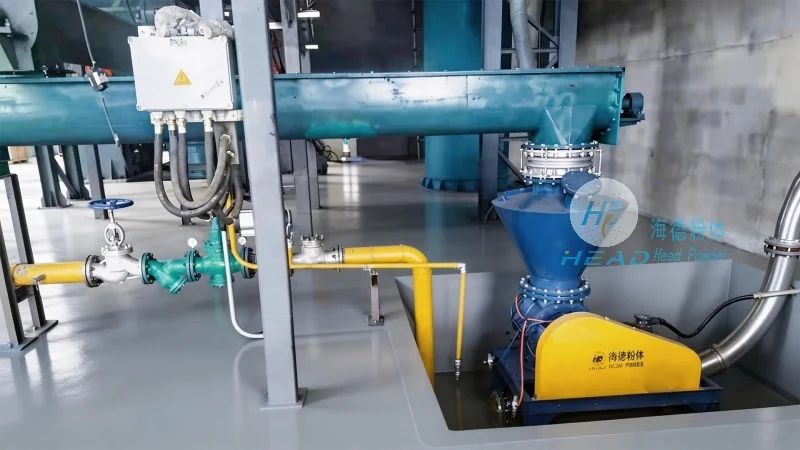
Proper system design and regular maintenance are essential for the long-term performance and reliability of limestone powder handling systems. A well-designed system considers factors such as the material's properties, the required flow rate, and the operating environment. Regular maintenance, including cleaning of dust collection systems, inspection of conveyor belts, and calibration of sensors, ensures that the system operates at optimal efficiency. Proper maintenance also helps to prevent equipment failures, reduce downtime, and minimize the risk of accidents related to dust exposure. Additionally, adhering to safety regulations and industry standards is crucial for maintaining a safe working environment and ensuring compliance with environmental requirements.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of material handling solutions for limestone powder and other fine materials. With a focus on innovation and customer satisfaction, the company specializes in designing and manufacturing customized handling systems tailored to the specific needs of its clients. Headpowder's expertise in material handling technology ensures that its systems are efficient, reliable, and safe, meeting the demands of various industrial applications. The company's commitment to quality and service has earned it a reputation as a trusted partner in the material handling industry. Headpowder is based in Shandong, China, and serves clients worldwide with its advanced solutions and professional support.




