For industrial facilities dealing with bulk materials, efficient and reliable material handling is crucial to maintaining smooth production operations. The tonne bag material handling system, developed by Shandong HeadPowder Engineering Co., Ltd., offers a comprehensive solution that integrates advanced technology and robust engineering to streamline the entire material handling workflow. This system is designed to handle large quantities of bulk materials, typically stored in tonne bags, ensuring safe and efficient transfer from storage to processing areas.
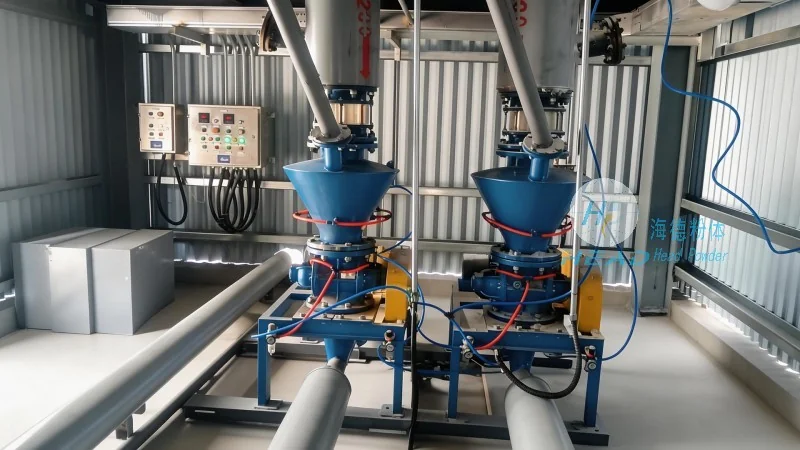
Key Components and Their Roles
The tonne bag material handling system consists of several key components that work in tandem to achieve optimal performance. The primary components include the bag lifting mechanism, conveyor system, and material discharge equipment. The bag lifting mechanism, often utilizing hydraulic or mechanical arms, is responsible for securely lifting the tonne bags from the ground or storage racks. This component ensures that the bags are handled with precision, minimizing the risk of damage or spillage. The conveyor system, which may include belt conveyors or chain conveyors, then transports the lifted bags to the processing or packaging area. The material discharge equipment, such as spout valves or discharge gates, facilitates the controlled release of the material from the tonne bags into the next stage of the production process.
System Operation Process
The operation of the tonne bag material handling system follows a systematic sequence to ensure efficient material transfer. The process begins with the positioning of the tonne bags at the loading area. The lifting mechanism then engages, lifting the bag vertically and moving it to the conveyor system. The conveyor transports the bag to the discharge point, where the discharge equipment opens to release the material. This sequence is typically automated, with sensors and control systems monitoring each step to ensure smooth operation. The system is designed to handle multiple bags simultaneously, increasing throughput and reducing downtime. Each operation is synchronized to maintain a consistent flow of material, which is critical for maintaining production efficiency.
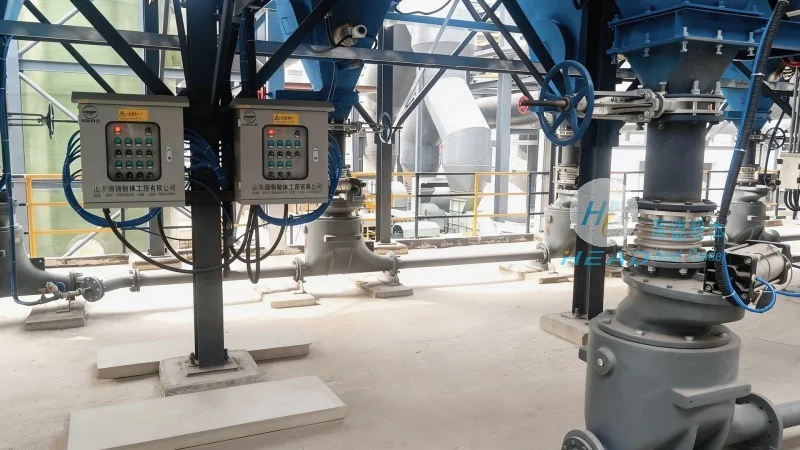
Working Principle of the System
The working principle of the tonne bag material handling system is based on mechanical and hydraulic principles to achieve precise control over the material handling process. The lifting mechanism operates by applying force to the tonne bag, using hydraulic cylinders or mechanical levers to lift the bag off the ground. The conveyor system uses rollers or belts to move the bag horizontally, while the discharge equipment uses valves or gates to control the release of the material. The entire system is controlled by a central control unit that coordinates the actions of each component. Sensors are integrated throughout the system to detect the position of the bags, the status of the conveyor, and the level of material in the discharge area. This feedback loop allows the system to adjust its operation in real-time, ensuring optimal performance and preventing issues such as overloading or material blockages.
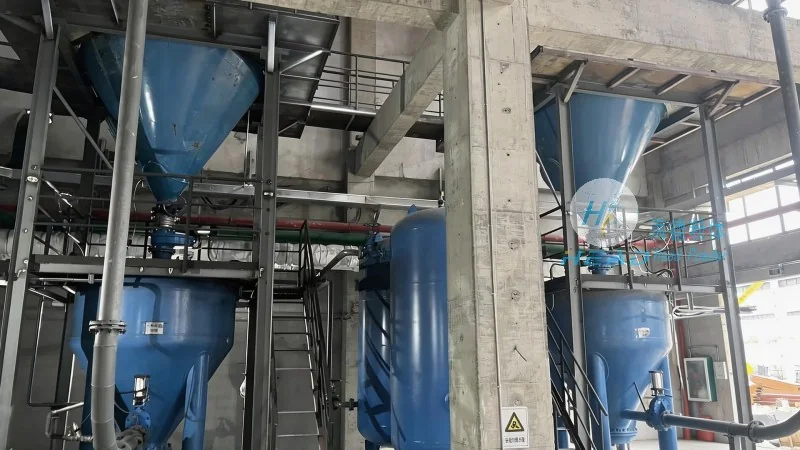
Advantages of the Tonne Bag Material Handling System
Implementing a tonne bag material handling system offers several advantages for industrial operations. Firstly, it significantly improves material handling efficiency by reducing manual labor and increasing throughput. The automated process minimizes the risk of human error, leading to more consistent and reliable material transfer. Secondly, the system enhances safety by eliminating the need for workers to handle heavy tonne bags manually, reducing the risk of injuries. Additionally, the system reduces material spillage and contamination, as the discharge process is controlled and precise. The robust design of the system ensures long-term reliability, with minimal maintenance requirements. The system is also scalable, allowing it to be adapted to different production needs and material types. Overall, the tonne bag material handling system provides a cost-effective and efficient solution for bulk material handling in various industrial applications.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of material handling systems in China. With a focus on innovation and quality, the company has developed a range of advanced solutions for bulk material handling, including the tonne bag material handling system. HeadPowder Engineering is committed to providing customized solutions that meet the specific needs of its clients, ensuring optimal performance and reliability. The company's products are designed to meet international standards and are widely used in various industries, including food processing, chemical manufacturing, and mining. HeadPowder Engineering is dedicated to delivering high-quality products and excellent customer service, helping businesses improve their operational efficiency and productivity.




