HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling rare earth mineral powders. The rare earth mineral powder pneumatic conveying machine is a critical piece of equipment in industrial processes that require efficient, dust-free, and reliable material transport. This article delves into the operational process and working principles of such equipment, highlighting its significance in modern material handling applications.
Introduction to Rare Earth Mineral Powder Pneumatic Conveying
Rare earth minerals are essential components in various high-tech industries, including electronics, aerospace, and renewable energy. The efficient and safe transport of these powders is paramount to ensure product quality and operational safety. Pneumatic conveying systems offer a solution by utilizing air as the medium to move materials, eliminating the need for mechanical components that might cause contamination or wear. HeadPowder's rare earth mineral powder pneumatic conveying machine is engineered to meet the stringent requirements of handling these valuable and often hazardous materials.
Key Components of the Pneumatic Conveying System
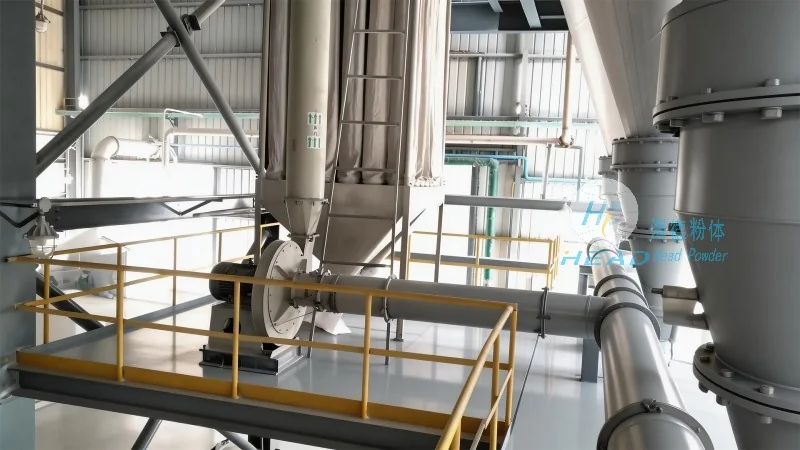
The rare earth mineral powder pneumatic conveying machine consists of several core components that work in tandem to achieve effective material transport. These components include a material hopper, a rotary valve or feeder, a conveying line, a dust collector, and a blower or air compressor. The material hopper is designed to store the rare earth mineral powder, ensuring a consistent feed to the system. The rotary valve or feeder regulates the flow of powder into the conveying line, controlling the rate of material discharge. The conveying line, typically made of stainless steel or other corrosion-resistant materials, transports the powder through the system. The dust collector captures any airborne particles, maintaining air quality and preventing contamination. The blower or air compressor generates the necessary air pressure to move the powder through the system.
Working Principle of the Pneumatic Conveying Process
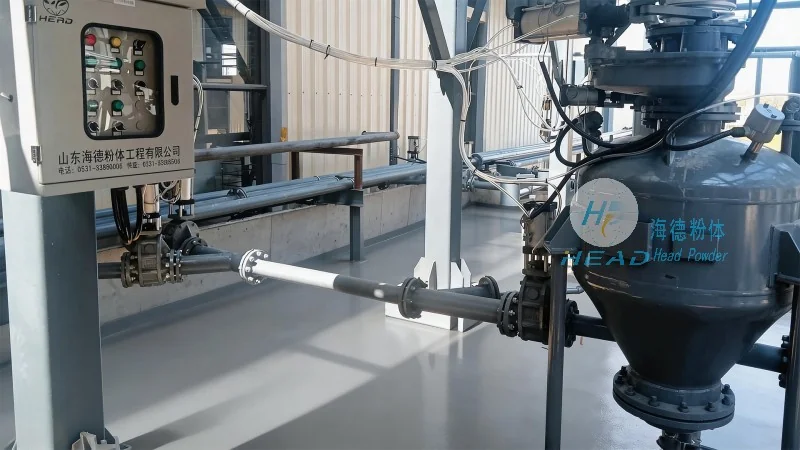
The operation of the rare earth mineral powder pneumatic conveying machine follows a systematic process that ensures efficient material transport. The process begins with the material being fed from the hopper into the rotary valve or feeder. The feeder controls the flow rate, ensuring a steady supply of powder to the conveying line. Simultaneously, the blower or air compressor generates high-pressure air, which is introduced into the conveying line. As the air flows through the line, it creates a low-pressure zone that draws the powder particles into the air stream. The powder particles are then carried along the conveying line to the destination point, such as a storage silo or processing unit. The dust collector is integrated into the system to capture any fine particles that may escape, ensuring that the air discharged is clean and safe. The entire process is controlled by a programmable logic controller (PLC) or other automation systems, allowing for precise regulation of flow rates, air pressure, and material discharge.
Operation Process and Control Systems
The operation of the rare earth mineral powder pneumatic conveying machine involves several steps that are coordinated by the control system. The process starts with the startup sequence, where the blower or air compressor is activated, and the conveying line is pressurized. The material hopper is then filled with the rare earth mineral powder, and the rotary valve or feeder is set to the desired flow rate. The control system monitors the pressure and flow rates in real-time, adjusting the air pressure or feed rate as needed to maintain optimal performance. During operation, the system continuously checks for any blockages or abnormalities, such as excessive pressure or low material levels, and triggers alarms or shutdown procedures if necessary. The shutdown sequence involves stopping the blower or air compressor, allowing the conveying line to depressurize, and then stopping the feeder to prevent material from being discharged into the hopper. The control system ensures that the entire process is safe, efficient, and consistent, minimizing downtime and maximizing productivity.
Advantages of Using a Rare Earth Mineral Powder Pneumatic Conveying Machine
HeadPowder's rare earth mineral powder pneumatic conveying machine offers several advantages over traditional mechanical conveying systems. One of the primary benefits is the elimination of dust and contamination, as the material is transported in a closed system. This is particularly important for rare earth minerals, which are often sensitive to moisture and air exposure. The system also reduces labor costs by automating the material handling process, as it eliminates the need for manual loading and unloading. Additionally, the pneumatic conveying system is more flexible, allowing for changes in material flow rates and destination points without significant modifications to the equipment. The equipment is also designed for easy maintenance, with accessible components that can be serviced quickly, minimizing downtime. The use of corrosion-resistant materials ensures the longevity of the system, even when handling aggressive or abrasive materials.
Applications and Industries
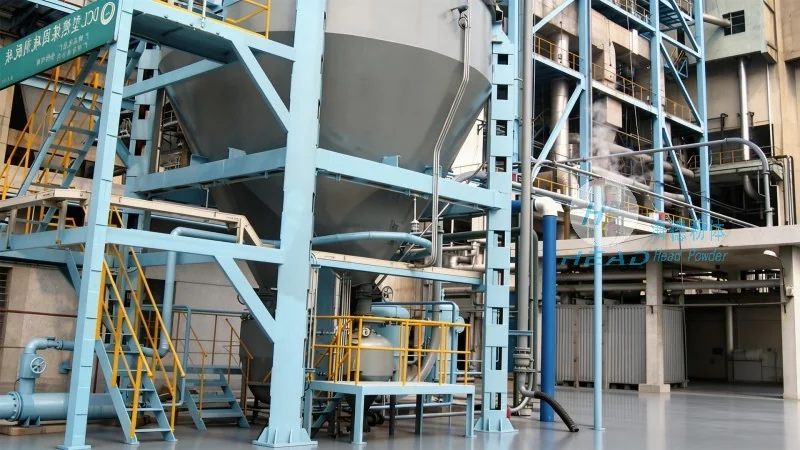
The rare earth mineral powder pneumatic conveying machine is widely used in various industries that require the transport of fine powders. In the rare earth industry, it is used to transport raw materials from storage silos to processing units, ensuring a continuous and efficient supply of materials. In the electronics industry, it is used to transport rare earth oxides to manufacturing lines, where they are used in the production of magnets and other components. The system is also used in the aerospace industry for the transport of rare earth-based alloys, and in the renewable energy sector for the handling of materials used in wind turbine and solar panel production. The versatility of the pneumatic conveying system makes it suitable for a wide range of applications, from small-scale operations to large industrial plants.
Conclusion
HeadPowder's rare earth mineral powder pneumatic conveying machine is a reliable and efficient solution for handling rare earth mineral powders. The equipment is designed with advanced technology and materials to ensure optimal performance, safety, and durability. The systematic operation process and control systems ensure consistent and safe material transport, while the advantages of the pneumatic conveying system make it a preferred choice over traditional methods. As the demand for rare earth minerals continues to grow, the importance of efficient material handling systems like the pneumatic conveying machine becomes increasingly critical. HeadPowder remains committed to providing high-quality equipment that meets the evolving needs of the industry, ensuring that customers can achieve their production goals with minimal downtime and maximum efficiency.




