Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier specializing in the design, development, and production of pneumatic conveying systems. With a strong focus on technological innovation and customer-centric solutions, the company has established itself as a leading provider in the field of bulk material handling, particularly for glucose and other similar granular or powdered substances. HeadPowder's headquarters is located in Shandong, China, where the company leverages local industrial resources and expertise to deliver high-quality, reliable equipment tailored to meet diverse industrial needs.
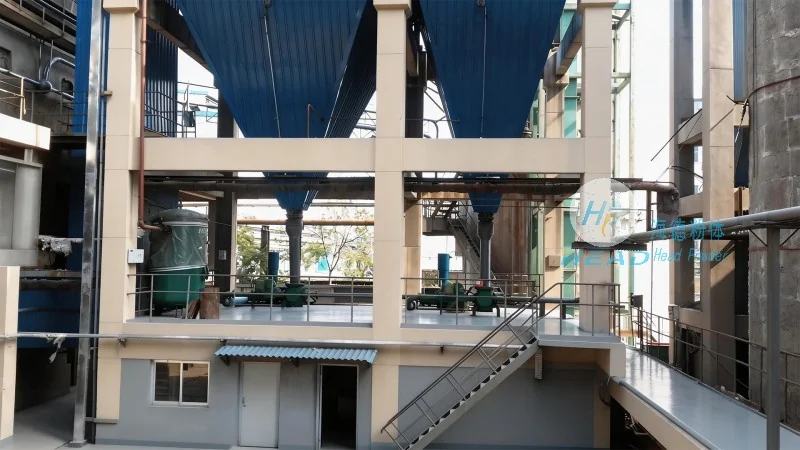
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder is dedicated to advancing the efficiency and safety of material handling processes through advanced pneumatic conveying technologies. The company's team of experienced engineers and technicians combines deep industry knowledge with cutting-edge research to develop customized solutions that optimize material transport, reduce operational costs, and enhance overall production line performance. By adhering to strict quality control standards and adhering to international safety regulations, HeadPowder ensures that its products meet the highest industry benchmarks, providing customers with durable and efficient equipment for long-term use.
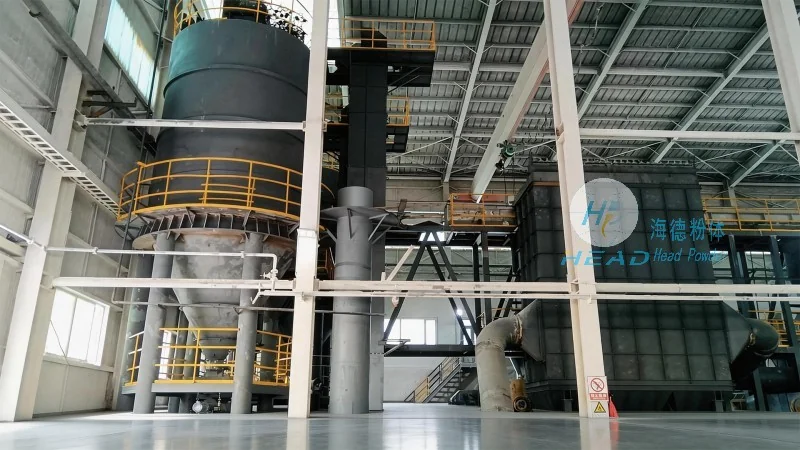
Glucose Pneumatic Conveying System Overview
Glucose pneumatic conveying systems are engineered to transport glucose granules or powders from storage silos or production lines to processing units, packaging stations, or other destinations within a facility. These systems utilize compressed air or other gases to create a flow of material through a network of pipes, eliminating the need for mechanical components like conveyor belts or buckets that may cause contamination or wear. The system typically consists of a hopper, a feeder, a conveying line, and a receiver, all working in tandem to ensure smooth and continuous material movement. HeadPowder's glucose pneumatic conveying systems are designed to handle various glucose forms, including crystalline or powdered glucose, with precision and reliability.
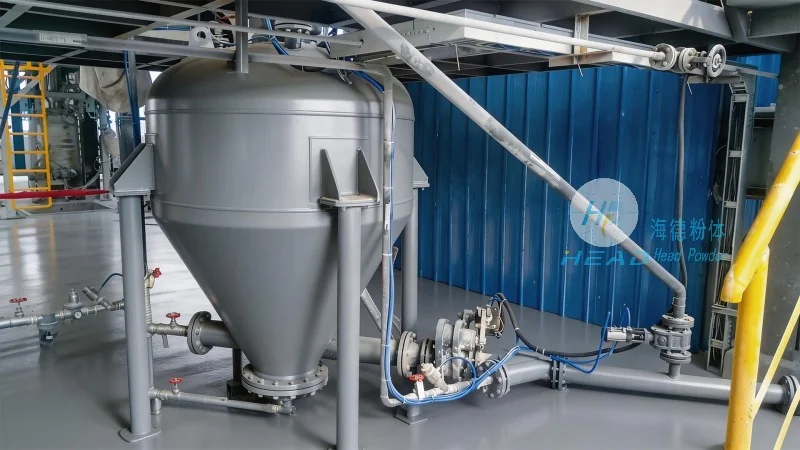
Structural Principles of Pneumatic Conveying Systems
The core structural principle of a pneumatic conveying system is the generation of a pressure differential between the material source and the destination. By introducing compressed air into the conveying line, the system creates a flow that lifts and transports the material particles. The design of the system, including the size and configuration of the pipes, the type of air injection method (e.g., positive pressure or negative pressure), and the placement of components like the feeder and receiver, plays a critical role in determining the system's efficiency and capacity. HeadPowder's engineers carefully calculate these parameters to ensure optimal performance, minimizing energy consumption while maximizing material throughput. The system's structural integrity is also a key consideration, with robust materials and construction methods used to withstand the pressures and stresses associated with continuous operation.
Key Components and Their Functions
Several key components make up a glucose pneumatic conveying system, each with a specific function to ensure the system operates efficiently. The hopper serves as the storage container for the glucose, providing a consistent feed to the feeder. The feeder, often a rotary valve or a screw feeder, regulates the flow of material into the conveying line, preventing blockages and maintaining a steady flow rate. The conveying line, made of durable materials such as stainless steel or plastic, transports the material and air mixture. The air injection system, which can be a blower or a compressor, supplies the necessary pressure to move the material. The receiver, typically a collection hopper or a storage tank, collects the material at the destination. Each component is designed to work in harmony, with HeadPowder ensuring that all parts are compatible and optimized for the specific glucose handling requirements.
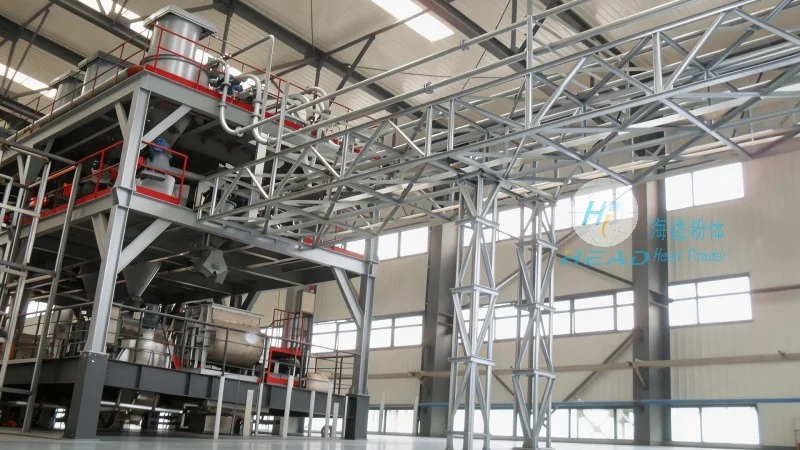
Application and Advantages
Glucose pneumatic conveying systems are widely used in the food and pharmaceutical industries, where maintaining product purity and preventing contamination is paramount. The systems are particularly suitable for transporting glucose from production lines to packaging areas, as they eliminate the need for manual handling and reduce the risk of product degradation. The advantages of pneumatic conveying for glucose include improved hygiene, reduced labor costs, increased operational efficiency, and the ability to handle materials in a dust-free environment. HeadPowder's systems are designed to meet the stringent requirements of these industries, with features such as easy cleaning, minimal product residue, and compliance with food safety regulations. Additionally, the systems are adaptable to different production scales, from small-scale operations to large industrial facilities, making them a versatile solution for various glucose processing needs.




