HeadPowder, a leading provider in the field of material handling solutions, specializes in the design and manufacturing of advanced pneumatic conveying systems. This article provides a comprehensive overview of corn cob pneumatic conveying, focusing on its structural design and operational principles to help clients understand the technology's capabilities and applications.
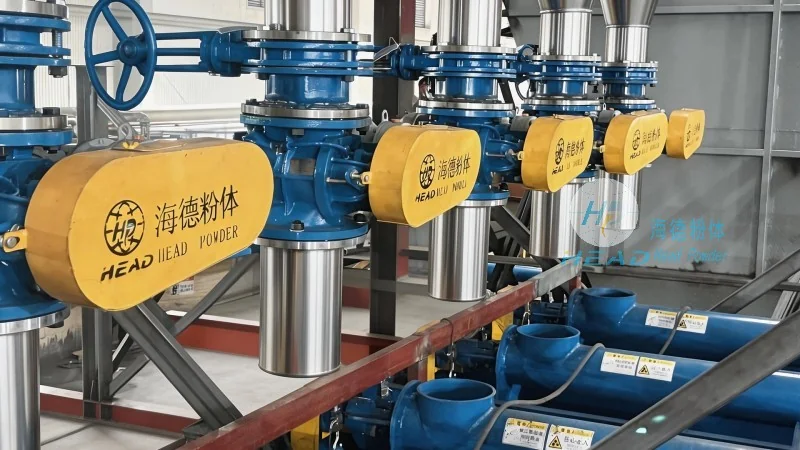
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the brand name of Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted manufacturer of high-quality pneumatic conveying equipment, catering to diverse industries that require efficient and reliable material transport solutions. With a strong commitment to innovation and customer satisfaction, HeadPowder delivers tailored solutions that meet the specific needs of its clients.
Understanding Corn Cob Pneumatic Conveying
Pneumatic conveying is a method of transporting bulk materials, such as corn cobs, through a pipeline using air pressure. This technology offers several advantages over traditional mechanical conveying systems, including reduced equipment wear, lower maintenance costs, and the ability to handle materials with high moisture content or abrasive properties. The corn cob pneumatic conveying system is specifically designed to handle the unique characteristics of corn cobs, ensuring efficient and safe transport from the source to the destination.
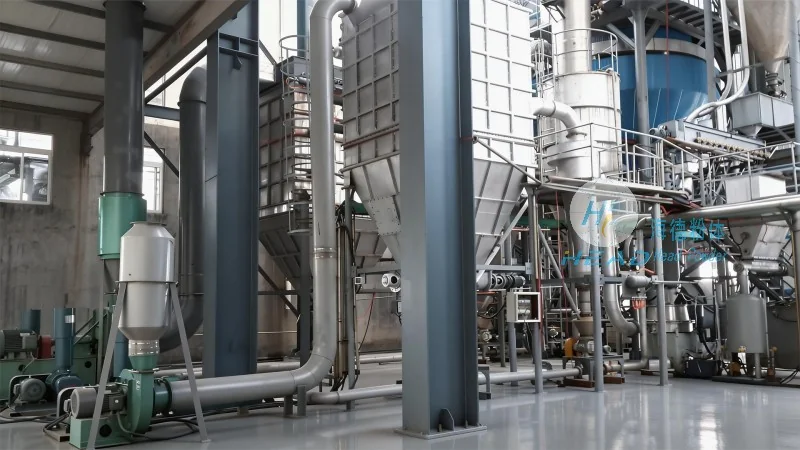
Structural Components of the Corn Cob Pneumatic Conveying System
The corn cob pneumatic conveying system consists of several key components that work in tandem to achieve effective material transport. These components include the hopper, which serves as the material storage and feeding unit; the air compressor, which generates the necessary air pressure to move the material; the pipeline network, which transports the material and air mixture; and the receiver, which collects the conveyed material at the end of the system. Each component is engineered to handle the specific challenges of corn cob transport, ensuring optimal performance and durability.
Working Principle of the System
The operation of the corn cob pneumatic conveying system involves a sequence of steps that ensure smooth material transport. Initially, corn cobs are fed into the hopper from the source. The air compressor then generates high-pressure air, which is introduced into the pipeline. As the air flows through the pipeline, it creates a vacuum or pressure differential that draws the corn cobs into the air stream. The material is then carried through the pipeline to the receiver, where it is collected and discharged. The system's control mechanisms ensure that the air flow and material feed are synchronized, preventing blockages and maintaining consistent transport rates.
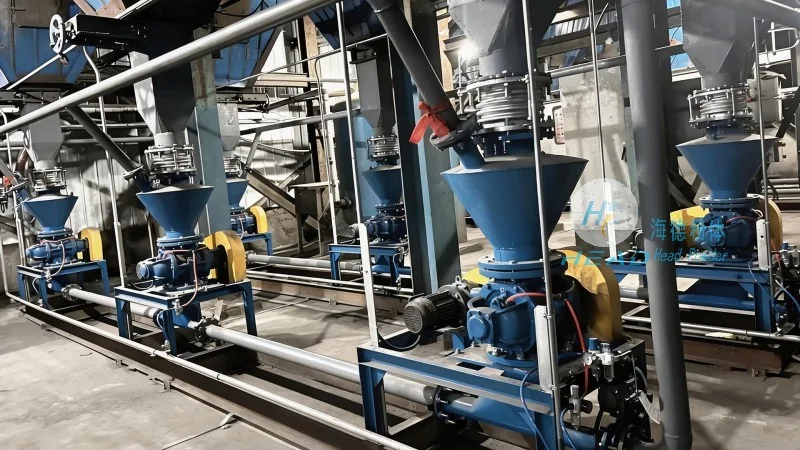
Advantages of Corn Cob Pneumatic Conveying
Implementing a corn cob pneumatic conveying system offers numerous benefits for industrial operations. The technology provides a clean and dust-free transport method, which is particularly important for food processing and agricultural applications where hygiene is critical. Additionally, the system reduces the risk of material contamination and damage, as the material is enclosed within the pipeline during transport. From an operational standpoint, pneumatic conveying systems are more energy-efficient compared to mechanical systems, as they require less power to move the material over long distances. The compact design of the system also allows for easier integration into existing production lines, minimizing space requirements and installation costs.
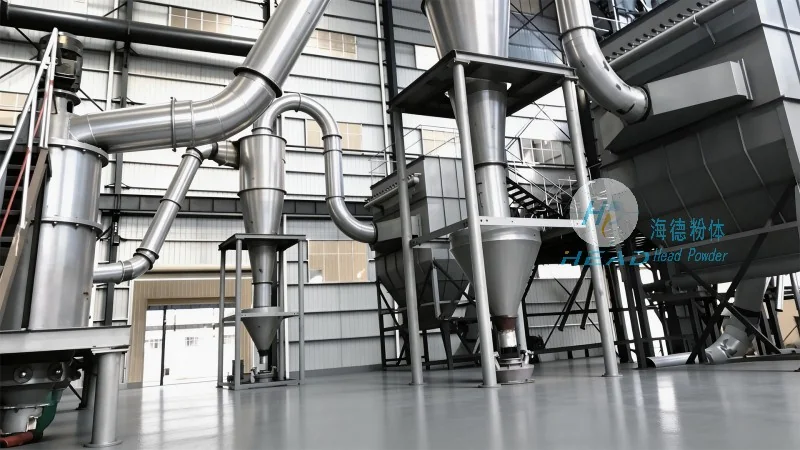
Applications and Industries
The corn cob pneumatic conveying system is widely used in various industries that process corn cobs or similar bulk materials. In the agricultural sector, it is employed in corn processing facilities to transport cobs from storage to processing equipment. The food industry utilizes the system for transporting corn cobs to drying or grinding units, where they are converted into animal feed or other products. Additionally, the system is applicable in the biofuel industry, where corn cobs are used as a raw material for producing biomass energy. The versatility of the system makes it suitable for a range of applications, from small-scale operations to large industrial plants.
Conclusion
HeadPowder's corn cob pneumatic conveying system represents a sophisticated solution for efficient material handling in agricultural and industrial settings. By understanding the structural components and working principles of the system, clients can appreciate its advantages in terms of efficiency, hygiene, and cost-effectiveness. With a strong presence in Shandong, China, HeadPowder continues to innovate and provide high-quality pneumatic conveying solutions that meet the evolving needs of its clients. The company's commitment to quality and customer satisfaction ensures that its systems deliver reliable performance and contribute to the success of industrial operations worldwide.




